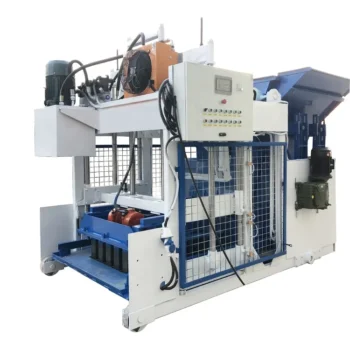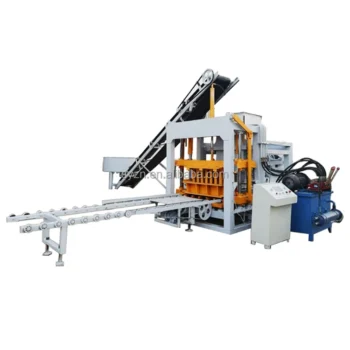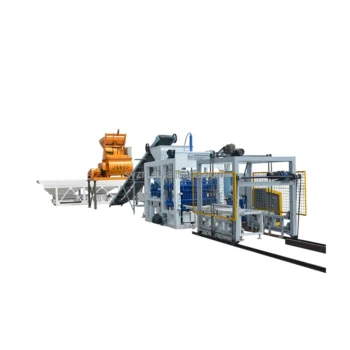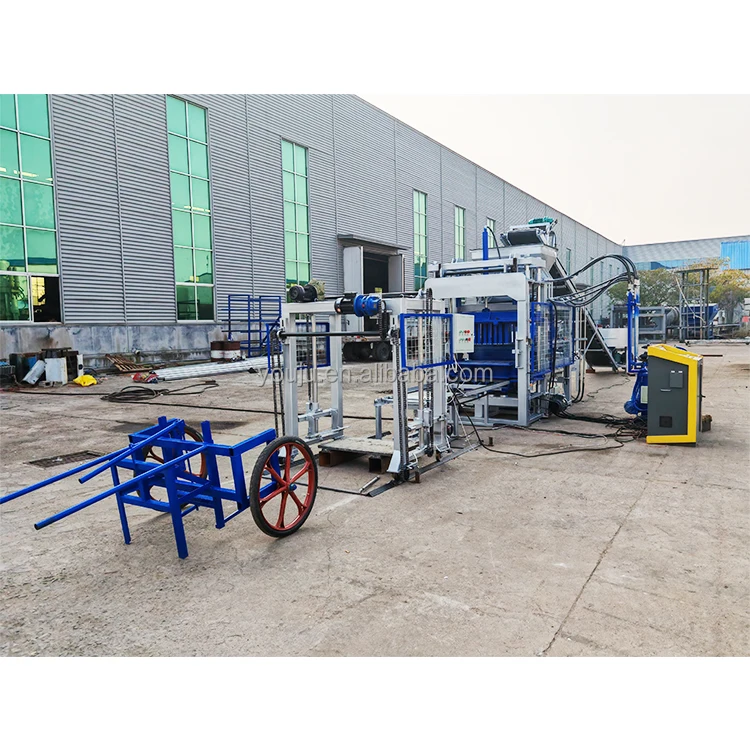
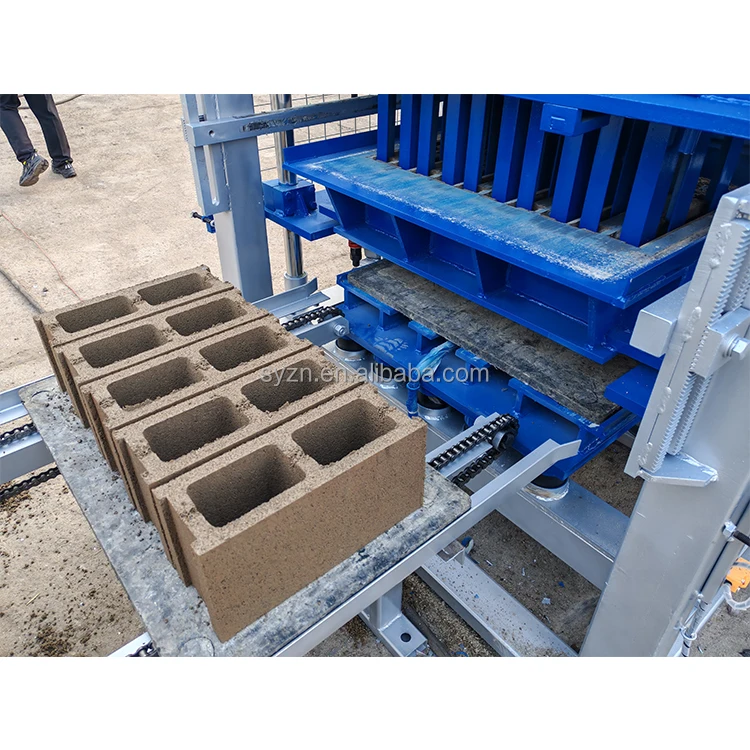
Description
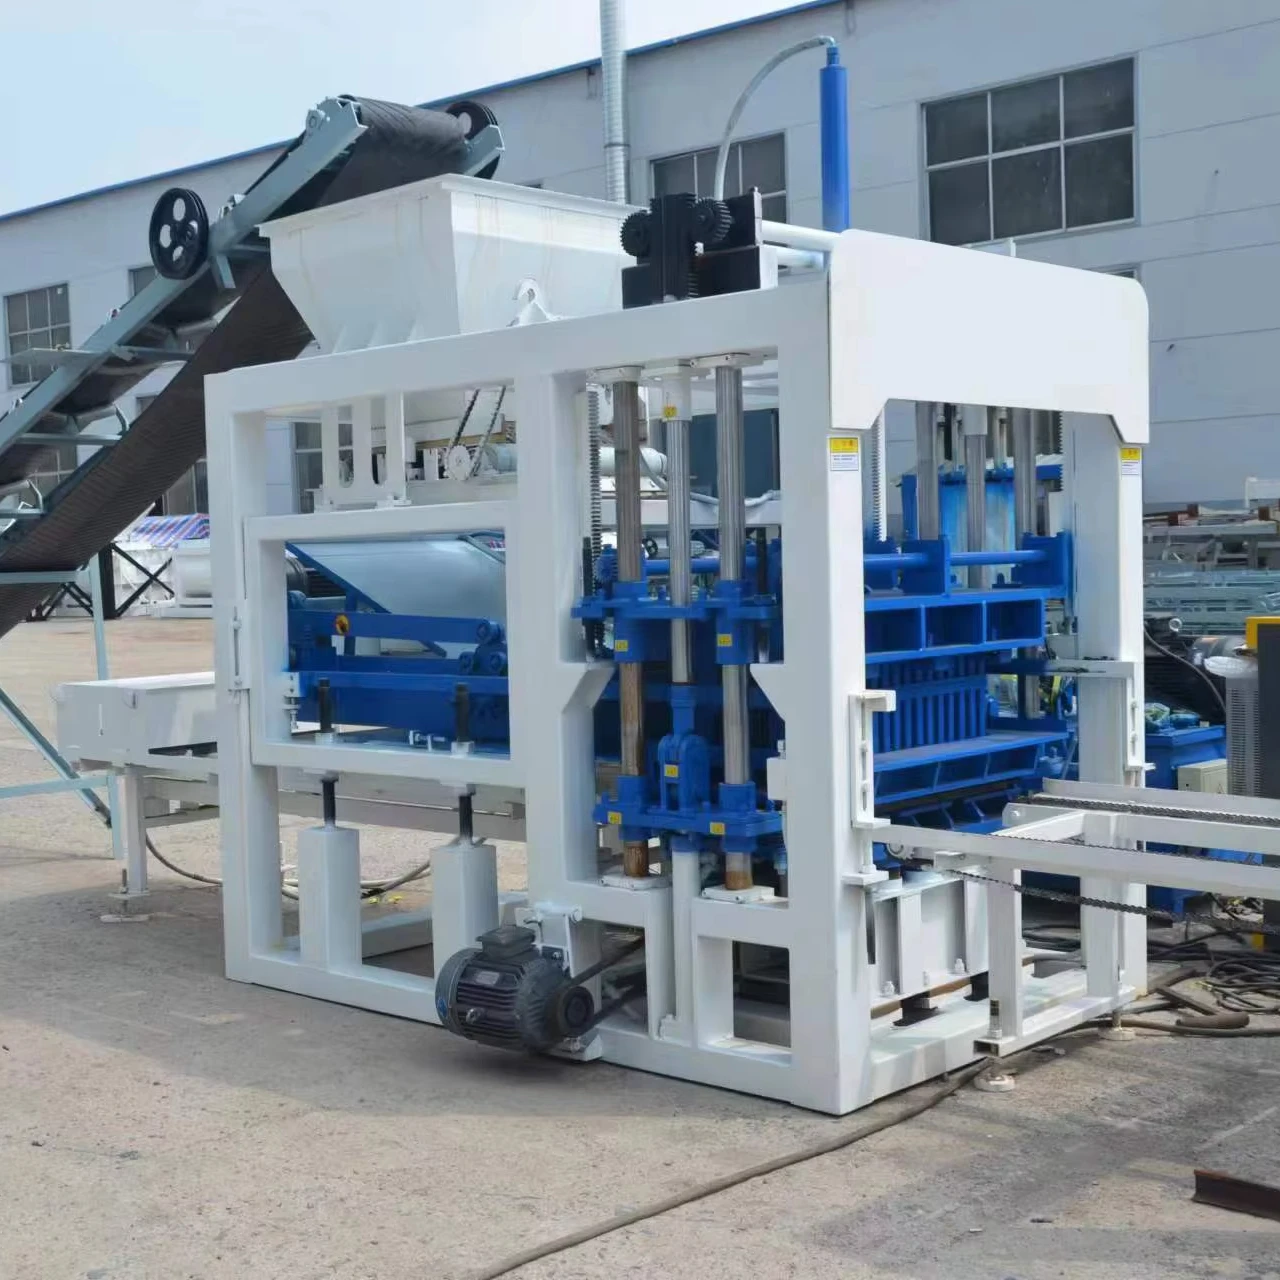
Rapid Deployment Focus — This QT6-15 automatic block making machine ships from verified stock with standard moulds and container loading schedules confirmed before purchase.
Technical Specifications
| Parameter | Value |
|---|---|
| Model | QT6-15 |
| Product Type | Automatic Concrete Block Making Machine |
| Host Machine Dimensions | 5870 × 2220 × 2850 mm |
| Host Machine Weight | 5.5 Tons |
| Molding Area | 1050 × 500 mm |
| Host Machine Power | 31.5 kW |
| Vibration Force | 55 kN |
| Vibration Frequency | 2800 – 4500 Times/Minute |
| Vibration Method | Hydraulic + Platform Vibration |
| Molding Period | 15 Seconds (basis not stated in source — confirm block format / material / thickness) |
| Pallet Size | 1100 × 550 × 25 mm |
| Control System | Siemens PLC with independently developed control program |
| Motor | Germany SIEMENS brand or CE standard brand |
| Travel Switch | France Schneider / Japan Omron |
| Voltage Options | 220V / 380V / 415V / 440V (Customized) |
| Mould Heat Treatment | Carburizing treatment, hardness 54-58 HRC, lifespan >100,000 cycles |
| Welding Standard | Carbon dioxide protection welding |
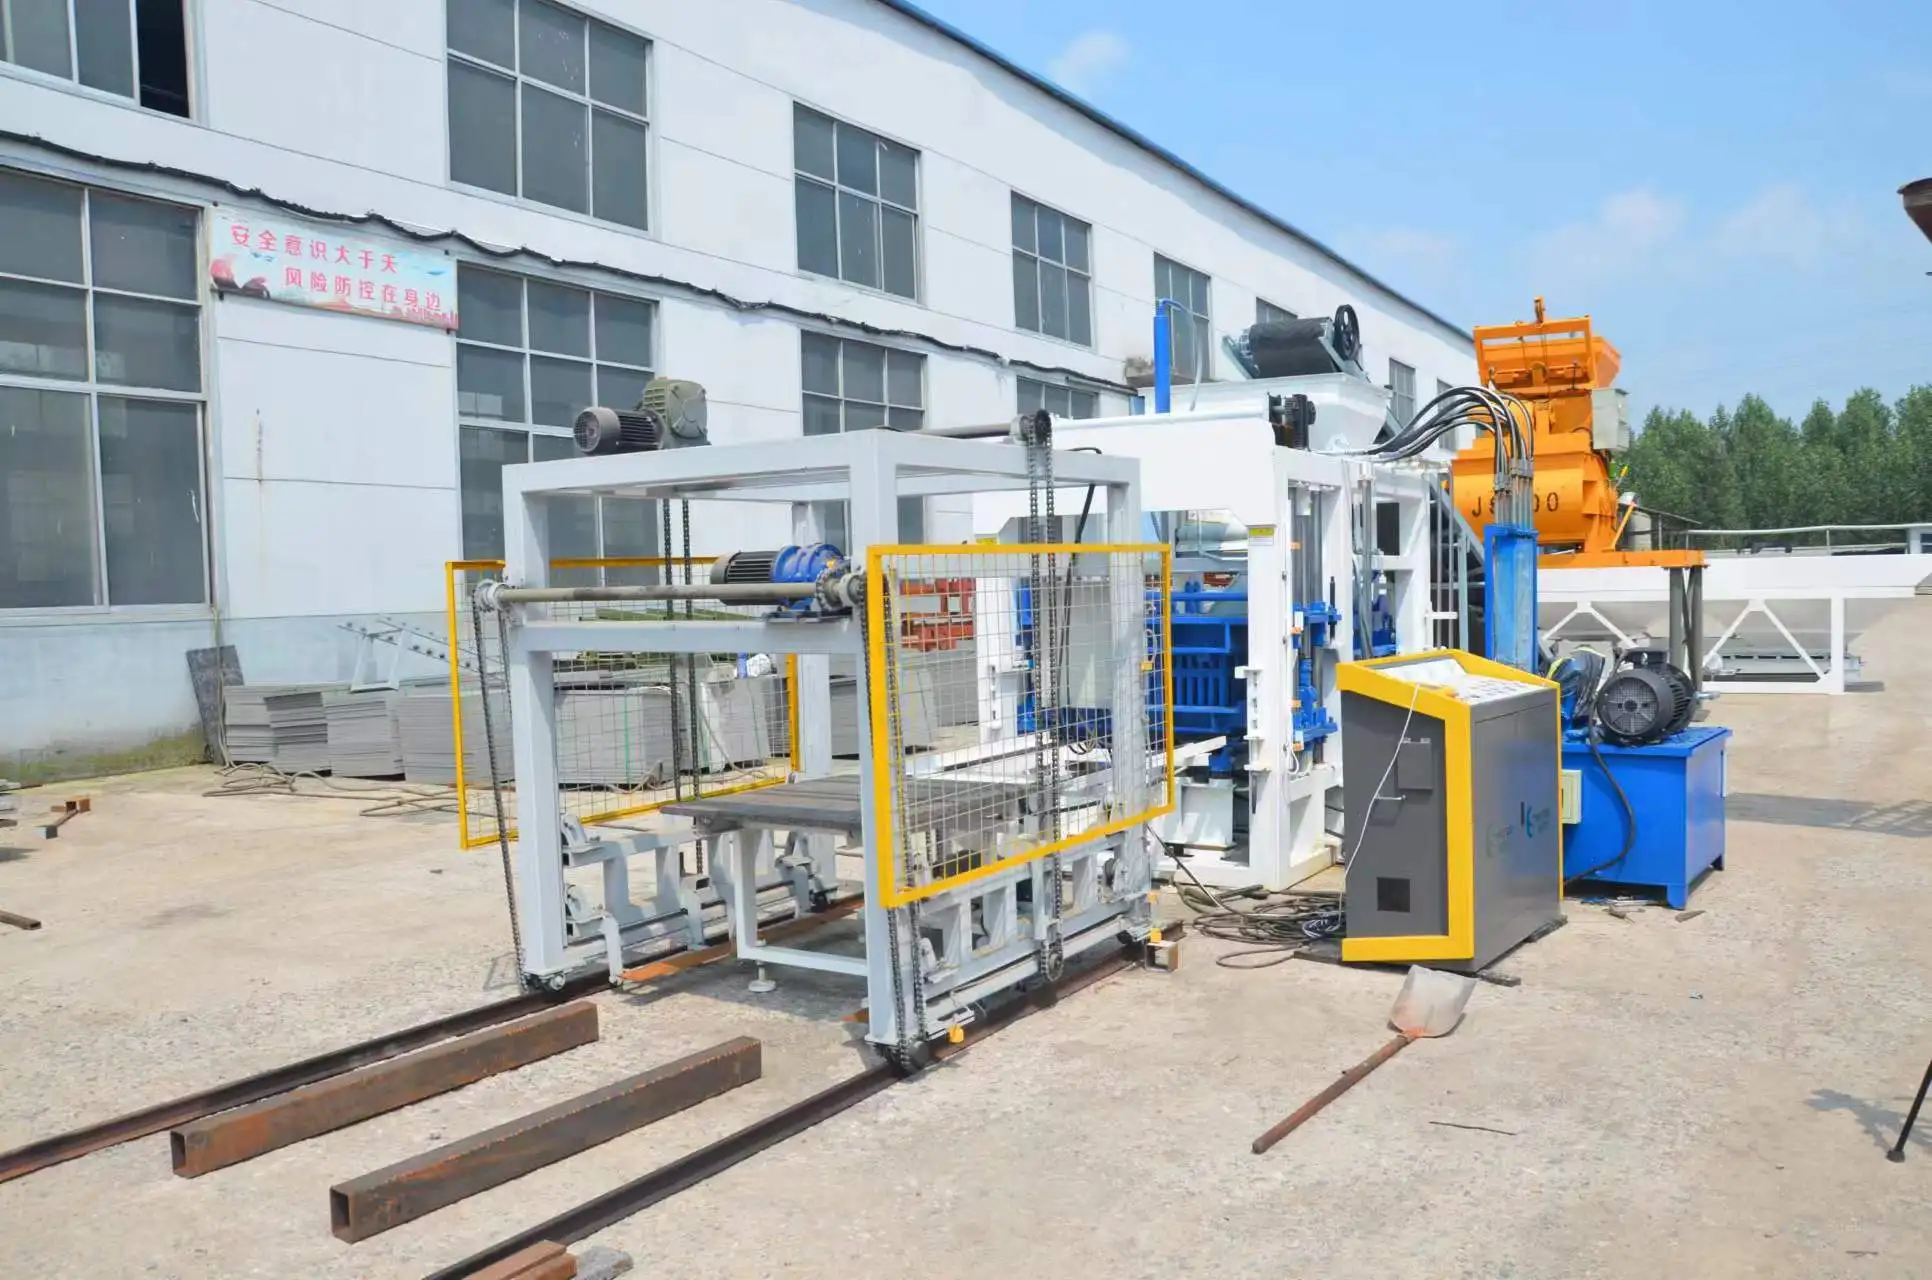
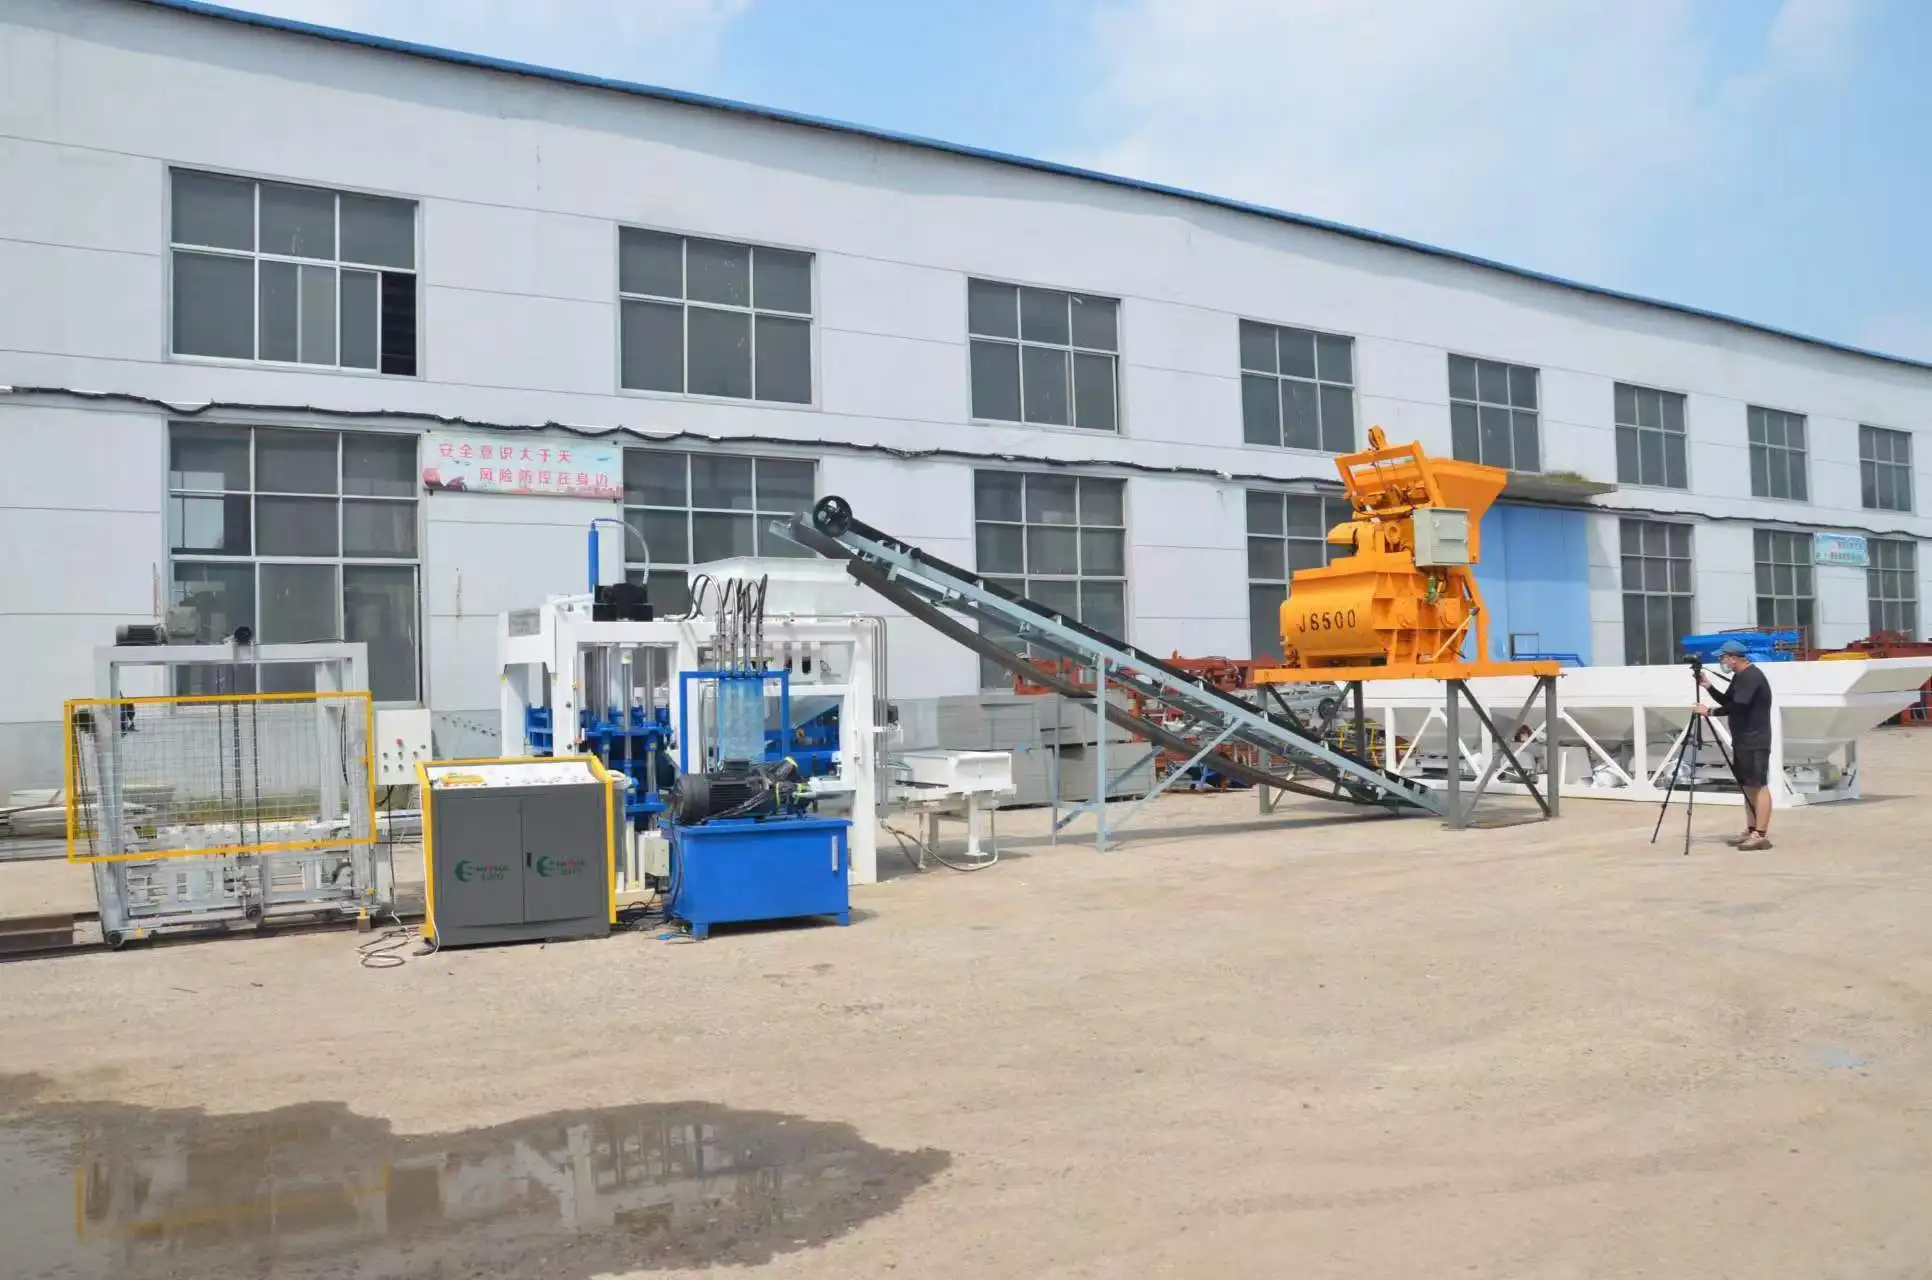
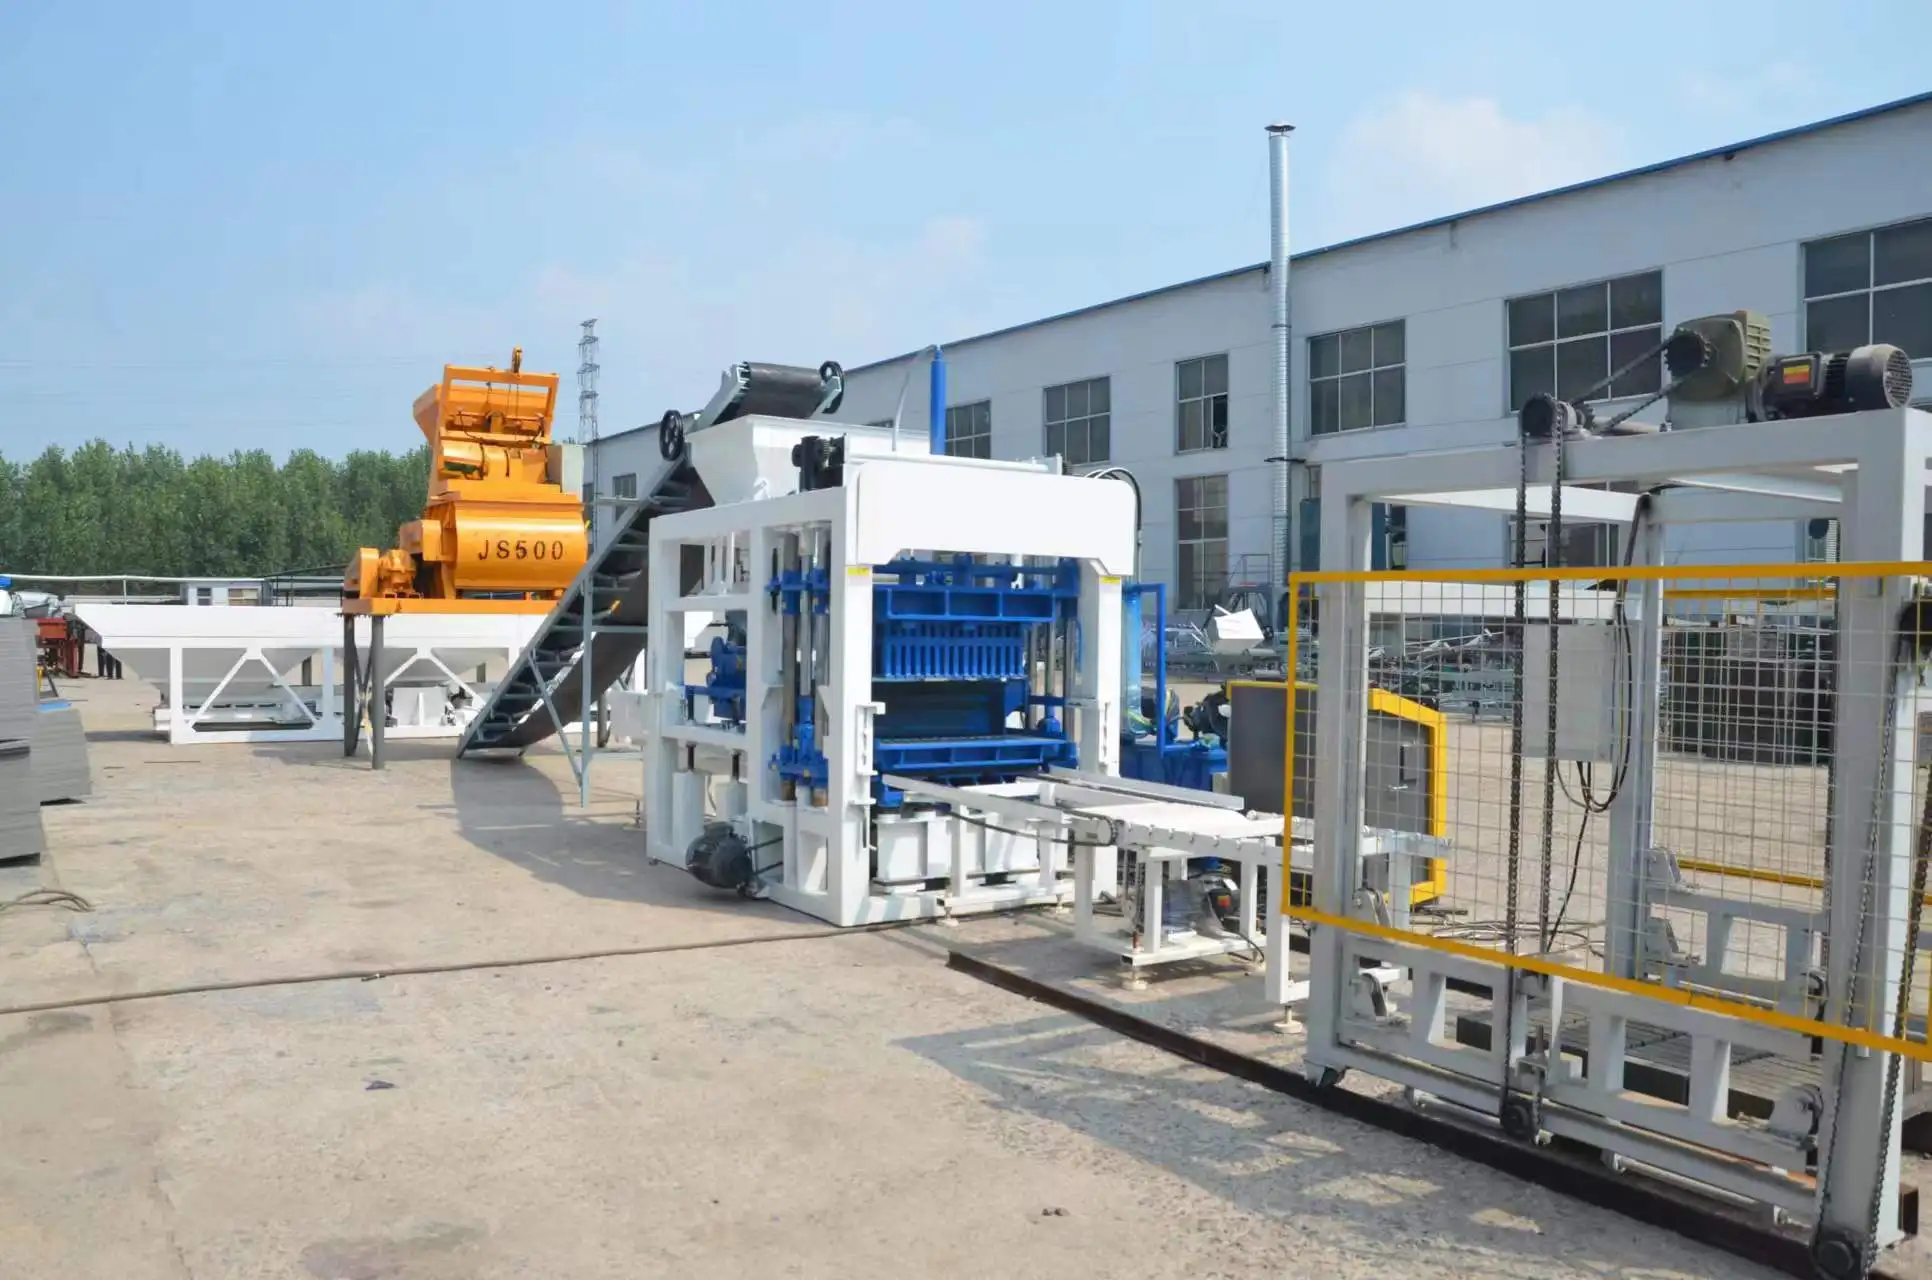
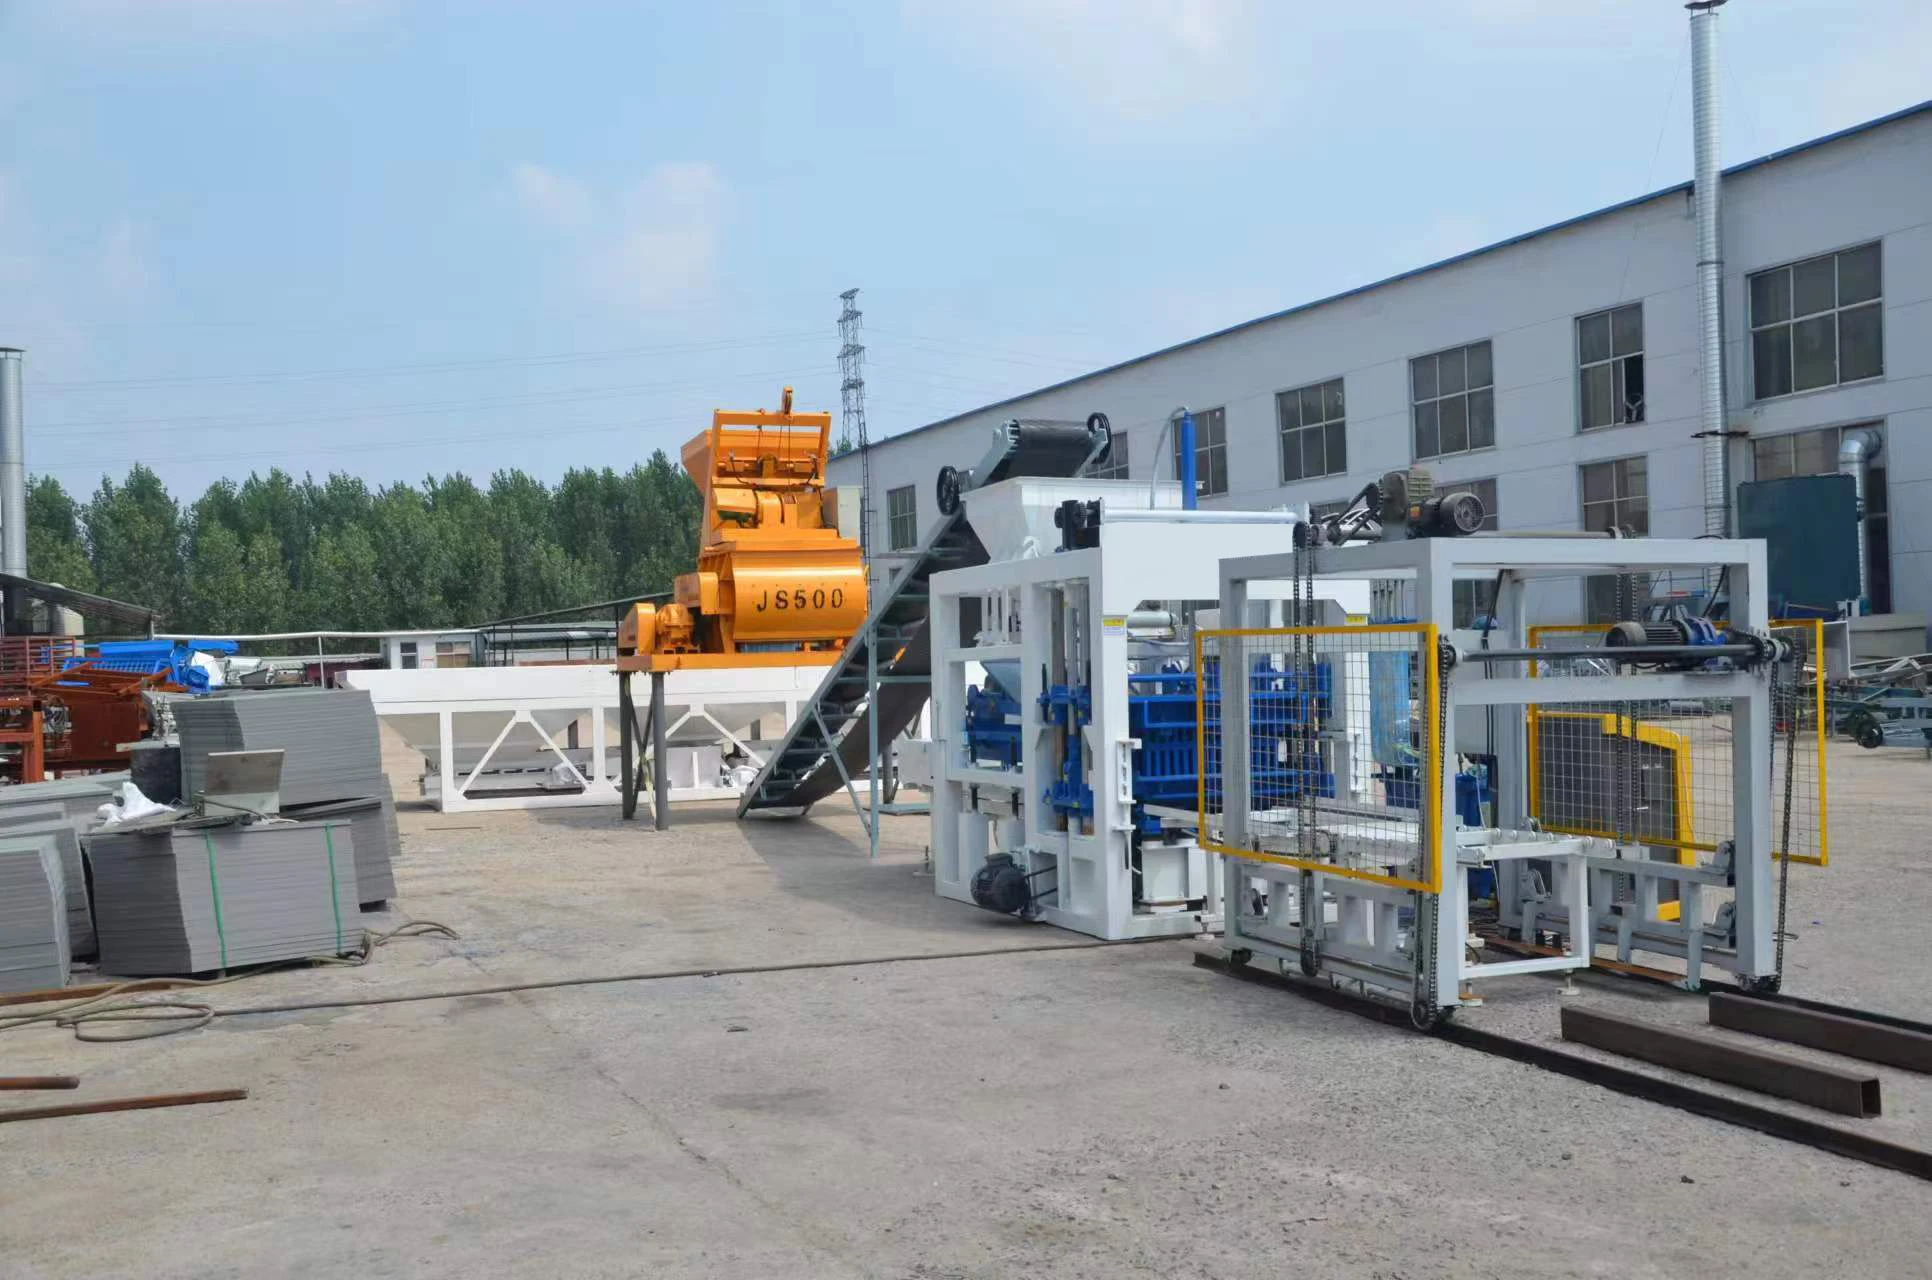
| Batching Machine | PLD1200 (1200L weigh-batching hopper, 4×2.5m³ storage) |
| Concrete Mixer | JS500 (Charging 800L / Discharging 500L / 18.5kW motor) |
| Stacker | SY-4 Mobile Pallet Stack (3kW, 600KGS capacity) |
| Assembly State | Grouped equipment line |
Application Suitability
| Application | Material or Output |
|---|---|
| Hollow Block Production | Crushed stone, sand, cement, and lightweight aggregates for structural walls |
| Paving Brick Manufacturing | Dense aggregates and pigments for heavy-duty walkways and driveways |
| Solid Brick Forming | Standard cement-sand mixes for load-bearing and partition walls |
| Interlocking Brick Production | Specialized moulds for dry-stack soil-cement or concrete interlocking blocks |
| On-Site Housing Projects | Rapid deployment for local production to meet fixed construction deadlines |
Why Arrival Estimates Dictate Machine Selection
A machine is only valuable if it is operational before your project milestones expire.
When sourcing a QT6-15 block machine in stock, the primary concern for contractors is rarely the raw cycle speed, but the actual time from dispatch to the first cured block. Delays in customs clearance, missing electrical schematics, or unconfirmed voltage configurations can stall a machine at the port for weeks. This downtime is devastating for housing developers working against fixed completion dates. Sourcing equipment that has already undergone pre-shipment dismantling verification ensures the container is loaded correctly and the documentation is ready for immediate customs processing [NEED_CITE: international shipping and customs clearance standards for heavy machinery].
Stock Availability and Dispatch Logic
The definition of "stock" varies across the industry. For a QT6-15 block machine in stock, we confirm the physical availability of both the host machine and the specific standard moulds you require. This prevents the common scenario where a machine is ready but the hydraulic system or PLC panel is awaiting final assembly.
Container Loading and Dismantling
Efficient loading is about geometry and protection. The 5870 × 2220 × 2850 mm host unit requires specific dismantling protocols to fit within standard high-cube containers while protecting the 55 kN vibration platform and Siemens PLC components from transit moisture and impact.
Electrical Pre-Verification Protocols
There is a critical difference between "220/380V" and a site-ready machine. We verify the destination grid frequency (50Hz vs 60Hz) and the specific language requirements for the Siemens PLC interface. This ensures the control system is readable and the motors do not overheat upon first commissioning.
Mould Heat Treatment and Inventory
Mould availability is the bottleneck of block production. Our stock includes carburized moulds (54-58 HRC hardness) that withstand the abrasive nature of crushed stone and cement, ensuring the lifespan exceeds 100,000 cycles before refurbishment is necessary [NEED_CITE: metallurgical standards for concrete mould carburizing].
Matching the Pallet Circuit
The 1100 × 550 × 25 mm pallet size is not arbitrary. It is designed to match standard curing rack dimensions and forklift capacities at existing plants. We confirm your current pallet inventory or curing area constraints to ensure the SY-4 stacker and the host machine integrate with your existing workflow without manual intervention.
Understanding the Vibration and Pressure Synergy
The 55 kN vibration force combined with hydraulic pressure is essential for high-density blocks. The 2800-4500 times/minute frequency range allows the operator to adjust the energy input based on the mix design. A finer sand mix requires a different frequency to achieve full compaction compared to a coarse aggregate mix, directly influencing the final block strength and curing time.
The Cost of Overlooking Dispatch Timing
Choosing a machine based solely on a lower initial price often results in significant "dead time." If a supplier cannot provide a verified packing list and dismantling photograph before the deposit is paid, you risk receiving a machine that requires on-site welding or custom electrical work to fit your workshop. This leads to prolonged commissioning periods that can derail an entire construction season [NEED_CITE: impact of equipment delay on construction project penalties].
Why Procurement Focus Matters Here
Our approach to the QT6-15 block machine in stock is built on single-focus machinery logistics. We do not bundle unrelated equipment; we provide a matched system where the PLD1200 batcher and JS500 mixer are calibrated to the host machine’s 15-second molding period (basis not stated in source — confirm block format). Every shipment includes a factory test record specific to your voltage requirements and a wear parts list that ensures you have the necessary spares for the first year of operation.
Documentation & Verification
- Machine specification sheet with confirmed pallet and mould dimensions.
- Hydraulic and electrical schematics matching the installed components.
- Voltage, frequency, and PLC display language confirmation record.
- Factory test video and dispatch lead time confirmation.
- Packing photographs and dismantling method for customs support.
- CE declaration and operation manual with safety protocols.
Installation, Commissioning & Support
- Foundation planning based on 5.5-ton host weight and vibration isolation.
- Electrical verification for 31.5 kW host power and 18.5 kW mixer load.
- Assembly guidance for the 1050 × 500 mm molding area and vibration table.
- Calibration of Siemens PLC for your specific aggregate and moisture content.
- Operator training on mould change and SY-4 stacker synchronization.
- Spare parts list for hydraulic valves and travel switches (Schneider/Omron).
Inquiry Direction for Immediate Dispatch
To move quickly on a QT6-15 block machine in stock, provide your specific block format (hollow, solid, or paving), the required daily output volume, and your local voltage/frequency standards. This allows us to confirm the exact moulds and electrical configuration available for the next container loading.
Frequently Asked Questions
Q: What is the actual dispatch lead time for the QT6-15 in stock?
A: Dispatch lead times are provided in writing upon order confirmation. Because the machine is in stock, the primary variable is the container booking and the pre-shipment verification of your specific voltage and PLC language requirements. We provide a loading schedule once the electrical confirmation is finalized.
Q: How is the machine dismantled for shipment to ensure it arrives safely?
A: The host machine and supporting equipment are dismantled according to a specific packing protocol designed for standard container loading. We provide packing photographs and a dismantling method document to ensure that upon arrival, the 5870 × 2220 × 2850 mm unit can be reassembled without cutting or welding.
Q: Can I confirm the voltage and control language before the machine ships?
A: Yes, this is a mandatory step. We verify the destination voltage (220/380/415/440V) and the required language for the Siemens PLC display to prevent commissioning delays. This ensures the electrical cabinet is wired correctly before it leaves the factory.
Q: Are standard moulds and wear parts included in the stock shipment?
A: We confirm the stock status of standard moulds (hollow, solid, or paving) and hydraulic wear parts before you commit. This ensures that the machine can begin production immediately upon arrival without waiting for international air freight for missing components.