



Description
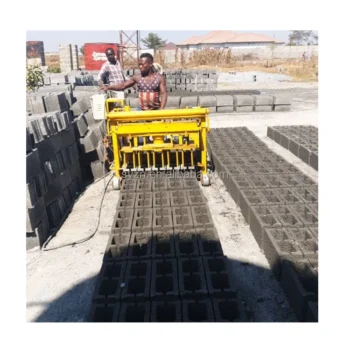
Ready-Stock Availability — QMJ4-45 units staged for container loading, letting project-bound contractors bypass typical multi-week production backlogs.
Technical Specifications
| Parameter | Value |
|---|---|
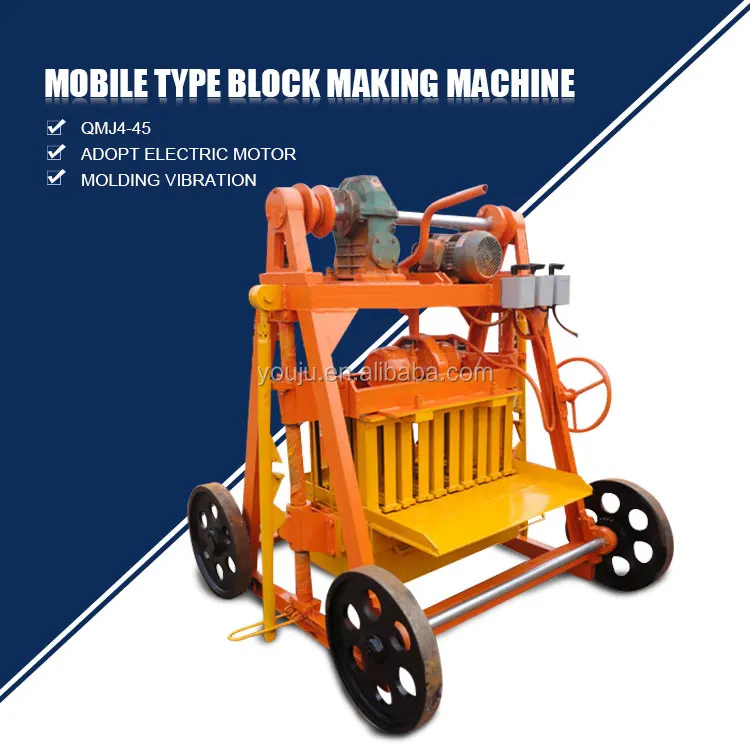
| Model | QMJ4-45 |
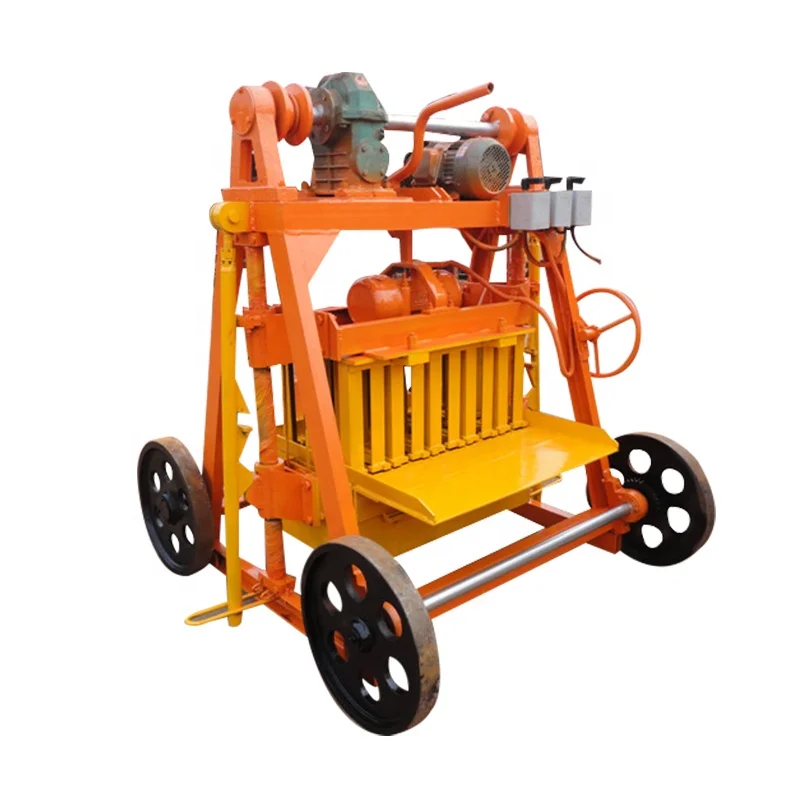
| Product Type | Mobile Egg-Laying Block Making Machine |
| Molding Capacity | 4 pcs/mold |
| Vibration Frequency | 2400 r/m |
| Vibration Method | Mold vibration |
| Molding Cycle | 45 s |
| Demold Method | Manual |
| Turning Method | Manual |
| Total Power | 6 kW |
| Power Source | Diesel or petrol engine option |
| Hollow Block Productivity (400×200×200 mm) | 3000 pcs per 8-hour shift (4 pcs/mould, 40-45 s cycle) |
| Hollow Block Productivity (400×150×200 mm) | 3500 pcs per 8-hour shift (5 pcs/mould, 40-45 s cycle) |
| Hollow Block Productivity (400×120×200 mm) | 4500 pcs per 8-hour shift (6 pcs/mould, 40-45 s cycle) |
| Automation Level | Manual (egg-laying / mobile) |
| Pallet Requirement | None — on-ground egg-laying operation |
| Certification | CE (declaration available; confirm per shipment) |
Application Suitability
| Application | Material or Output |
|---|---|
| On-site hollow block production for remote building projects | Crushed stone, sand, and cement mixes laid directly on prepared ground |
| Garden path and landscaping block supply | Solid or hollow format blocks from local aggregate without pallet infrastructure |
| Housing development contractors producing blocks near the build location | Standard hollow blocks (400×200×200 mm and smaller wall thicknesses) |
| Entrepreneur block supply in new or shifting markets | Relocatable egg-laying output without fixed curing racks or plant footprint |
What "3000 Blocks per Shift" Actually Means on Your Site
The daily output figure is only meaningful when tied to a specific block format, wall thickness, and cycle time — and most quotations leave that connection unstated.
A contractor ordering a mobile block machine in stock for a housing project often receives a single productivity number without knowing which mould and block size it assumes. Switching from a 200 mm wall block to a 120 mm wall block changes the mould cavity count and shifts the realistic shift output considerably. The QMJ4-45 produces 3000 pieces per 8-hour shift on 400×200×200 mm hollow blocks, 3500 pieces on 400×150×200 mm, and 4500 pieces on 400×120×200 mm — each tied to a 40-45 second cycle with the corresponding cavity count. Without that breakdown, buyers routinely overestimate daily tonnage and under-plan their curing space. [NEED_CITE: block format and cycle time impact on daily output calculations]
Stocked Units Versus Built-to-Order Delays
Project timelines rarely wait for factory schedules. The QMJ4-45 mobile block machine in stock is staged for dispatch without passing through a production backlog queue, meaning container booking can begin once mould and power specifications are confirmed. This matters most for contractors who committed to a build start date before the equipment purchase was finalized — a common sequence in development projects across West Africa and South Asia where site mobilization outpaces procurement cycles.
Engine-Powered Independence from Grid Constraints
Diesel and petrol engine options remove the dependency on site electrical infrastructure that stalls commissioning on remote projects. A garden-path contractor working outside Lagos or a housing team in rural Bangladesh often faces weeks of delay securing a stable three-phase supply. The 6 kW total power requirement of the QMJ4-45 falls within the range a portable engine can sustain, letting block production begin the day the machine is uncrated and leveled on prepared ground. [NEED_CITE: power source flexibility for off-grid construction equipment]
Reading the Specifications That Matter on Site
The 2400 r/m vibration frequency drives compaction through mold vibration rather than table vibration, concentrating force directly into the cavity where the mix sits. This method suits the egg-laying format because the machine moves forward after each cycle, leaving the block on the ground rather than on a pallet. The 45-second molding cycle encompasses feed, vibration, and manual demold — a pace that a two-person crew can sustain across an 8-hour shift without fatigue-driven slowdown. Mould cavity count scales with wall thickness reduction: four cavities at 200 mm, five at 150 mm, six at 120 mm. Buyers planning production around a specific block format should request the mould drawing to verify cavity layout before confirming the order, since cavity count directly determines which productivity tier applies to their project.
The Cost of Skipping the Dispatch Checklist
A mobile block machine arriving on site with the wrong engine specification or an unconfirmed mould format turns a fast-delivery advantage into a multi-week standstill. Contractors who skip voltage or engine verification before dispatch — or who assume a standard mould is included when it is on a separate lead time — absorb idle crew costs and missed construction milestones that far outweigh the machine price itself. [NEED_CITE: commissioning delays caused by unconfirmed equipment specifications] Egg-laying machines are particularly exposed because they serve remote sites where sourcing a replacement part or waiting on a mould shipment carries transport delays that fixed-plant buyers never face.
Why Buyers Source This Machine Here
Block machinery as a single focus means the QMJ4-45 is specified alongside its mould, pallet requirements (or elimination of them), and handling workflow as one system — not assembled from unrelated suppliers. Configuration is set against the buyer’s local aggregate and target block format, so the vibration frequency and cycle time match the actual mix available on site rather than a catalogue default. Standard moulds for common hollow block formats are stocked alongside the machine, preventing mould lead time from holding up press dispatch. The diesel or petrol engine option is confirmed before shipment, so the machine arrives ready to run on the fuel supply the site already has. Wear parts and a spare kit ship taped to the pallet, because remote sites cannot wait on international freight for a bearing that weighs under a kilo.
Documentation & Verification
- Factory test record run on your specified block format and mould cavity count before dispatch
- Mould drawing showing cavity layout, dimensions, and wear-part interface for your block size
- Engine specification sheet confirming fuel type, power output, and mounting configuration
- Voltage and control language confirmation document for engine instrumentation where applicable
- Packing photographs showing machine, mould, and wear-kit placement inside the container
Installation, Commissioning & Support
- Leveled ground preparation with compacted surface required before the 6 kW machine begins egg-laying cycles
- Diesel or petrol engine fuel supply and filter check completed during first-day commissioning
- Mould cavity inspection and vibration frequency verification at 2400 r/m before production run starts
- Manual demold and turning technique covered during operator training for consistent block release
- Wear kit included on the pallet covers vibration motor bearings and high-contact mould surfaces
- Mould change procedure walkthrough so format switches do not consume a full shift
Before You Request a Quote
Confirm the block format your project or market requires — wall thickness, length, and height — so the correct mould cavity count and productivity tier are quoted. Specify whether diesel or petrol engine power suits your site conditions and fuel supply chain. State your target daily output and the number of working hours per shift so the capacity calculation matches your actual schedule rather than a generic figure.
Frequently Asked Questions
Q: What block format is the quoted daily output based on, and can I get figures for my specific block size?
A: The published output figures are tied to specific hollow block dimensions: 3000 pieces per 8-hour shift for 400×200×200 mm at 4 cavities, 3500 for 400×150×200 mm at 5 cavities, and 4500 for 400×120×200 mm at 6 cavities, all on a 40-45 second cycle. If your target block falls outside these formats, request a revised calculation based on your mould cavity count and confirmed cycle time.
Q: Is the QMJ4-45 currently in stock, and what is the estimated dispatch and arrival timeline?
A: Stocked units are staged for dispatch without entering a production backlog queue. Once your mould format and engine type are confirmed, container booking proceeds immediately. Arrival timing depends on destination port and shipping lane — request a dispatch and transit estimate at the quotation stage so your project schedule accounts for the full lead time.
Q: Does the machine come with standard moulds in stock, or is there a separate lead time for moulds?
A: Standard hollow block moulds for common formats are stocked alongside the machine to prevent separate lead times from delaying the press itself. Custom mould designs or less common block formats may carry their own production window. Confirm your required mould at the inquiry stage so both machine and mould ship in the same container.
Q: Can the machine run on a diesel engine if my site has no reliable grid power?
A: Yes. The QMJ4-45 is available with a diesel or petrol engine power source, removing the need for grid electricity on remote or off-grid sites. The 6 kW total power requirement is within the range a portable engine sustains. Specify your preferred fuel type before dispatch so the correct engine is mounted and tested at the factory.