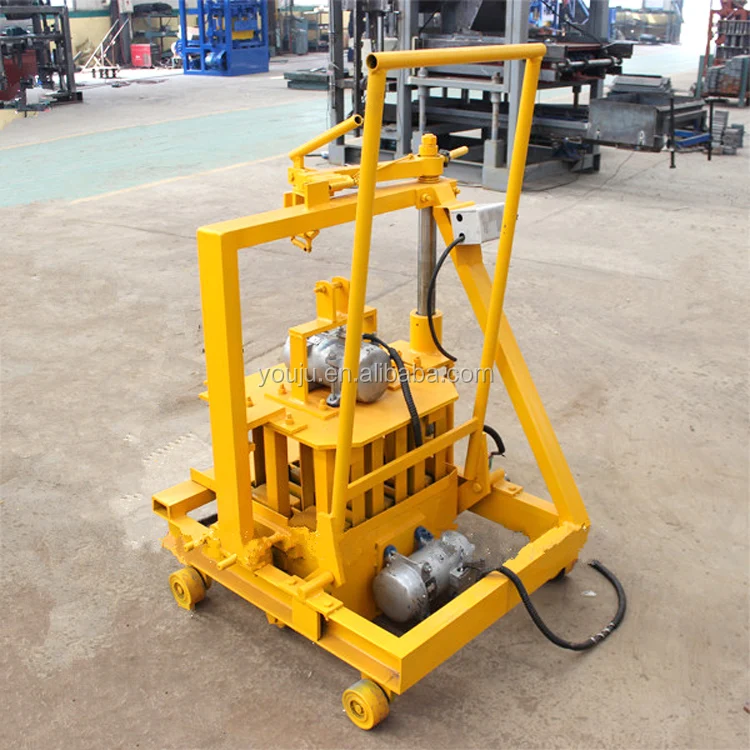


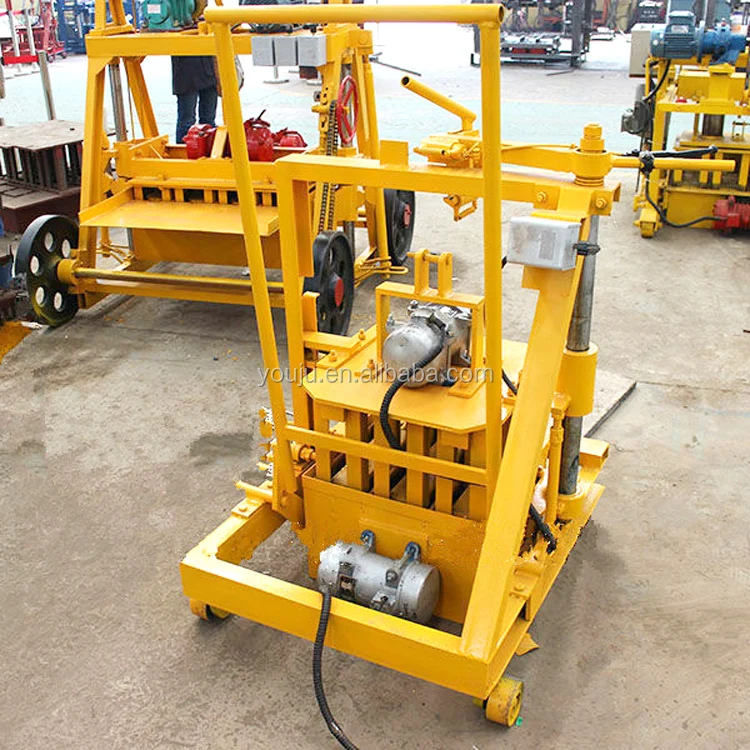

Description
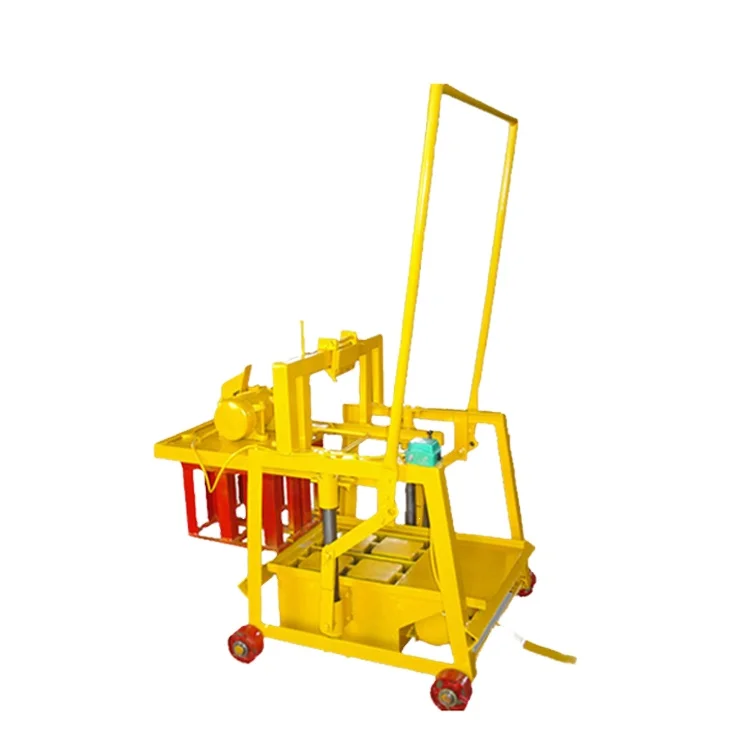
Pallet-Free Operation, Stocked for Dispatch — the QMJ2-45 mobile block making machine lays hollow blocks directly on the ground, eliminating pallet procurement and handling from your supply chain, and ships from stock so your project does not wait on a production queue.
Technical Specifications
| Parameter | Value |
|---|---|
| Model | QMJ2-45 |
| Product Type | Mobile Block Making Machine |
| Operation Mode | Manual mobile egg-laying |
| Pallet Requirement | No pallets required |
| Power Source | Engine (diesel or electric, confirm at inquiry) |
| Labor Requirement | 1 to 3 workers |
| Mould Change | Manual, supports multiple hollow brick formats |
| Cycle Time | 25-30 seconds per mould |
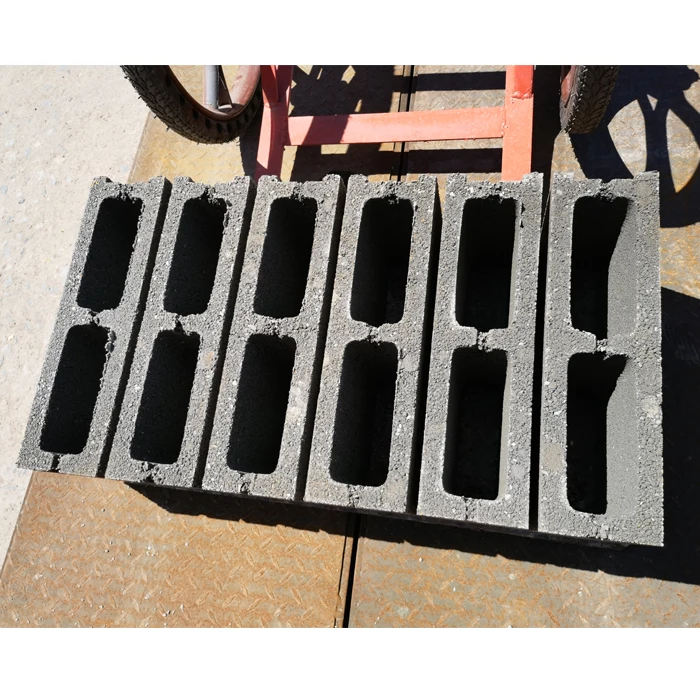
| Production Capacity — 400×200×200mm Hollow Brick | 160 pcs/h, 1280 pcs/8hr (basis: 2 pcs/mould, 25-30s cycle) |
| Production Capacity — 400×150×200mm Hollow Brick | 240 pcs/h, 4800 pcs/8hr (basis: 3 pcs/mould, 25-30s cycle) |
| Production Capacity — 400×100×200mm Hollow Brick | 320 pcs/h, 2560 pcs/8hr (basis: 4 pcs/mould, 25-30s cycle) |
| Mould Formats | Hollow brick (multiple sizes; solid and paving formats to be confirmed) |
| Mobility | Freely movable on-site, no fixed plant required |
| Space Requirement | Suitable for small space operation |
| Control System | Manual (no PLC) |
| Automation Level | Manual |
| Standards | ISO 9001:2000, CE |
| Overall Dimensions | (basis not stated in source — confirm at inquiry) |
| Net Weight | (basis not stated in source — confirm at inquiry) |
| Rated Power | (basis not stated in source — confirm at inquiry) |
| Voltage & Frequency | (basis not stated in source — confirm at inquiry) |
| Hydraulic Pressure | (basis not stated in source — confirm at inquiry) |
| Vibration Force | (basis not stated in source — confirm at inquiry) |
Application Suitability
| Application | Material or Output |
|---|---|
| On-site hollow block production for building contractors | Crushed stone, sand, cement, and water mixed on the job site |
| Small-scale block production in limited space | Local aggregate blends including volcanic ash or river sand where available |
| Remote project sites without reliable grid power | Engine-driven operation independent of electrical infrastructure |
| First-time block plant operator producing hollow bricks locally | Standard cement-aggregate mixes with locally sourced raw materials |
| Project-based production relocating between job sites | Any standard hollow block mix design compatible with manual feeding |
Why the Block Format Question Must Come Before Dispatch
The QMJ2-45 mobile block making machine in stock produces different hourly outputs depending on which hollow brick size you run, and confirming your target format before shipment prevents a machine that arrives configured for the wrong mould.
I learned this the hard way early in my career. A contractor in Southeast Asia ordered a small egg-laying unit for 400×150×200mm blocks, but his market actually demanded 400×200×200mm. The machine shipped with the wrong mould set, and by the time replacement moulds arrived, his crew had been idle for weeks [NEED_CITE: typical mould replacement lead times for mobile block machines]. That experience reshaped how I approach every inquiry — format first, everything else follows. When a mobile block making machine in stock ships without the buyer confirming the exact block dimensions their local market purchases, the entire investment stalls on a mismatched mould.
Dispatch Speed Meets Format Verification
The primary advantage of sourcing a mobile block making machine in stock is the shortened timeline from order to production. For project contractors working against a deadline, weeks of waiting for a built-to-order unit can mean penalties or lost contracts. The QMJ2-45 is held as a stocked model, so once your block format and engine preference are confirmed, the dispatch sequence begins immediately. The egg-laying design means there is no pallet system to configure, no curing rack to build, and no fixed foundation to pour — the machine lays blocks directly on the ground and moves forward as production progresses.
What Stock Availability Actually Means for Your Timeline
Stock does not mean every possible configuration sits on the warehouse floor. The base machine is ready, but the mould set must match your specific hollow brick dimensions. Before dispatch, the correct mould is fitted and a factory test is run to confirm cycle time and block density on that format. This verification step takes additional time but prevents the costly mismatch I described earlier [NEED_CITE: common causes of block machine commissioning delays]. For buyers working to a project deadline, this pre-shipment check is far shorter than the delay caused by receiving the wrong mould and waiting for a replacement to be manufactured and shipped separately.
How Cycle Time and Block Format Determine Your Realistic Daily Output
The QMJ2-45 runs a 25-30 second cycle per mould. For a 400×200×200mm hollow block, the mould holds 2 pieces, yielding 160 pieces per hour or roughly 1,280 in an 8-hour shift. For the smaller 400×150×200mm format, the mould holds 3 pieces, pushing output to 240 per hour and 4,800 per shift. The narrowest format, 400×100×200mm, fits 4 pieces per mould at 320 per hour and 2,560 per shift. These figures assume continuous operation with a prepared mix and a cleared curing area ahead of the machine. On a real job site with material delivery delays, worker breaks, and mould changes, actual throughput will differ. The key point is that output is format-dependent, and any supplier quoting a single number without naming the block size is leaving out essential information [NEED_CITE: industry standard practice for quoting block machine capacity per format].
Reading the Specifications That Matter for On-Site Production
The QMJ2-45 operates without pallets, which removes an entire material handling stream from your site. Pallets cost money to buy, require storage space, and need workers to move them — none of that applies here. The engine-powered drive means the machine does not depend on grid electricity, a critical factor on remote construction sites where power supply is unreliable or unavailable. With 1 to 3 workers operating the unit, labour costs stay proportional to the small output scale this machine targets. The manual mould change allows switching between hollow brick formats, but the changeover takes operator time and care — plan format changes for shift breaks rather than mid-production to avoid losing cycle time.
The Hidden Cost of Skipping Raw Material Verification
I once watched a mobile egg-laying unit struggle for five straight days because the local contractor used a sea sand and volcanic ash blend, while the factory test had used standard silica sand. The vibration time and pressure parameters that worked perfectly in Shandong produced crumbling blocks on site. After we recalibrated, the machine ran fine — but five days of lost production and frustrated workers could have been avoided by sending a raw material sample before the machine shipped [NEED_CITE: impact of local aggregate variation on block compression strength]. Always request a factory test on your actual mix design, not the supplier’s default material.
Why Procurement Through This Channel Works for Stocked Machines
Block machinery is the single focus here, which means the QMJ2-45 is not bundled from separate suppliers but specified as a matched unit with its mould set and engine. The configuration is set against your actual block format rather than a catalogue default, so the mould that ships with the machine produces the hollow brick your market buys. Dispatch lead time is quoted upfront at inquiry, not buried in fine print. Factory test records and packing photographs are provided before shipment so you can verify condition and completeness. Documentation for customs clearance is prepared in advance, reducing port delays. The manual operation design means there are fewer electronic components to fail in dusty, humid job site conditions.
Documentation & Verification
- Factory test record run on your specified hollow brick format before dispatch
- Machine specification sheet listing overall dimensions and weight for freight planning
- Mould drawing confirming block dimensions and cavity count per format
- CE declaration for import compliance in regulated markets
- Operation and maintenance manual covering daily checks and mould change procedure
- Packing photographs showing machine condition and container loading arrangement
Installation, Commissioning & Support
- No foundation required — the QMJ2-45 operates on level ground at your job site
- Confirm engine type and fuel specification against locally available diesel or petrol before shipment
- Machine arrives assembled with mould fitted; verify all fasteners after transport vibration
- First production run should use your local aggregate blend to confirm block strength and adjust cycle parameters
- Operator training covers manual feeding rhythm, mould change procedure, and basic engine maintenance
- Request a wear parts list for mould edges and vibration components at time of order
What to Include in Your Inquiry
To move quickly from inquiry to dispatch on the QMJ2-45, specify the exact hollow brick dimensions your market demands, including length, width, and height. Confirm the engine type available in your area — diesel or electric — along with local voltage and frequency if electric is preferred. State your target daily output so the correct mould cavity count can be matched to your production plan. If your local aggregate differs from standard silica sand, send a raw material sample so the factory test reflects your actual conditions.
Frequently Asked Questions
Q: Is the QMJ2-45 mobile block making machine in stock now, and what is the dispatch lead time?
A: The QMJ2-45 is stocked as a standard model. Once your block format and engine preference are confirmed, the factory test and packing are completed before dispatch. Exact lead time depends on the mould configuration required and current stock position at the time of your inquiry. We quote the dispatch date upfront so you can plan around your project deadline.
Q: How does the machine ship, and what are the loading requirements?
A: The QMJ2-45 is compact enough to ship via LCL or full container depending on quantity and accompanying mould orders. The machine is loaded in its operational configuration with the selected mould fitted. We provide overall dimensions and loading photographs at the packing stage so your freight forwarder can arrange the correct container type and secure loading plan.
Q: Can I order additional moulds for different hollow block formats, and are those stocked too?
A: Additional moulds for different hollow brick dimensions can be ordered alongside the machine. Standard hollow block format moulds are typically available from stock. Custom mould sizes may require a manufacturing lead time. Specify all required formats at inquiry so the complete mould set ships together and your machine arrives ready to produce every block your market needs.
Q: What engine type does the QMJ2-45 use, and is it serviceable locally?
A: The machine can be configured with a diesel or electric engine depending on your site conditions. Confirm your local fuel availability and electrical supply at inquiry so the correct option is fitted. The engine type used is a common industrial specification, and spare parts are generally available through regional engine distributors. We confirm the exact engine model before production so you can verify local serviceability.
Q: What documentation ships with the machine for customs and operation?
A: Each QMJ2-45 ships with an operation and maintenance manual, CE declaration where applicable, factory test record, and packing list. Customs documentation support is provided to smooth the import process at your destination port. The manual covers daily maintenance, mould change procedure, and engine care so your operators can maintain the machine independently from day one.