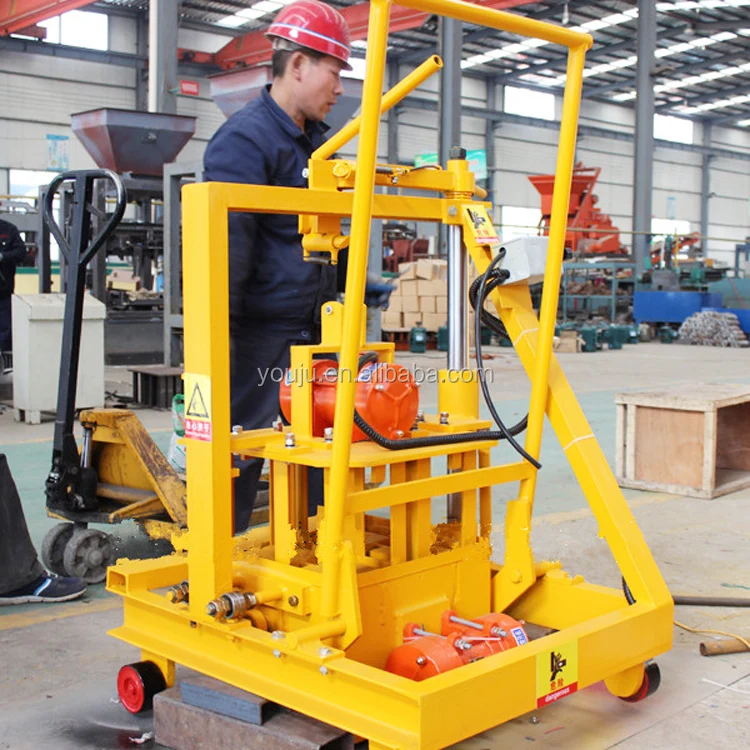
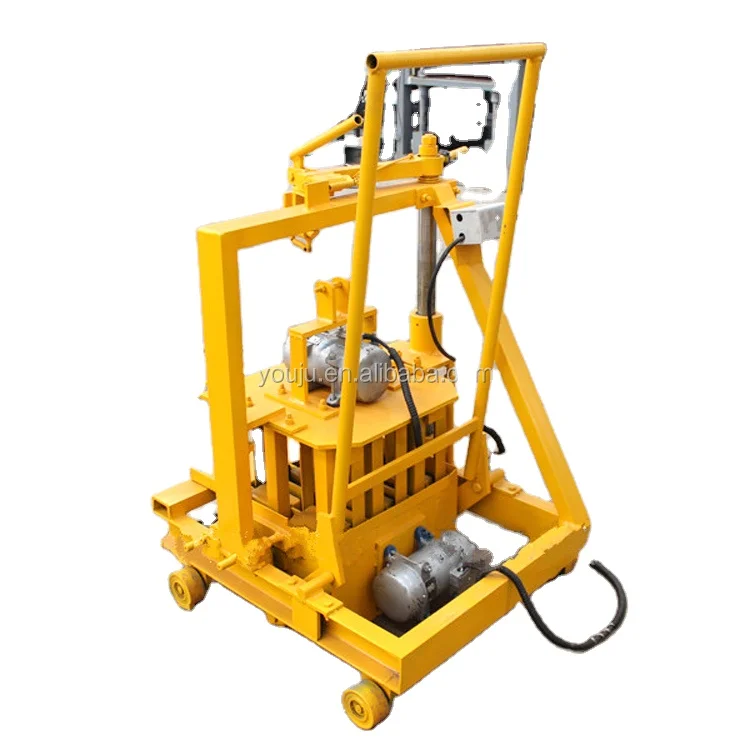
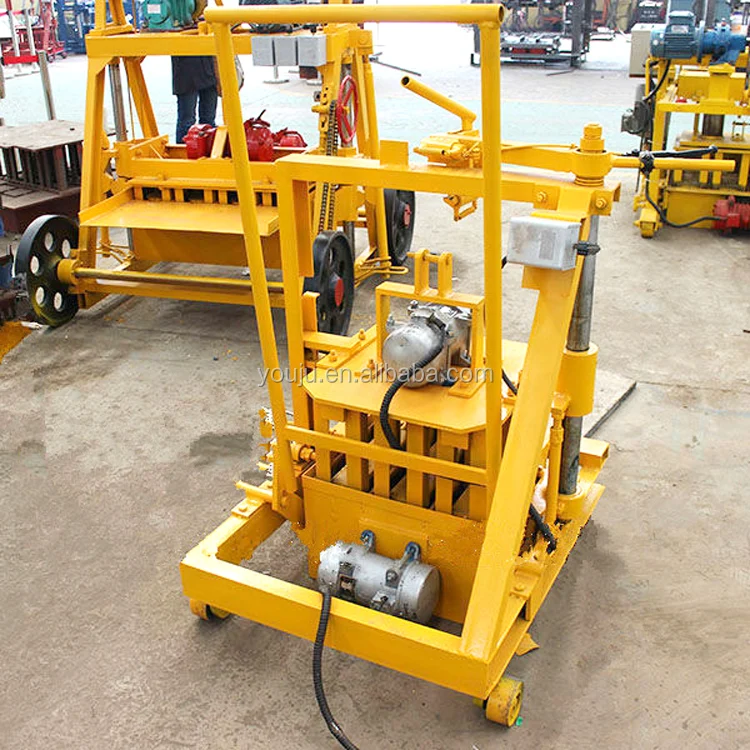
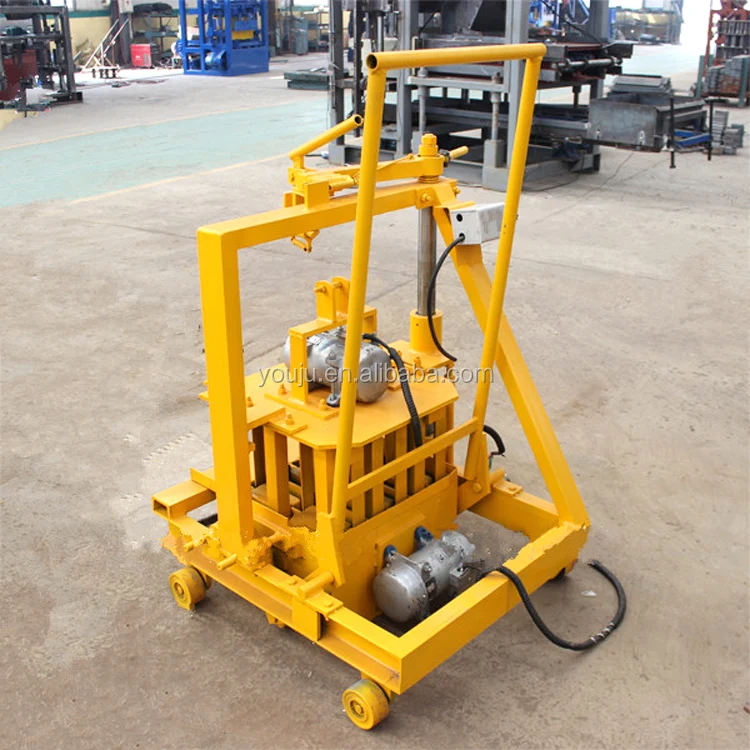
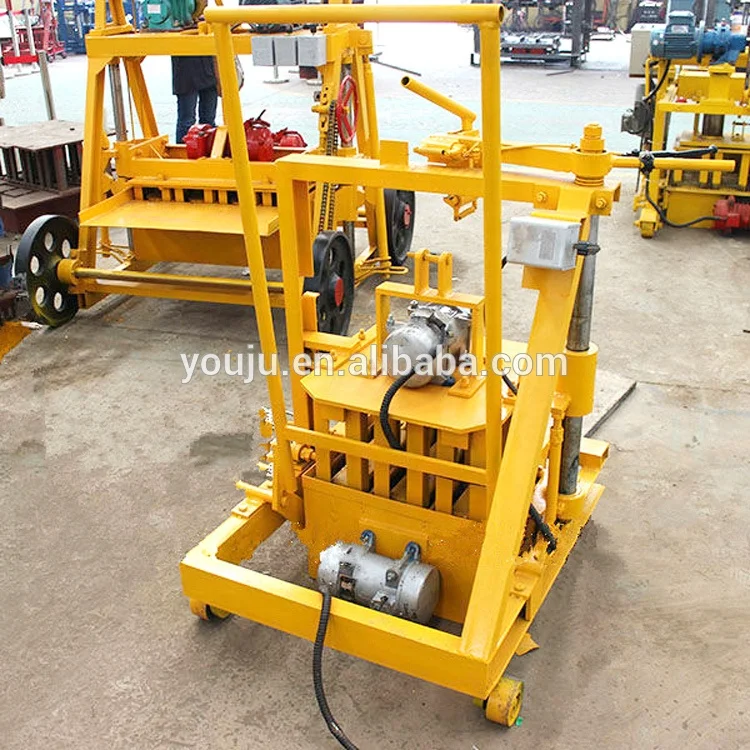
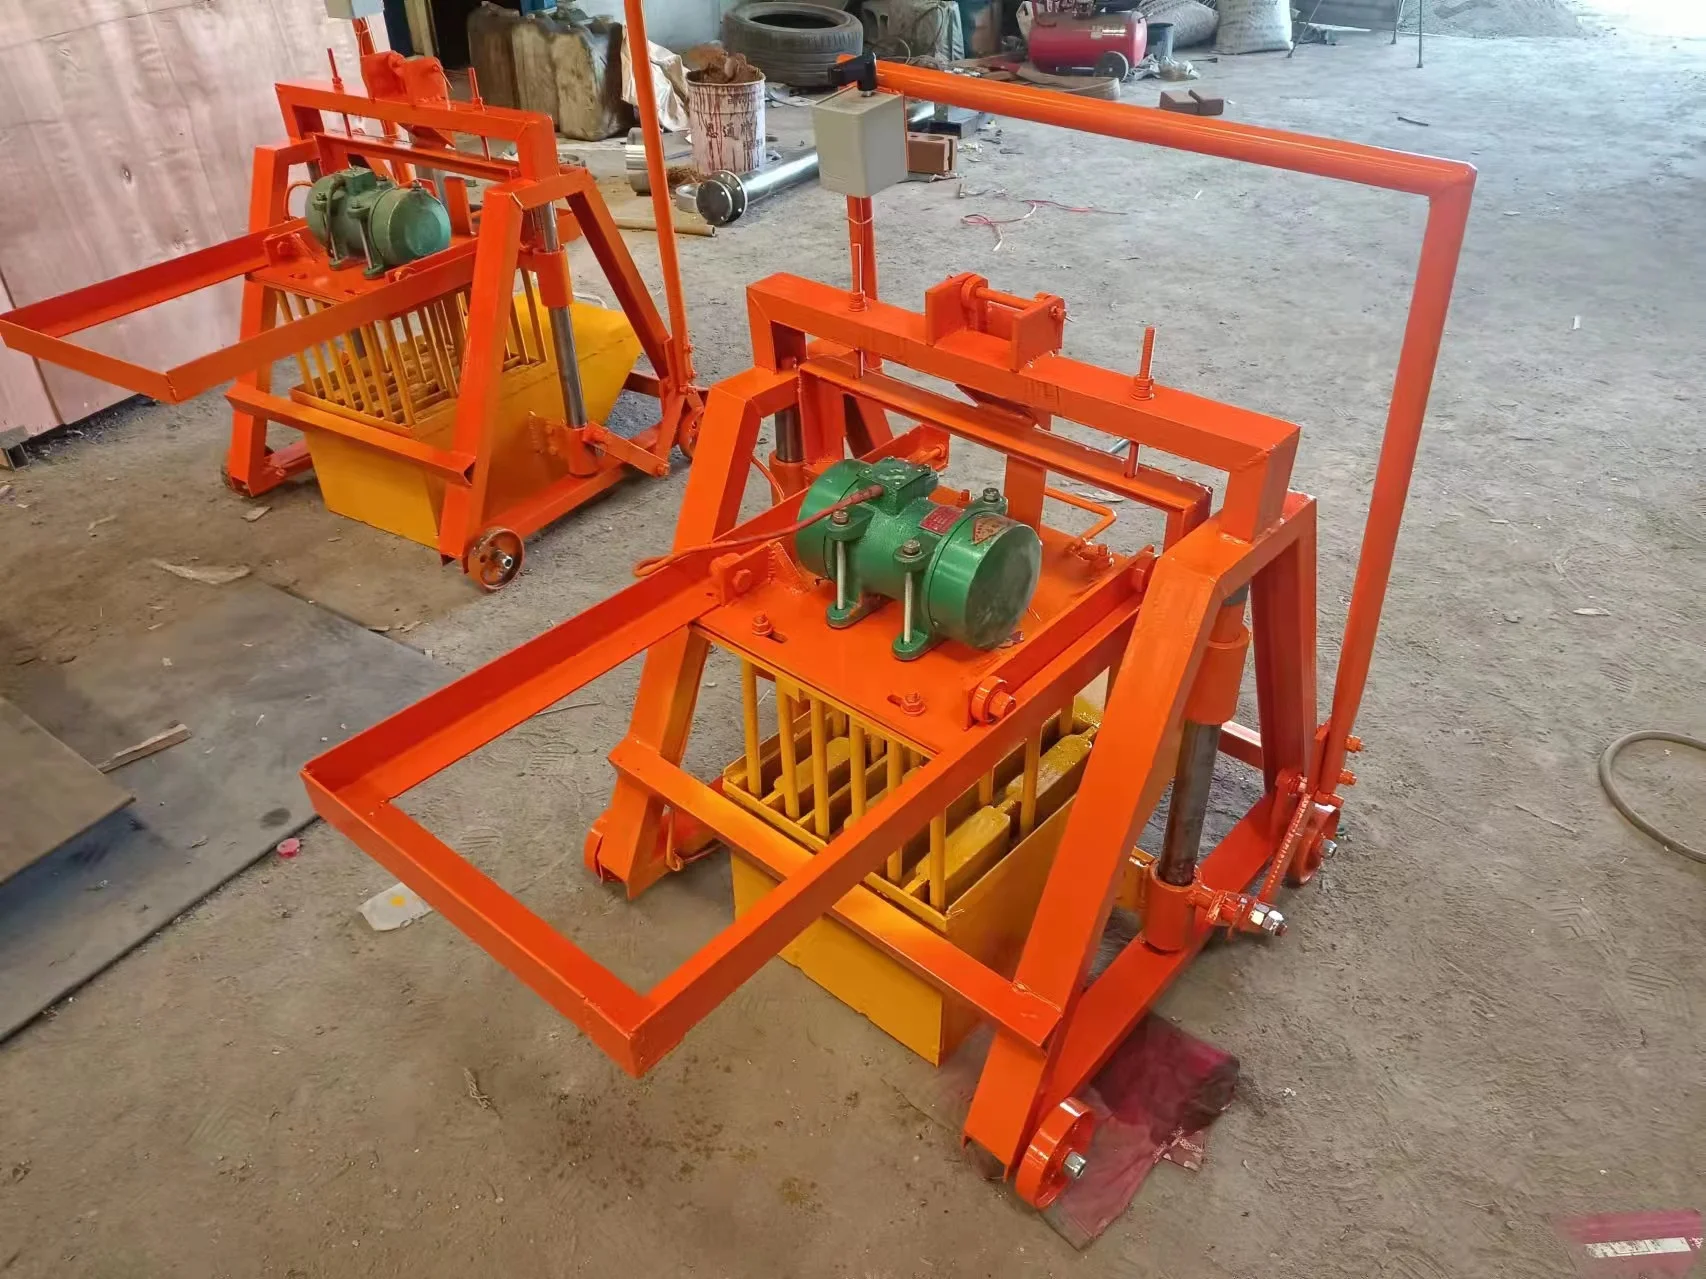
Description
Stocked for Fast Dispatch — QMJ2-45 mobile block machines sit in our Linyi warehouse with standard hollow brick moulds matched to the press, so your container loads within days, not weeks.
Technical Specifications
| Parameter | Value |
|---|---|
| Model | QMJ2-45 |
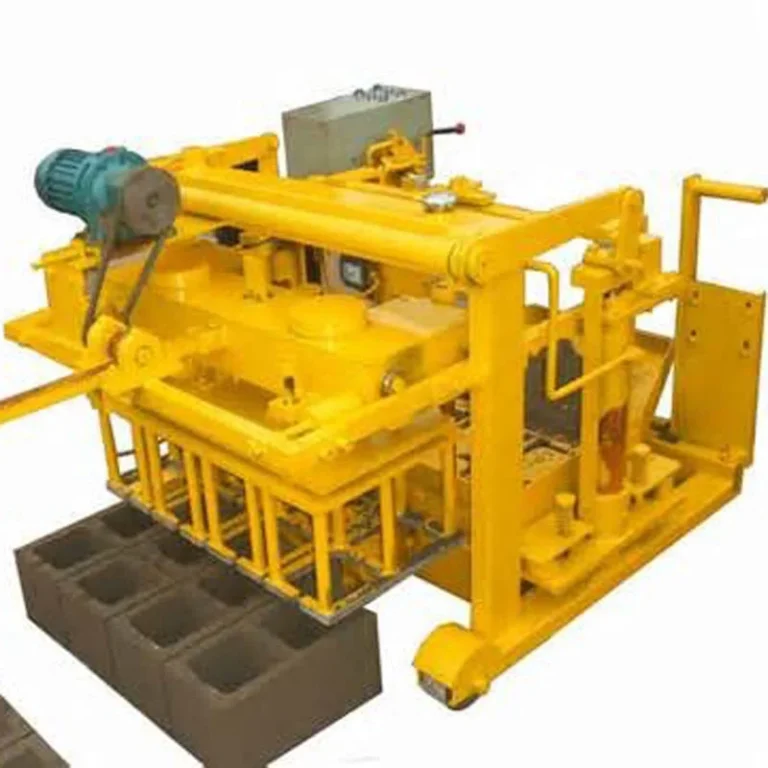
| Product Type | Mobile Egg-Laying Concrete Block Making Machine |
| Machine Type | Mobile / egg-laying (pallet-free) |
| Operation Mode | Manual |
| Power Source | Diesel engine |
| Workers Required | 1 to 3 |
| Cycle Time | 25–30 s per mould cycle |
| Output Capacity (400×200×200 mm hollow brick) | 160 pcs/h (2 pcs/mould) |
| Output Capacity (400×150×200 mm hollow brick) | 240 pcs/h (3 pcs/mould) |
| Output Capacity (400×100×200 mm hollow brick) | 320 pcs/h (4 pcs/mould) |
| Daily Output @ 8 hr (400×200×200 mm) | 1,280 pcs |
| Daily Output @ 8 hr (400×100×200 mm) | 2,560 pcs |
| Mould Change | Supported, multiple hollow brick formats |
| Pallet Size | N/A (pallet-free egg-laying design) |
| Automation Level | Manual |
| Certification | ISO 9001:2000, CE |
| Mould Format Options | 400×200×200, 400×150×200, 400×100×200 mm hollow brick |
Application Suitability
| Application | Material or Output |
|---|---|
| On-site hollow concrete block production | Cement, crushed stone, sand, water — no fixed plant required |
| Small-scale block supply for building contractors | 400×200×200 mm and 400×100×200 mm hollow blocks from local aggregate |
| Remote or off-grid construction projects | Diesel-powered egg-laying operation without pallet logistics |
| Low-investment entry into block manufacturing | Manual operation with 1–3 workers, multiple mould formats |
Why the Capacity Number on the Brochure Is Not What You Get on Site
Real daily output depends on the block format you actually run, not the headline figure.
I spent years dispatching machines from the Linyi workshops, and one pattern repeats: the buyer reads "320 pieces per hour" on the spec sheet and plans their whole project around it. But that figure only holds for the smallest hollow brick format in the mould range. Switch to the 400×200×200 mm block — the one most building sites actually order — and the same machine, same cycle time, produces half that number. When you source a mobile block machine in stock, the dispatch is fast, but if the capacity was never matched to your target format, you still end up short on the first day of production [NEED_CITE: block output calculation based on mould cavity count and cycle time].
Pallet-Free Operation Removes a Hidden Logistics Chain
The QMJ2-45 lays blocks directly onto the ground as it moves forward, which eliminates the entire pallet purchase, storage, and return loop that fixed-plant machines require. For a contractor working a remote housing project, this means the machine arrives, the operator mixes a batch, and blocks start curing on the slab within the first hour. No pallet racks to ship in the same container, no forklift to move stacks to a curing area, no pallet replacement budget to plan for the second year.
Stock Availability Means the Mould Match Happens Before Loading
When we pull a mobile block machine in stock from the warehouse, the standard hollow brick moulds — 400×200×200, 400×150×200, and 400×100×200 mm — are already paired and tested on that specific press. The mould cavity count determines the per-cycle output, and having all three formats in the container means you can start with the size the project demands today and switch to a different format next month without waiting for a second shipment [NEED_CITE: mould cavity count and cycle time relationship in egg-laying block machines].
Reading the Specs That Actually Matter for Egg-Laying Machines
The 25–30 second cycle time is the rhythm the operator sets: feed the mix, vibrate, move forward, repeat. This number holds across all three hollow brick formats because the vibration and compaction phase does not change — what changes is how many blocks drop per cycle. The diesel engine power source is the reason this machine works on sites with no grid connection, but it also means the operator controls throttle manually, which directly affects vibration consistency. Mould change is mechanical and supported on-site; you unbolt the current mould, lower the new one, and lock it in. The manual operation mode keeps the machine simple and the maintenance list short, but it also means output consistency depends on the operator maintaining a steady rhythm and the mix staying within the right moisture range for local aggregate [NEED_CITE: moisture content and compaction quality in manual block production].
The Cost of Ignoring the Pallet Question Until the Machine Arrives
Buyers who select a fixed-plant machine without checking their curing area footprint and forklift capacity often discover that the pallets do not fit the racks they already own. For an egg-laying machine like the QMJ2-45 this problem does not exist — the ground is the pallet — but buyers who were originally quoted a pallet-based machine sometimes switch to mobile at the last minute and then find they never planned a flat, level casting area on site. The blocks cure unevenly on rough ground, and the complaint lands on the machine rather than the preparation [NEED_CITE: ground preparation requirements for egg-laying block machines].
Why Dispatch Timing Matters More Than You Think
The QMJ2-45 is held in stock with standard hollow brick moulds already matched, so the container loading plan is confirmed at quotation stage rather than after production. The machine is dismantled for shipment to fit efficiently, and packing photographs are sent before the container doors close. Arrival estimates are quoted upfront based on your destination port, because a machine that sits in a warehouse for six extra weeks is a machine that misses the building season. Every unit dispatched carries a factory test record showing cycle times on the exact mould formats in the container, so there is no commissioning guesswork when it arrives. Documentation includes the machine specification sheet, mould drawing and format list, hydraulic and electrical schematic where applicable, operation and maintenance manual, and wear parts list — all tied to the specific machine serial number.
Documentation & Verification
- Factory test record on the three standard hollow brick formats before dispatch
- Mould drawing and cavity count list matching the moulds in your container
- Operation manual with diesel engine maintenance intervals for manual operation
- Packing photographs showing dismantling and loading sequence before doors close
- Voltage and control confirmation sheet — not applicable for diesel, but power specs verified
Installation, Commissioning & Support
- Flat, level casting area required — the egg-laying design needs a smooth concrete slab or compacted ground to move across
- Diesel fuel supply and basic tool kit for mould change — no electrical grid connection needed
- Machine arrives dismantled; reassembly is bolting the frame together and mounting the first mould
- First batch run with operator present to confirm 25–30 s cycle rhythm on your local mix
- Spare mould wear parts list included so you can order replacements before the first set wears through
What to Send with Your Inquiry
Tell us which hollow brick format your project specifies and the daily volume you need to hit. Share the local aggregate type — sand source, stone size, any clay or silt content — because the mix behaviour changes the cycle rhythm. If the site has no grid power, confirm the diesel supply arrangement. We will reply with stock status, the exact moulds in the container, dispatch lead time, and an arrival estimate for your port.
Frequently Asked Questions
Q: What is the actual dispatch lead time for the QMJ2-45 and its standard moulds?
A: The QMJ2-45 and the three standard hollow brick moulds — 400×200×200, 400×150×200, and 400×100×200 mm — are held in stock at our Linyi warehouse. Once the container loading plan is confirmed and the quotation accepted, the machine is dismantled, packed, and photographed before dispatch. Lead time from order to port is typically measured in days, not weeks, though exact timing depends on container availability and your destination.
Q: How is the machine dismantled and loaded into a container for shipment?
A: The QMJ2-45 is broken down into its main frame, mould assembly, and diesel engine for container loading. This reduces the footprint and protects the vibration components during transit. Packing photographs are taken at each stage and sent to the buyer before the container doors are sealed, so you know exactly what to expect when the container is opened at your site.
Q: Which hollow brick mould sizes are kept in stock versus made to order?
A: The 400×200×200 mm, 400×150×200 mm, and 400×100×200 mm hollow brick moulds are standard stock items shipped with the QMJ2-45. Other formats can be manufactured to order, but these three cover the majority of building site requirements. Additional moulds, if ordered at the same time, can be loaded in the same container to save on freight.
Q: What is the realistic daily output for my target block format at 25–30 s cycle time?
A: At 25–30 seconds per cycle, the QMJ2-45 produces 160 pieces per hour on the 400×200×200 mm format, 240 per hour on the 400×150×200 mm, and 320 per hour on the 400×100×200 mm. Over an 8-hour shift, that translates to 1,280, roughly 2,400, and 2,560 blocks respectively. The number you should plan around is the one tied to the format your project actually uses.
Q: Can additional mould formats be shipped in the same container as the machine?
A: Yes. The QMJ2-45 container has space for additional moulds beyond the three standard formats. If your project requires a fourth or fifth hollow brick size, those moulds can be manufactured and loaded alongside the machine at the same dispatch point, arriving together so your operator can switch formats from day one without waiting for a separate shipment.