
Description
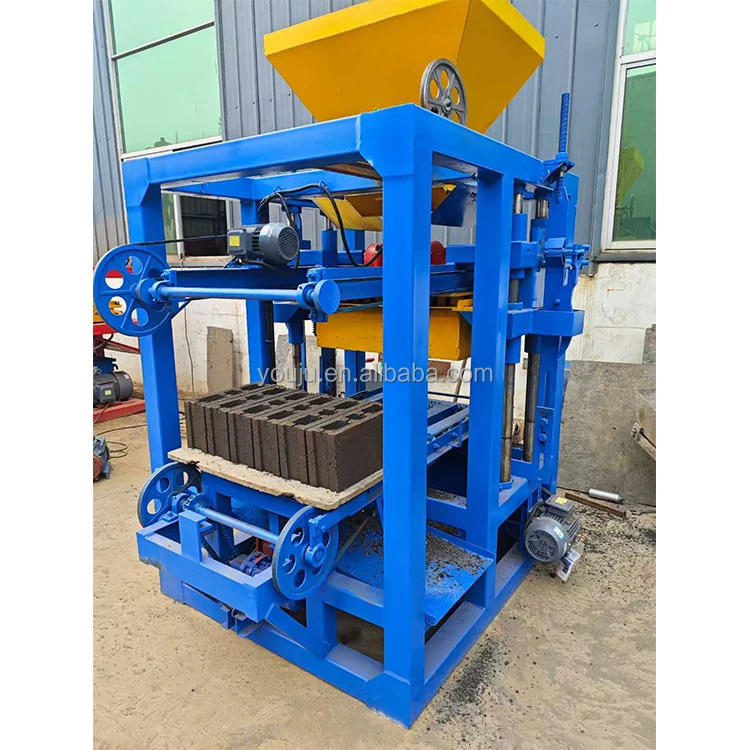
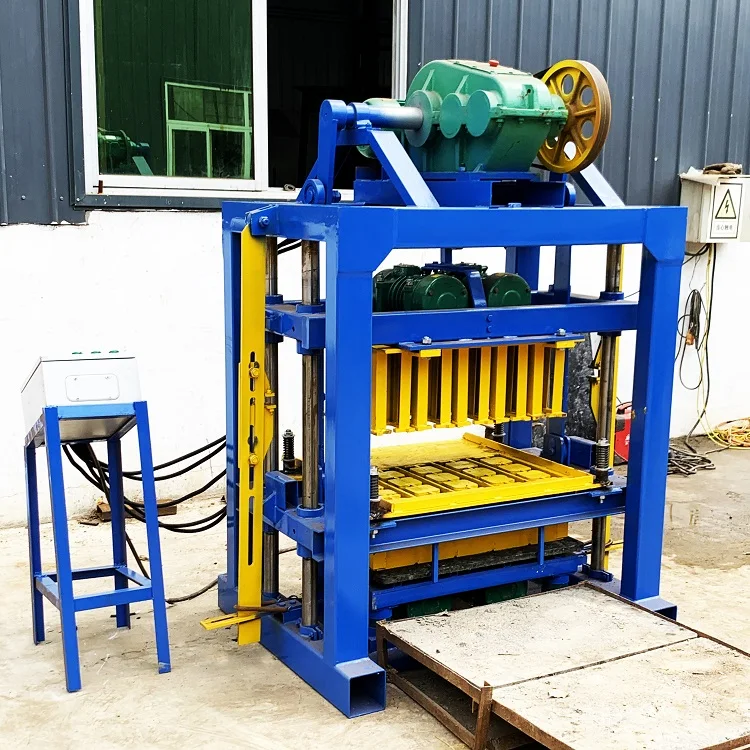
Stocked and ready for fast dispatch — this stationary block machine ships with container loading plans and arrival estimates confirmed before payment, so your project timeline stays intact.
Technical Specifications
| Parameter | Value |
|---|---|
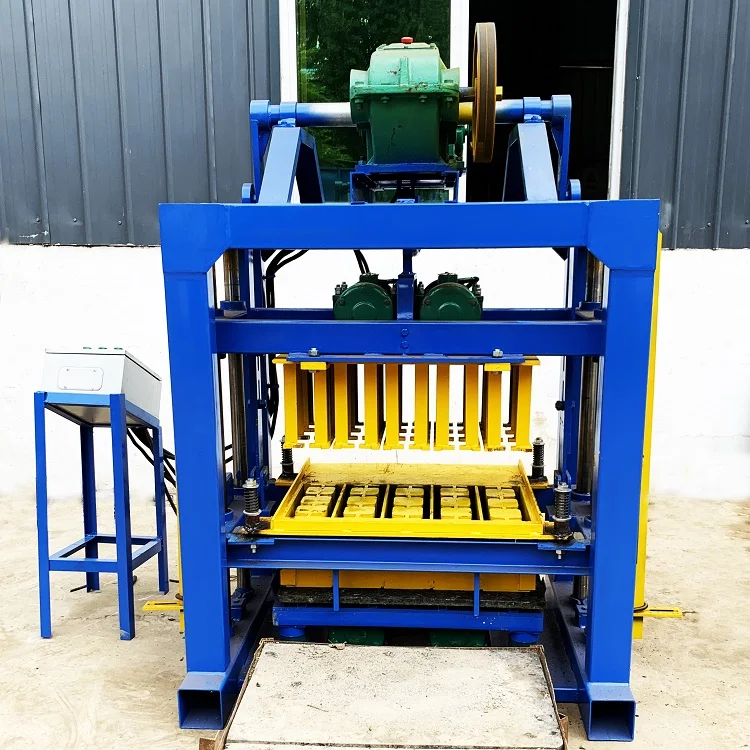
| Model | QTJ4-40 |
| Product Type | Hydraulic Motor Concrete Block Making Machine |
| Main Vibration Form | Platform Vibration |
| Vibration Frequency | 2800 r/min |
| Pallet Size | 850×450 mm |
| Machine Weight | Approximately 1,000 kg |
| Overall Dimensions | 1350×1460×1800 mm |
| Worker Required | 1–3 people |
| Mould Change System | Top die push and pull with automatic scraper |
| Raw Material Compatibility | Concrete, cement, fly ash, crushed stone, sand, gravel, slag |
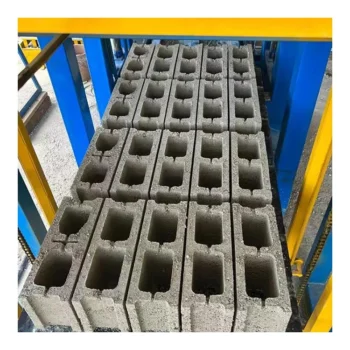
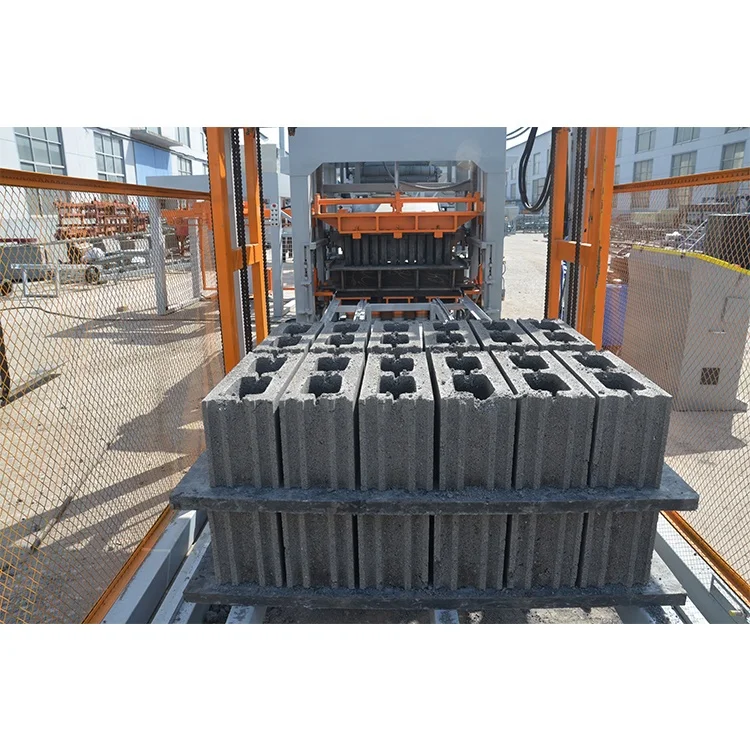
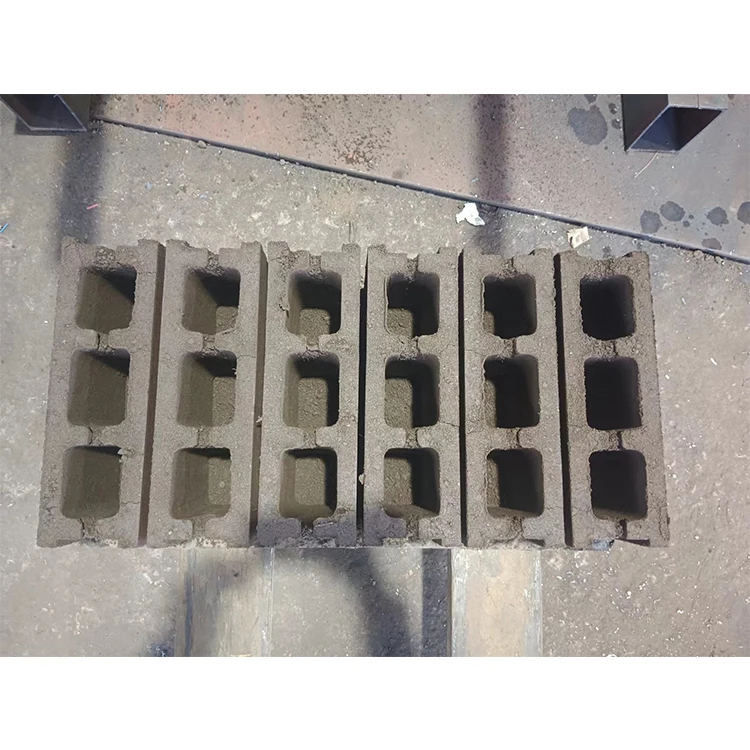
| Production Capacity (400×200×200 mm hollow block) | 4 pcs/mould, approx. 360 pcs/h |
| Production Capacity (400×150×200 mm solid block) | 5 pcs/mould, approx. 500 pcs/h |
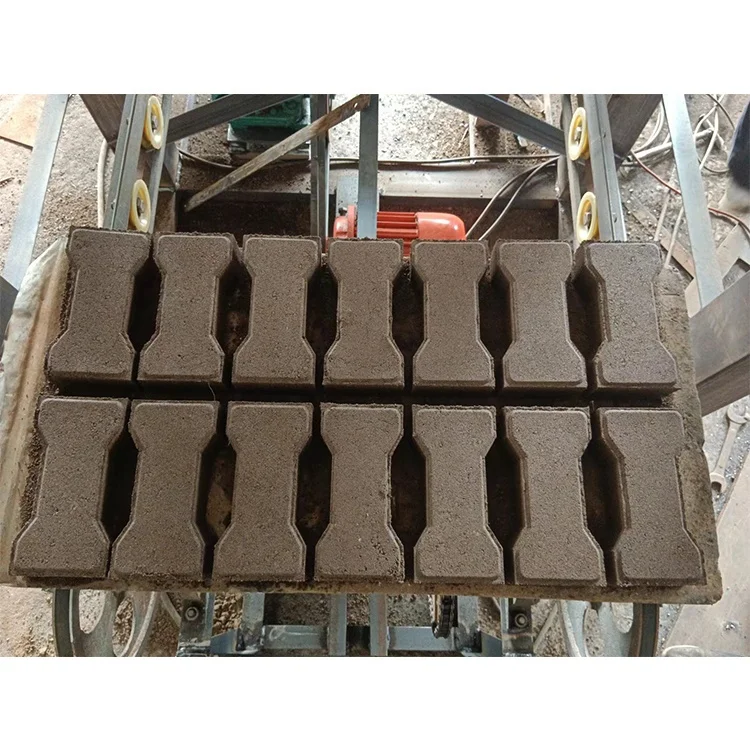
| Production Capacity (225×112.5×60 mm paver) | 9 pcs/mould, approx. 900 pcs/h |
| Certification | CE |
Application Suitability
| Application | Material or Output |
|---|---|
| Housing project hollow block production | Crushed stone, sand, and cement mix |
| On-site interlocking brick manufacturing | Fly ash blended with local aggregate |
| Paver and curbstone supply for local contractors | Cement, dust, and gravel combinations |
| First block plant for entrepreneurs | Standard concrete mixes with 8–10% cement ratio |
Why a Stocked Machine Can Still Arrive Late
Dispatch timing depends on what happens between the order and the port.
A stationary block machine in stock does not guarantee it reaches your site on schedule. Voltage mismatches discovered after arrival, pallet sizes that do not fit your curing racks, or control panels displaying in the wrong language can stall commissioning for days. I have watched machines sit in yards because the frequency was confirmed too late, and the project deadline passed while the electrician waited for a transformer [NEED_CITE: electrical frequency compatibility for exported machinery]. These are not machine defects — they are ordering gaps that a stocked model alone cannot fix.
How Stock Status Translates to Your Project Timeline
When a buyer commits to a construction deadline, the lead time conversation must cover more than warehouse availability. A stocked QTJ4-40 can leave the factory within days, but container loading, port clearance, and ocean transit add their own schedule. The realistic planning window starts from dispatch confirmation, not from the day you sign the order. This stationary block machine in stock is dismantled into loadable sections that fit standard container dimensions, and the packing plan is photographed and shared before the doors close.
What "Ready to Ship" Actually Means on the Dock
Stock does not mean the machine rolls onto a truck untouched. Hydraulic lines are depressurized, the vibration platform is secured, and the mould is crated separately to prevent transit damage. Every fast delivery commitment includes a loading sequence that accounts for weight distribution inside the container. Buyers who need the machine operational within weeks of arrival should confirm pallet specifications and voltage settings before the crate is sealed [NEED_CITE: container loading standards for heavy industrial equipment].
Reading the Specs That Matter for Daily Output
Platform vibration at 2800 r/min works together with the hydraulic motor to compact the mix uniformly across the mould cavity. The pallet size of 850×450 mm determines how many blocks cure per rack tier — if your existing forklift or curing area was built around a different pallet dimension, the mismatch compounds every shift. The top die push-pull system with automatic scraper keeps mould changes manageable for a small crew, but the actual swap time depends on whether your operators have the correct spanner set and whether the replacement mould matches the machine’s bolt pattern.
The Cost of Skipping the Pre-Shipment Checklist
Ordering a stocked machine without confirming voltage and frequency is the most common reason commissioning stalls on arrival. Pallet material matters too — wooden pallets warp in humid curing yards, and if the specification was never discussed, replacements may not be locally available. Moulds designed for one aggregate gradation will produce weak blocks when the local sand carries high clay content, cutting usable output well below the quoted figure [NEED_CITE: aggregate quality impact on concrete block compressive strength]. These issues surface after the machine is already on your site, where fixes take longer and cost more.
What Separates a Shipment from a Working Machine
Configuration is confirmed against your actual mix design and target block format before the machine is crated, not pulled from a default catalogue setting. Pallet size and material are verified against your curing area dimensions and forklift capacity so nothing arrives incompatible. Voltage, frequency, and control language are locked in before production so the electrician can connect power on day one. Packing photographs and a container loading plan are provided before dispatch, giving you a documented record of what went inside. Factory testing covers the specific mould and block format you ordered, not a generic run.
Documentation & Verification
- Capacity calculation sheet stating output per confirmed block format
- Voltage, frequency, and PLC display language confirmation record
- Pallet specification matched to your curing area and forklift
- Factory test record on your selected mould before dispatch
- Packing photographs and container loading plan before shipment
- Operation and maintenance manual with wear parts list
Installation, Commissioning & Support
- Foundation must be level and cured to support the 1350×1460 mm footprint without vibration transfer
- Dedicated power circuit matching confirmed voltage and frequency before the machine is uncrated
- Hydraulic lines reconnected and platform vibration tested during on-site commissioning
- Mould bolt pattern verified and first production run supervised with your crew
- Pallet feeding sequence adjusted to match your curing rack layout and forklift reach
Getting a Reliable Dispatch Date
To move from inquiry to a firm shipment date, share your target block format and daily volume requirement, your local aggregate type and cement availability, and your site’s voltage and frequency standard. If you already have curing racks and a forklift, send the pallet dimensions they accept. These details let us confirm whether the stocked unit ships as-is or needs a pallet or voltage adjustment before it leaves the factory.
Frequently Asked Questions
Q: What is the real daily output for my specific block format?
A: Output varies by block size and mix. For a 400×200×200 mm hollow block, the QTJ4-40 produces approximately 360 pieces per hour. For a 225×112.5×60 mm paver, it reaches roughly 900 pieces per hour. We provide a capacity sheet tied to your chosen format so the number reflects your actual product, not a generic headline figure.
Q: Is the machine in stock and how fast can it ship?
A: Stocked units can be prepared for dispatch within days of order confirmation. The timeline from factory to your port depends on container availability and sailing schedules. We confirm the loading plan and provide packing photographs before the container doors close so you can track the shipment.
Q: Will the voltage and control language match my country?
A: Voltage, frequency, and PLC display language are confirmed before the machine is crated. We lock these specifications during the order process so the control panel and motor match your site’s electrical standard and your operators can read the interface on the first day.
Q: How is the machine loaded into a container for shipment?
A: The QTJ4-40 is dismantled into sections that fit standard container dimensions. The vibration platform is secured, hydraulic lines are depressurized, and the mould is crated separately. A loading plan is prepared to manage weight distribution, and photographs are taken before dispatch.