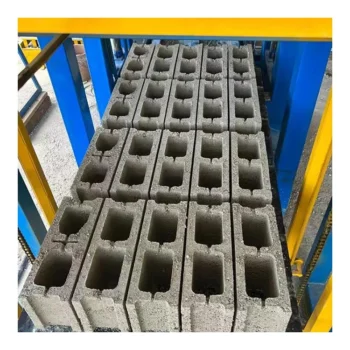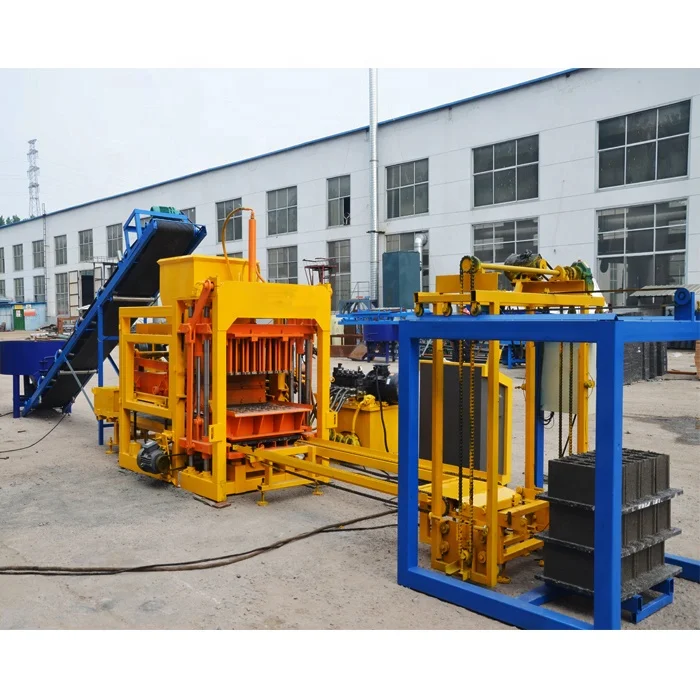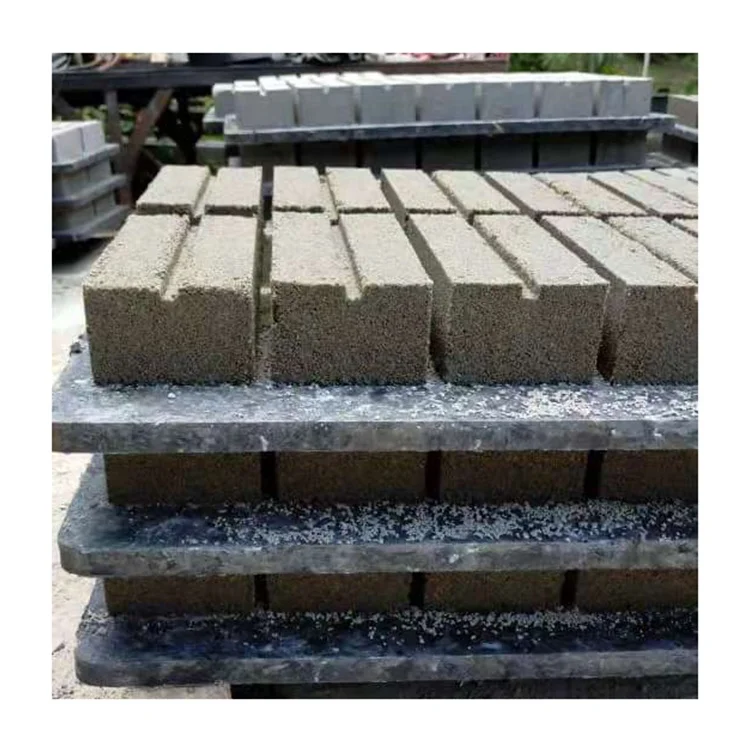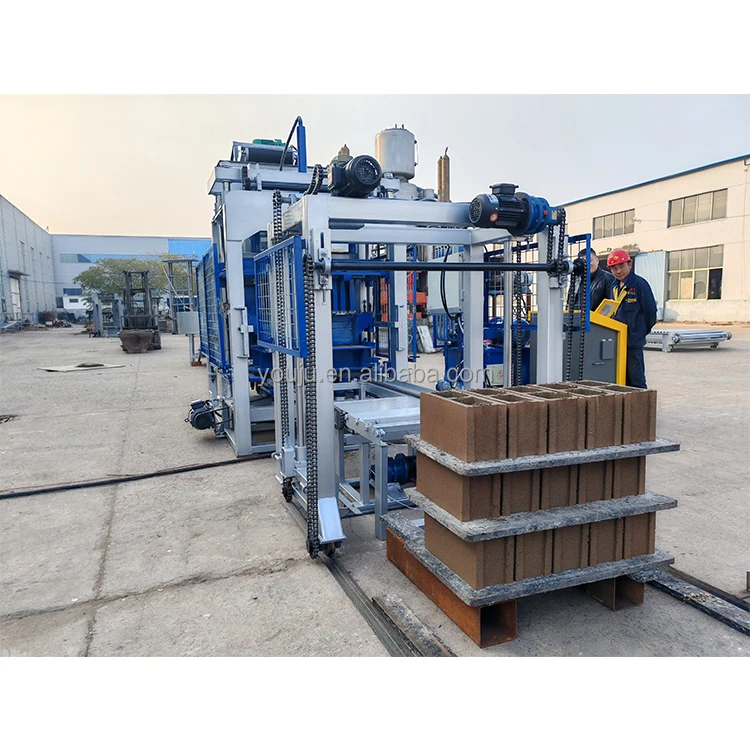



Description
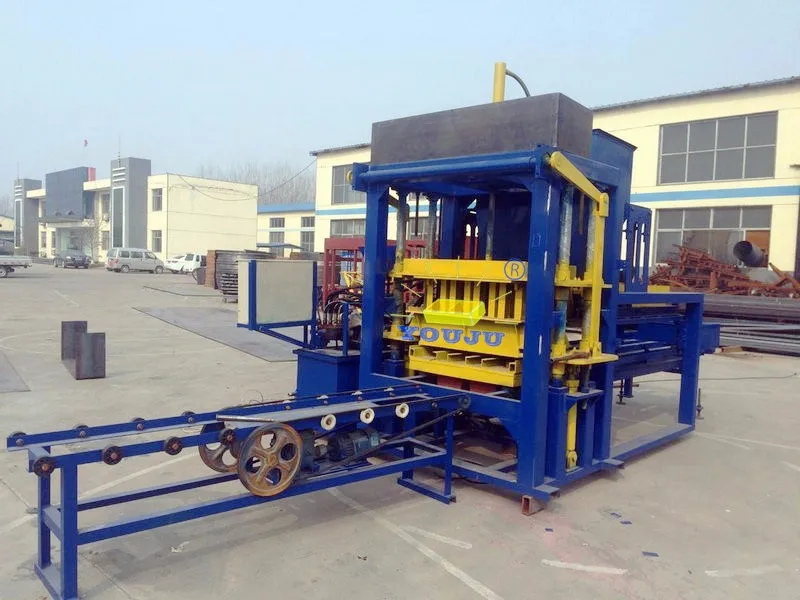
Matched system dispatch — Every QT4-20 block machine in stock ships as a press-and-pallet system verified against your target block format before the container is sealed.
Technical Specifications
| Parameter | Value |
|---|---|
| Model | QT4-20 |
| Product Type | Hydraulic Concrete Block Making Machine |
| Overall Dimensions (L×W×H) | 7100×1600×2610 mm |
| Rated Pressure | 16–21 MPa |
| Main Vibration Form | Platform Vibration |
| Vibration Frequency | 4600 r/min |
| Vibration Force | 40 kN |
| Pallet Size | 1020×570 mm |
| Molding Cycle | 15–25 s |
| Overall Power | 27.5 kW |
| Total Mass | 5 T |
| Demolding Method | Hydraulic |
| Molding Area | 400×800 mm |
| Factory Area | 500 m² |
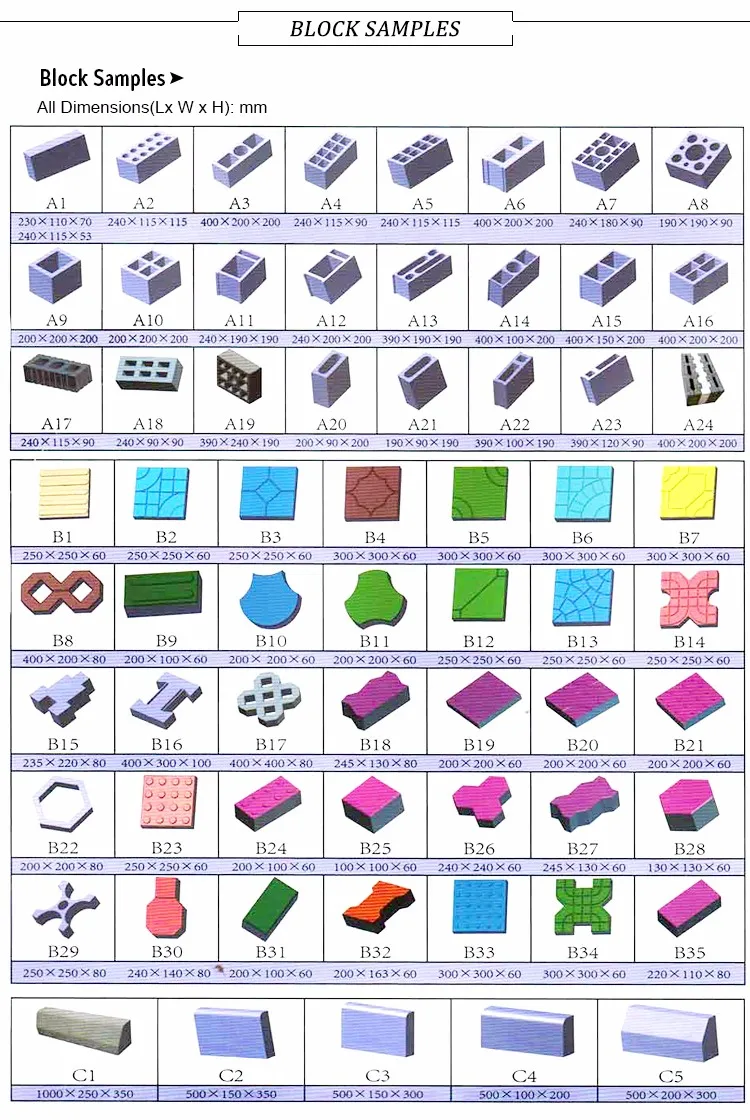
| Output Capacity (Hollow brick 400×200×200 mm, 4 pcs/mold, 15–20s cycle) | 7,200–9,600 pcs/day |
| Output Capacity (Porous brick 240×115×90 mm, 14 pcs/mold, 15–20s cycle) | 20,200–26,800 pcs/day |
| Output Capacity (Standard brick 240×115×53 mm, 28 pcs/mold, 15–17s cycle) | 47,400–53,700 pcs/day |
| Control System | PLC (basis not stated in source — confirm brand and language options) |
| Voltage & Frequency | Configurable (confirm before order) |
| Automation Level | Configurable (confirm degree of automation) |
| Raw Materials | Crushed stone, sand, cement, dust, fly ash, gravel, slag |
Application Suitability
| Application | Material or Output |
|---|---|
| Hollow block production for housing projects | Crushed stone, sand, cement — 400×200×200 mm format |
| Solid block manufacturing for load-bearing walls | Sand, gravel, cement mix designs |
| Porous brick runs for infill and partition walls | Fly ash, cement, fine aggregate — 240×115×90 mm format |
| Standard brick batches for masonry contractors | Cement, dust, slag — 240×115×53 mm format |
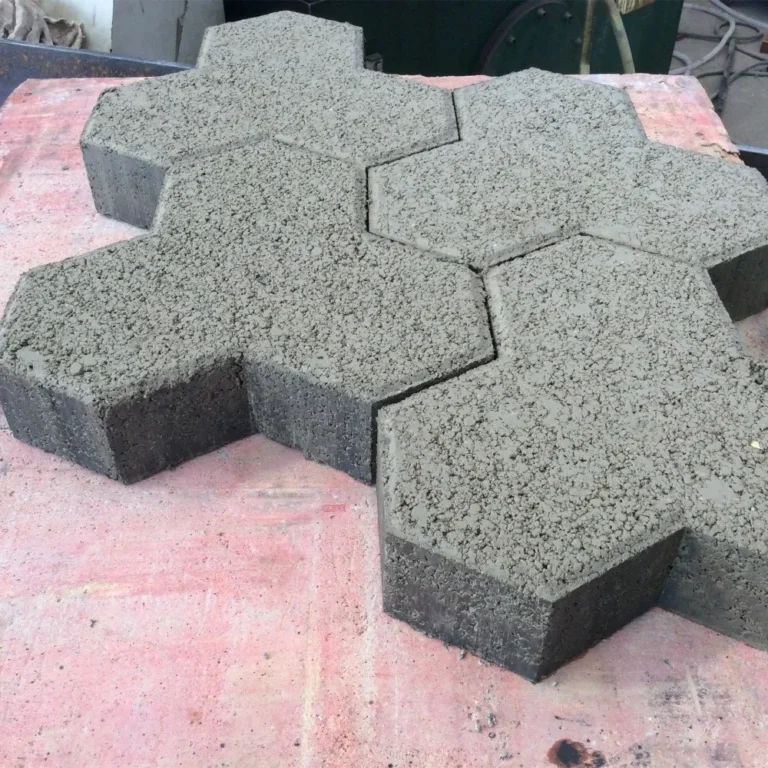
| Paver production for walkways and yards | Crushed stone, sand, cement with pigment additives |
What the Cycle Time Figure Actually Means on Site
A QT4-20 block machine in stock can leave the factory quickly, but a 15–25 second molding cycle only translates to real output when your mix design, pallet circulation speed, and curing rack capacity all keep pace with the press.
I once watched a contractor in the Gulf receive a mid-range press on schedule, only to discover the local desert sand required a completely different vibration profile than the standard aggregate the machine was tuned for at the factory. The first two weeks of production ran at roughly half the expected volume while we re-tuned parameters on site. That delay had nothing to do with shipping speed and everything to do with configuration [NEED_CITE: aggregate grading standards for concrete block production]. Confirming your raw material sample before dispatch prevents this kind of lost time.
Dispatch Timing and Container Loading Clarity
When your project timeline is fixed, knowing exactly when the QT4-20 block machine in stock will be dismantled, loaded, and dispatched matters more than any catalogue promise. We confirm stock status and lead time in writing before the proforma invoice is issued, so there is no ambiguity between order and departure.
How the Machine Arrives at Your Port
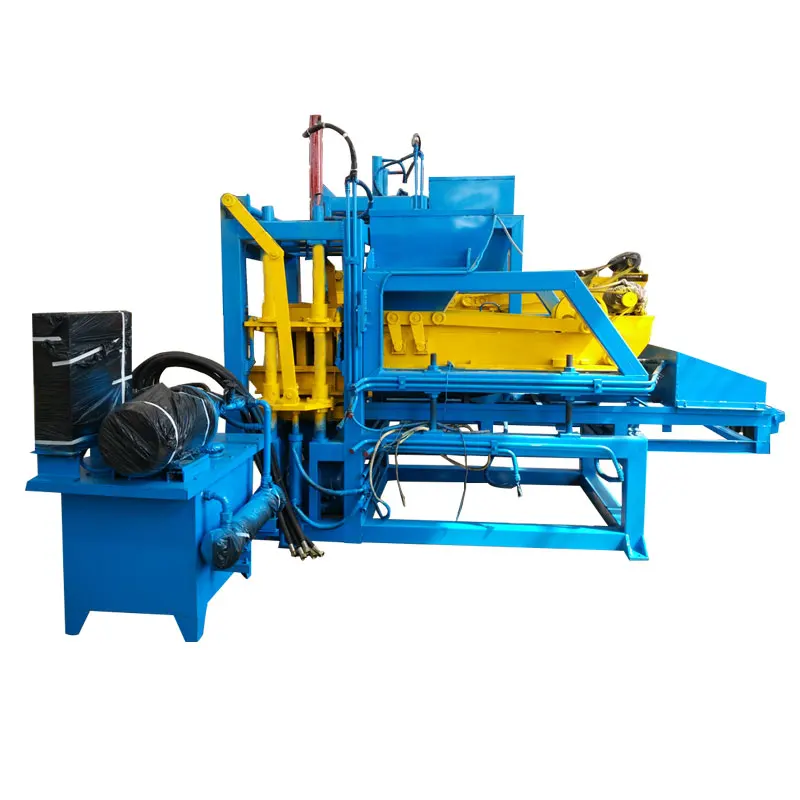
The QT4-20 ships dismantled into components that fit standard container dimensions. A loading plan is provided showing how the main frame, hydraulic station, vibration platform, and pallet feed system are secured for transit. Packing photographs are taken before the container doors close, and customs documentation is prepared to match the destination port requirements [NEED_CITE: container loading standards for heavy industrial machinery].
Reading the Numbers That Matter for Your Block Format
The rated pressure range of 16–21 MPa combined with 40 kN vibration force at 4600 r/min determines how densely the concrete is compacted in the mold cavity. For hollow blocks, this pairing must produce enough green strength for the block to hold its shape during pallet transfer and early curing. The 1020×570 mm pallet size defines how many cavities fit per cycle — and must match the forklift and curing rack spacing you already have on site, not just the machine footprint. Molding area of 400×800 mm sets the maximum mold envelope, which constrains how many standard bricks fit per cycle versus hollow blocks. Overall power at 27.5 kW means the electrical supply must be confirmed for voltage and frequency before the motor windings are wound at the factory.
The Cost of Overlooking Pallet and Voltage Details
Buyers who confirm the press specifications but leave pallet size and electrical configuration to default settings often face delays that no amount of stock availability can fix. A pallet that does not match your existing curing racks forces you to rebuild the curing area or handle blocks manually off non-standard boards. Voltage confirmed after production means rewinding motors or adding transformers — both of which push commissioning back by weeks [NEED_CITE: industrial voltage and frequency standards by export market].
Why Buyers Source This Machine Here
Block machinery is the single focus of this operation, so the QT4-20 is specified as a matched press, mold, and pallet system rather than assembled from unrelated suppliers. Dispatch lead time is quoted before the order is placed, not after. Container loading plans are provided so you know exactly how the machine arrives. Voltage, frequency, and PLC display language are confirmed in advance to avoid commissioning delays. Mould design covers the block formats your market actually sells, with custom drawings available.
Documentation & Verification
- Factory test record run on your specified block format before dispatch
- Machine specification sheet with confirmed voltage and frequency
- Pallet specification matched to your curing area dimensions
- Packing photographs taken before container doors close
- Customs documentation prepared for destination port requirements
- Operation and maintenance manual in confirmed language
Installation, Commissioning & Support
- Foundation plan sized to the 7100×1600 mm footprint and 5 T operating mass
- Electrical connection matching confirmed voltage and the 27.5 kW total power draw
- Dismantled components reassembled on site with hydraulic station and vibration platform aligned
- First production run supervised with molding cycle tuned to your local aggregate
- Operator training covering mold change procedure and PLC interface navigation
- Wear parts list provided with hydraulic seal and vibration motor replacement intervals
Before You Send the Inquiry
Share the block formats your market requires, the daily volume you need per format, and the raw materials available locally — including a sample if possible. Confirm your site voltage, frequency, and the language your operators will use on the PLC display. If you already have pallets, forklifts, or curing racks in place, send their dimensions so the system is matched before the machine ships.
Frequently Asked Questions
Q: Is the QT4-20 currently in stock or what is the lead time?
A: Stock status for the QT4-20 block machine in stock is confirmed in writing before you receive the proforma invoice. If the unit is allocated, we provide the exact dispatch date and container loading schedule so you can plan around your project deadline rather than guessing at arrival timing.
Q: How is the machine dismantled and loaded into containers?
A: The QT4-20 is broken down into main frame, hydraulic station, vibration platform, and pallet feed components for container loading. A written loading plan shows placement and securing method. Packing photographs document condition before the container is sealed.
Q: Can you match my country’s voltage and frequency standard?
A: Voltage and frequency are confirmed with you before production begins. The 27.5 kW overall power requirement must align with your site supply, and motor windings are set accordingly. PLC display language is also locked in at this stage to avoid commissioning issues on arrival.
Q: Which block formats and moulds ship with the press from stock?
A: Standard moulds available from stock are confirmed at inquiry stage based on your target block format. Custom moulds require a separate lead time. The molding area of 400×800 mm defines the maximum mold envelope, and cavity count varies by block size.