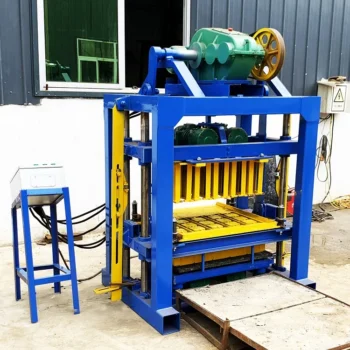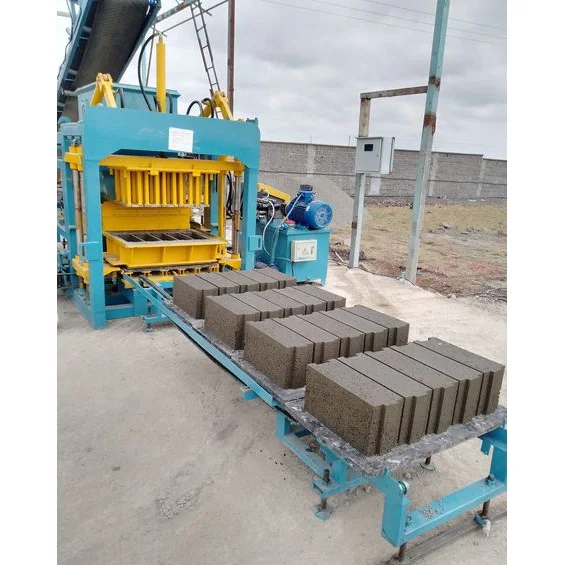



Description
Container-Ready Dispatch — Every QTJ4-25 unit is checked against the destination port’s unloading conditions before we finalize the loading plan, because a machine that cannot come out of the container is a machine that cannot produce.
Technical Specifications
| Parameter | Value |
|---|---|
| Model | QTJ4-25 |
| Product Type | Semi-Automatic Concrete Block Making Machine |
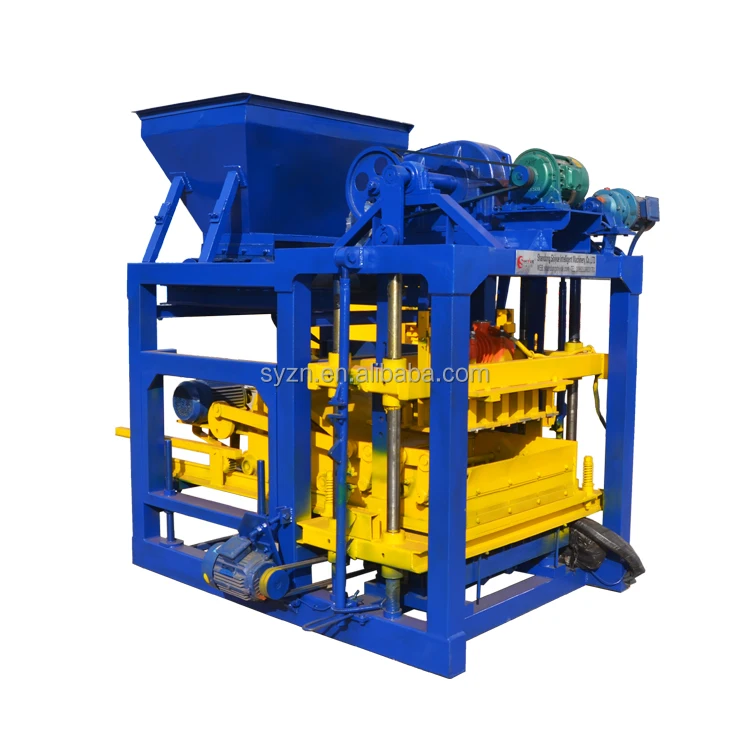
| Overall Dimensions (L×W×H) | 3060×1730×2580 mm |
| Total Weight | 4 T |
| Vibration Force | 45 kN |
| Cycle Time | 25 s |
| Pallet Size | 850×550 mm |
| Block Height Range | 40–280 mm |
| Workshop Area | 50–150 m² |
| Material Storage Area | 300–500 m² |
| Belt Conveyor Length | 8 m |
| Mixer Model | JQ500 |
| Motor Brand | Siemens or ABB |
| Control System | Electric control (PLC availability to be confirmed) |
| Voltage & Frequency | 380V, 3-phase, 50Hz (customizable) |
| Automation Level | Semi-automatic |
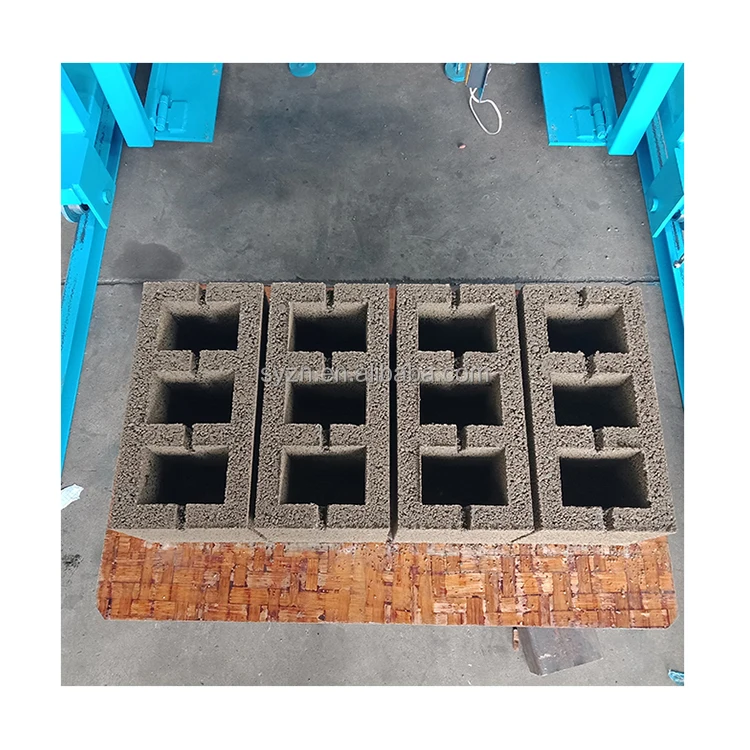
| Output Capacity | 480 pcs/h (basis: 400×200×200mm hollow block, 4 pcs/mould) |
| Output Capacity | 600 pcs/h (basis: 400×150×200mm hollow block, 5 pcs/mould) |
| Output Capacity | 840 pcs/h (basis: 400×100×200mm hollow block, 7 pcs/mould) |
| Output Capacity | 2880 pcs/h (basis: 240×115×53mm solid brick, 24 pcs/mould) |
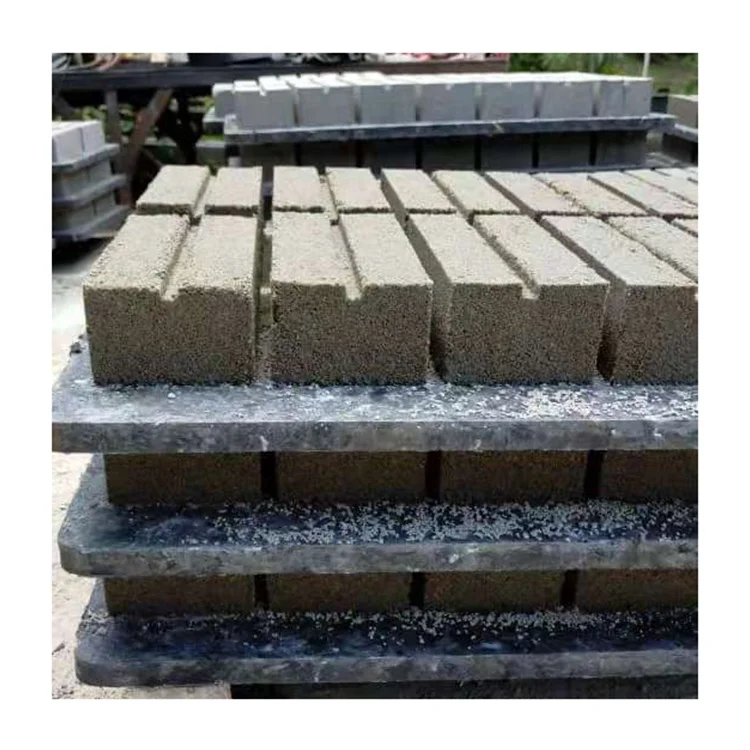
| Mould Compatibility | Hollow, solid, paver, interlocking, curbstone, grassed, revetment brick; custom design available |
| Warranty | 1 year (excluding wearing parts) |
Application Suitability
| Application | Material or Output |
|---|---|
| Small to medium block plant | Hollow and solid blocks from crushed stone, sand, and cement |
| On-site construction production | Pavers and interlocking bricks for contractor project use |
| First block plant startup | Semi-automatic operation with lower initial capital outlay |
| Format diversification | Curbstone, grassed brick, and colored paver with mould change |
| Revetment and slope work | Revetment brick from local aggregate blends |
What "In Stock" Actually Means for the QTJ4-25 Block Machine
A stocked machine still needs a confirmed voltage, control language, and pallet spec before it enters the container.
I have watched a QTJ4-25 block machine in stock sit on a dock for days because the buyer’s forklift could not handle the pallet size they assumed would ship. The machine was ready, but the supporting details were not. Fast dispatch only matters when every variable around the machine has been locked down before it leaves the factory floor [NEED_CITE: common commissioning delays in concrete block machinery imports].
Dispatch Timing and Container Loading Sequence
When a buyer needs a QTJ4-25 block machine in stock shipped quickly, the first thing I check is dismantling sequence against container dimensions. The main press frame, mixer, belt conveyor, and pallet stack each have a specific loading order inside the container so nothing shifts during sea transit. Skipping this sequence means rearranging cargo at the destination port, which costs more than taking an extra day to plan it right.
Arrival Estimate and Port Unloading Reality
The arrival estimate we quote upfront is based on the shipping line’s published schedule, not a best-case guess. Once the container lands, the buyer needs equipment that matches the machine’s 4-ton weight and the dimensions of the dismantled components. I once sent a machine to a Middle East port where the buyer had no heavy forklift available, and the unloading delay added significant cost to the project timeline [NEED_CITE: port handling equipment requirements for heavy industrial machinery].
Reading the Specifications for Production Reality
The 25-second cycle time applies to a single mould press, and actual daily output depends entirely on which block format the buyer is running. At 400×200×200mm hollow blocks with 4 pieces per mould, the rate is 480 pieces per hour. Switch to 240×115×53mm solid bricks with 24 pieces per mould, and the same cycle yields 2,880 pieces per hour. The vibration force of 45 kN must be matched to the buyer’s mix design and local aggregate; too weak a mix with this force level produces crumbling edges, while too rich a mix wastes cement. The 850×550 mm pallet size must align with the curing area layout and the forklift the buyer already operates on site. Siemens or ABB motors are specified as standard because service networks for these brands cover most export markets, reducing downtime if a motor issue arises.
The Hidden Cost of Skipping the Pre-Ship Checklist
When voltage and frequency are not confirmed before the machine leaves, the buyer discovers at commissioning that the 380V/50Hz configuration does not match their local grid. Rewiring or adding a transformer on site delays production and adds unplanned expense. The same applies to the control panel language — if the operator cannot read the electric control display, every mould change and cycle adjustment becomes a guessing game [NEED_CITE: electrical standard mismatches in international machinery trade].
Why Buyers Source This Machine Through Our Dispatch Process
Block machinery is our single focus, so the QTJ4-25 is never shipped as a standalone press — it leaves with matched moulds, pallets, and handling components specified as one system. Configuration is set against the buyer’s actual mix design and target block format, not a catalogue default. Mould supply covers the formats the buyer’s market actually sells, with custom drawings available for non-standard shapes. The automation level is semi-automatic, and buyers can plan an upgrade path as production volume grows. Packing photographs and the container loading plan are shared before shipment so the buyer knows exactly how the machine will arrive.
Documentation & Verification
- Line layout with capacity stated per specific block format before order confirmation
- Voltage and frequency confirmation sheet signed off before production begins
- Factory test record on the buyer’s requested mould format prior to dispatch
- Pallet specification matched to curing area dimensions and forklift capacity
- Mould list and wear parts list included for first replacement sourcing
Installation, Commissioning & Support
- Workshop area of 50–150 m² requires level concrete foundation before machine arrival
- 380V 3-phase dedicated circuit must be installed before commissioning begins
- Machine ships dismantled; reassembly sequence provided with packing photographs
- First run includes cycle time verification on the buyer’s chosen block format
- Operator training covers mould change procedure and electric control operation
- Wear parts list enables local sourcing of high-wear components after arrival
What We Need to Move Your Order Forward
To prepare a dispatch plan for the QTJ4-25, share your target block format, the daily volume your market absorbs, and the curing space available on your site. Confirm your local voltage, frequency, and the language your operators read on a control panel. Let us know what forklift and pallet handling equipment you already have so the pallet size we ship is compatible from day one.
Frequently Asked Questions
Q: What is the dispatch lead time for QTJ4-25 and is the machine currently in stock?
A: Stocked units can enter the container loading process once voltage, frequency, and pallet specifications are confirmed. The lead time depends on how quickly these variables are locked in. We provide a container loading plan and packing photographs before the container leaves the yard.
Q: How is the machine dismantled and loaded into a container for sea shipment?
A: The press frame, mixer, belt conveyor, and pallet stack are separated and loaded in a fixed sequence to prevent shifting during transit. Each component’s position in the container is documented with photographs shared before dispatch.
Q: What is the arrival estimate once shipped to my port?
A: We quote an arrival estimate based on the shipping line’s published schedule at the time of booking. This estimate accounts for the route and port rotation, not a best-case scenario.
Q: Which block formats and moulds are stocked versus made to order?
A: Standard hollow and solid block moulds matching common dimensions are typically available with the machine. Custom moulds for non-standard shapes or specific interlocking profiles require a design review and additional lead time before shipment.
Q: Is voltage and frequency customization confirmed before the machine leaves the factory?
A: Yes. Voltage, frequency, and control panel language must all be confirmed and documented before the QTJ4-25 enters production or leaves stock. This prevents commissioning delays caused by grid mismatch at the destination.