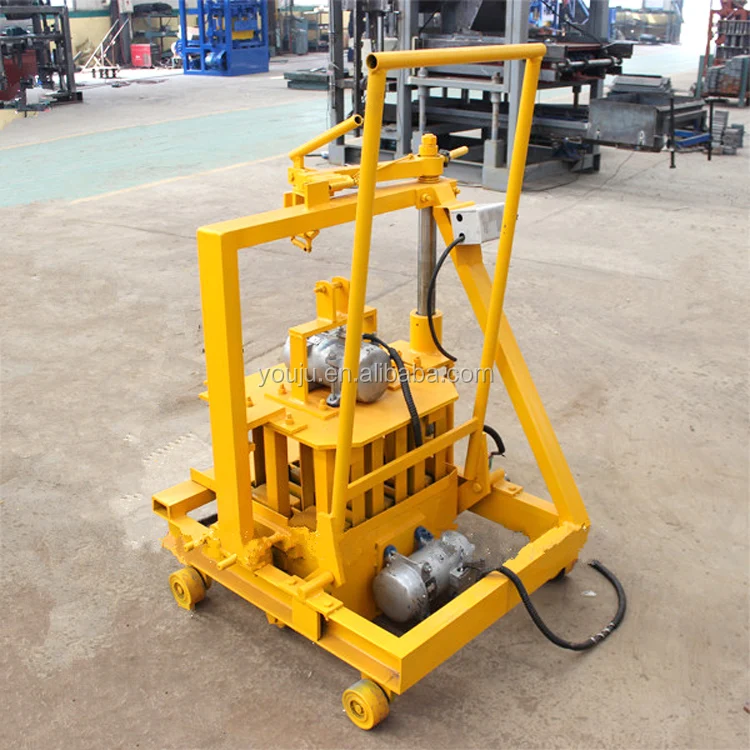
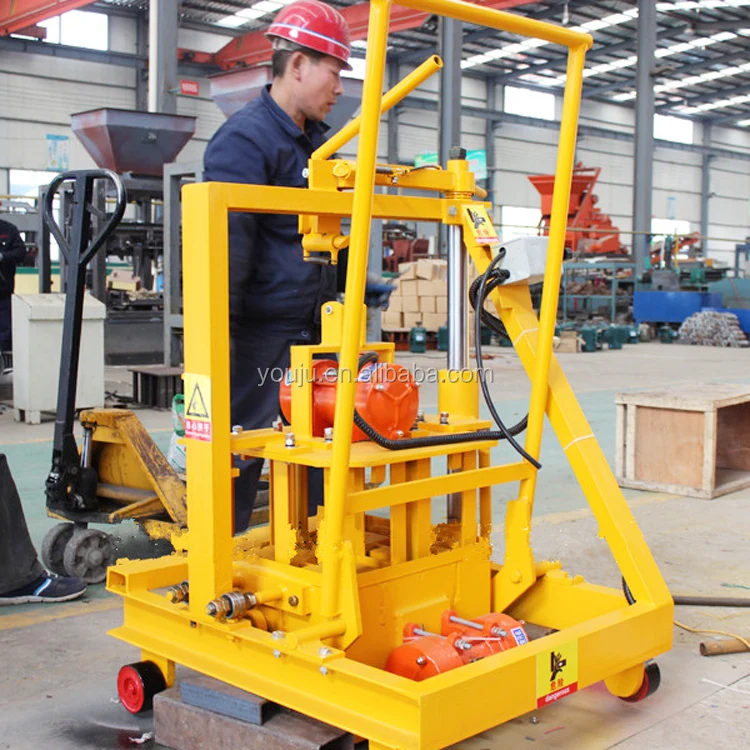
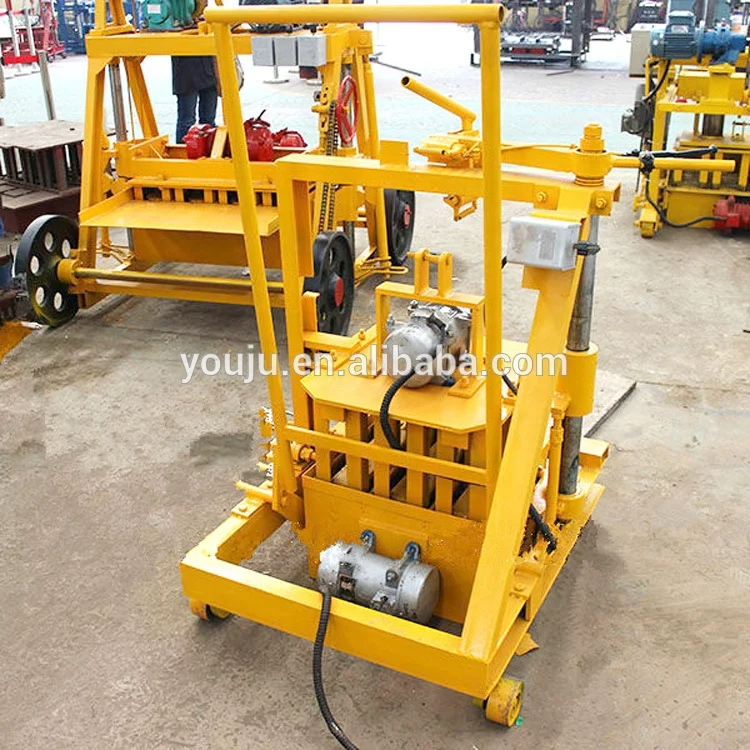
Description
Stock-to-Ship Readiness — every QMJ2-45 unit leaving our Linyi yard is factory-tested against the buyer’s raw material sample before container loading, not after arrival.
Technical Specifications
| Parameter | Value |
|---|---|
| Model | QMJ2-45 |
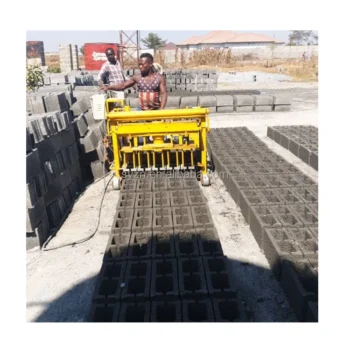
| Product Type | Mobile Block Making Machine |
| Automation Level | Manual operation, no pallets required |
| Mould Change Method | Manual mould replacement for different hollow brick formats |
| Labor Requirement | 1 to 3 workers |
| Mould Format A | Hollow brick 400×200×200 mm — 2 pcs/mould, cycle 25–30 s, 160 pcs/h, 1280 pcs/8 hr |
| Mould Format B | Hollow brick 400×150×200 mm — 3 pcs/mould, cycle 25–30 s (8 hr figure basis to be confirmed) |
| Mould Format C | Hollow brick 400×100×200 mm — 4 pcs/mould, cycle 25–30 s, 320 pcs/h, 2560 pcs/8 hr |
| Pallet System | Not required (egg-laying / mobile type) |
| Power Source | Electric (voltage & frequency configurable for destination market) |
| Control System | Manual |
| Mould Treatment | Heat treatment and carburization |
| Certification | CE, ISO 9001:2000 |
Application Suitability
| Application | Material or Output |
|---|---|
| Small-scale on-site hollow block production | Cement mixed with local sand, crushed stone, or gravel aggregate |
| Construction job-site block manufacturing | Red soil blended with aggregate, laterite, or volcanic ash where locally sourced |
| Rural and remote-area block supply | Cement-stabilized soil, fly ash blends, or crusher dust mixes |
| First-time block plant startups | Standard concrete mixes with minimal batching infrastructure |
Why "In Stock" Should Mean More Than a Warehouse Tag
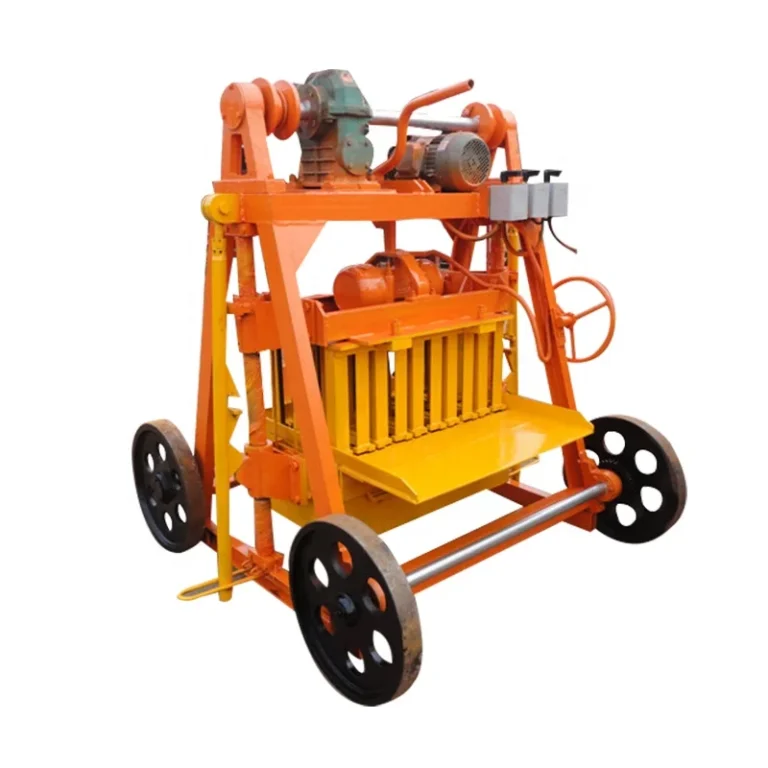
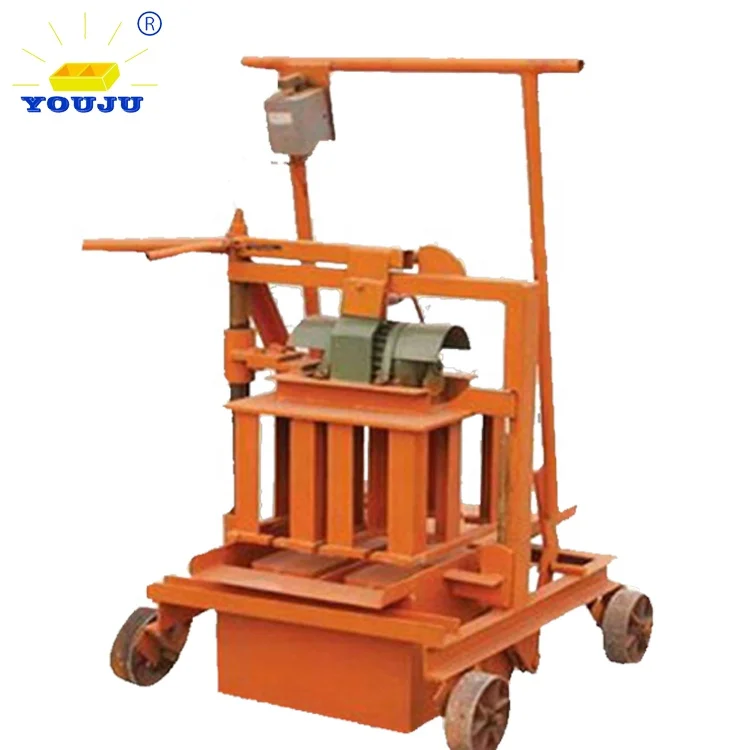
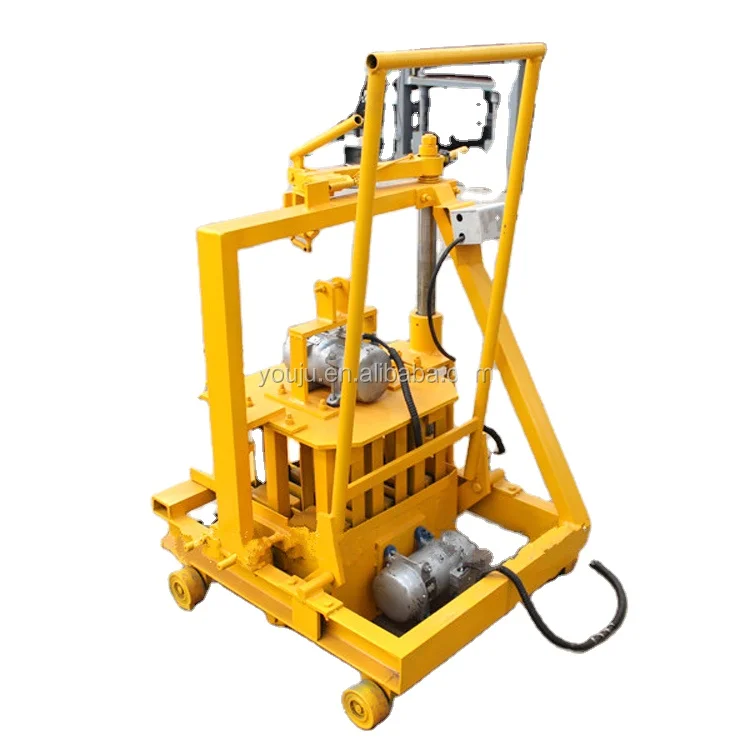
A stocked QMJ2-45 mobile block making machine in stock only matters if the unit has been run on material resembling yours before it ships.
I have watched container arrivals turn into weeks of on-site debugging because the machine was tested on clean silica sand in Shandong while the buyer in West Africa was feeding laterite mixed with crushed granite. The vibration characteristics shift entirely when aggregate angularity and moisture content change. [NEED_CITE: effect of aggregate shape on block compaction in manual egg-laying machines] A dispatch-ready unit must be validated against the actual mix, not a laboratory default. This step is where most fast-delivery promises fall apart.
What Fast Dispatch Actually Covers
Securing a QMJ2-45 mobile block making machine in stock from the Linyi production yard means the frame, vibration assembly, and mould set have already passed mechanical run-in. The machine can be dismantled into its container-loading configuration within days rather than weeks of build time. For project contractors facing a construction deadline, this difference compresses the gap between purchase order and first block on the ground to a matter of port transit time.
The Loading Sequence That Prevents Arrival Damage
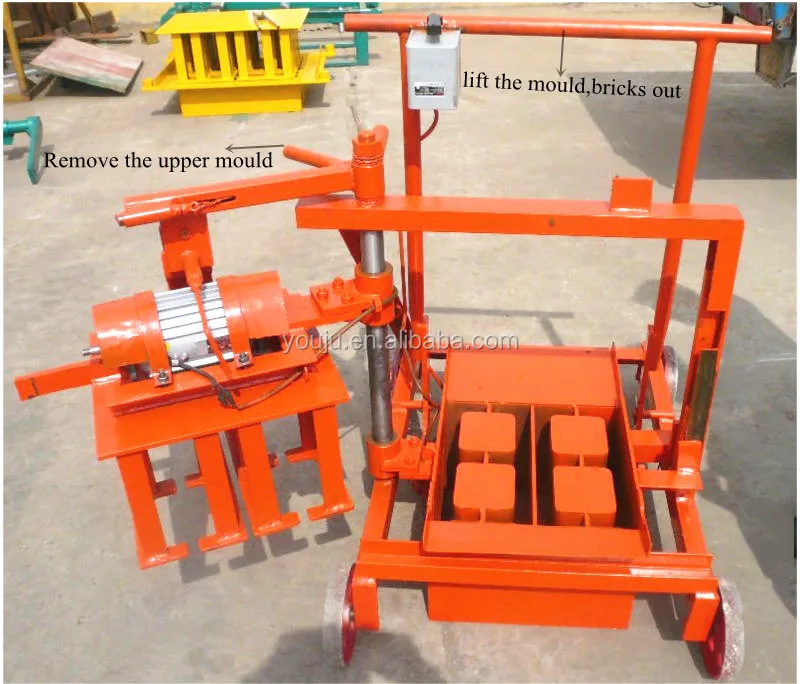
Mobile egg-laying machines are compact enough to ship in standard containers, but their vibration motors and guide columns need specific bracing. Each QMJ2-45 is partially dismantled — mould removed, guide rails secured, electrical panel wrapped and boxed separately — then positioned on dunnage with the heavy base frame bearing the load. Container loading photographs are shared with the buyer before the seal goes on. [NEED_CITE: container lashing standards for heavy machinery export]
Reading the Capacity Table Without Being Misled
The output figures for the QMJ2-45 — 160 pieces per hour for 400×200×200 mm hollow blocks and 320 pieces per hour for 400×100×200 mm blocks — assume a consistent 25–30 second cycle with immediate repositioning on level ground. In practice, the smaller the block format, the more repositioning moves are required per square meter of cured area, and ground preparation becomes a larger share of total shift time. Mould carburization and heat treatment keep the cavity walls dimensionally stable across these cycles, which matters when you are producing thousands of blocks per shift and any taper in the mould shows up as stacking misalignment downstream. The manual operation means cycle consistency depends on operator rhythm — experienced teams settle into a pace that less experienced crews take a full shift to find.
The Cost of Skipping Voltage Confirmation Before Dispatch
A QMJ2-45 mobile block making machine in stock ships quickly, but if the motor winding is configured for 380 V / 50 Hz and arrives at a site running 440 V / 60 Hz, the vibration motor overheats within the first production day. The damage is not always immediate — it shows as weakening block density over the first week before the winding finally fails. Replacement motors take longer to source locally than the original dispatch saved. [NEED_CITE: industrial motor voltage mismatch failure patterns in export markets] Voltage and frequency must be confirmed against the buyer’s grid before the unit is crated.
What Stock Availability Means from This Yard
Every QMJ2-45 held ready for dispatch has been assembled, run through a test cycle, and had its mould cavity dimensions verified against tolerance. The standard mould set — 400×200×200, 400×150×200, and 400×100×200 mm hollow formats — ships with the machine, and additional moulds can be consolidated into the same container. Because block machinery is the single focus here, the pallet-free egg-laying system is specified as a complete unit with matched vibration force and mould geometry rather than assembled from separate component suppliers. The Linyi yard maintains stock of carburized replacement moulds and vibration motor assemblies so that first spare orders can ride the same vessel or follow in a subsequent shipment without delay. [NEED_CITE: typical mould wear intervals for cement-aggregate hollow block production]
Documentation & Verification
- Factory test record on buyer-supplied aggregate blend before dispatch
- Container loading photographs with seal number logged
- Voltage and frequency confirmation sheet signed before crating
- Mould cavity dimension check report per format shipped
- Operation manual with illustrated mould-change procedure
Installation, Commissioning & Support
- Level compacted ground required — no fixed foundation or pallet storage area needed for the QMJ2-45
- Dedicated electrical circuit matching confirmed voltage and frequency must be available at site before arrival
- Machine arrives partially dismantled; guide rails and mould reattach with standard hand tools
- First production run supervised remotely or on-site to establish cycle rhythm with local mix
- Operator training covers mould change sequence, mix moisture judgement, and repositioning spacing
- Carburized mould and vibration motor kept in Linyi stock for rapid reorder
Before You Request a Dispatch Date
To confirm availability and give you a realistic arrival estimate, the key inputs are your target block format and daily requirement, your local aggregate type and cement ratio, and your site voltage and frequency. Share a photo of your raw materials and a sample of the block your market expects, and the right mould set and motor configuration can be locked in before crating.
Frequently Asked Questions
Q: Is the QMJ2-45 currently in stock and what is the dispatch lead time?
A: Units are held in the Linyi yard after factory assembly and test run. Once voltage and frequency are confirmed for your market and mould formats are agreed, the machine can be dismantled and container-loaded within a short window. Exact dispatch days depend on container booking availability at the port.
Q: How is the machine packed and loaded into a container for shipment?
A: The QMJ2-45 is partially dismantled — mould removed, guide rails secured, electrical panel boxed separately — and positioned on dunnage inside the container with the base frame bearing the load. Loading photographs and the container seal number are shared with the buyer before dispatch.
Q: What is the estimated arrival time to my destination port?
A: Port-to-port transit time depends entirely on the destination and current shipping line schedules. Once the container is booked, the estimated arrival date is provided upfront so project planning can proceed without guesswork.
Q: Which mould formats ship as standard and can additional moulds be added?
A: The standard set includes hollow brick moulds at 400×200×200, 400×150×200, and 400×100×200 mm. Additional formats or spare moulds can be consolidated into the same container at dispatch, avoiding separate freight costs.
Q: What voltage and frequency options are available from stock?
A: Motor windings can be configured for the buyer’s local grid before crating. Voltage and frequency must be confirmed at order stage so the correct winding is installed and tested during the pre-dispatch factory run.