


Description
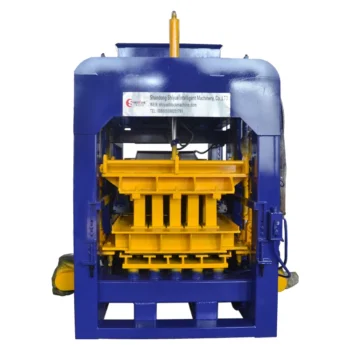
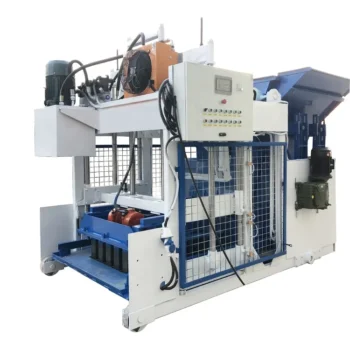
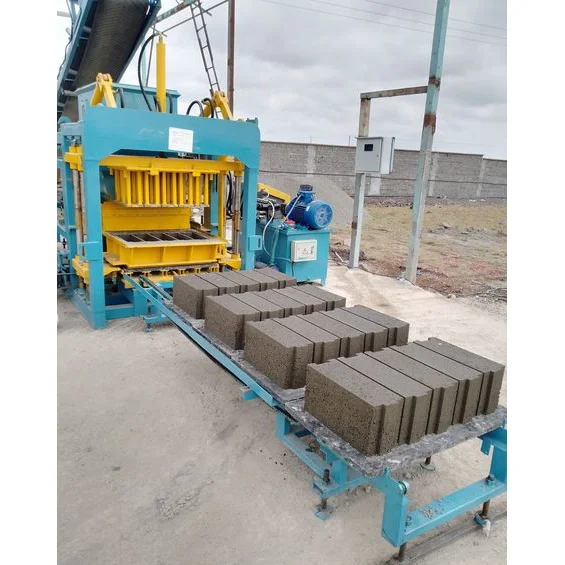
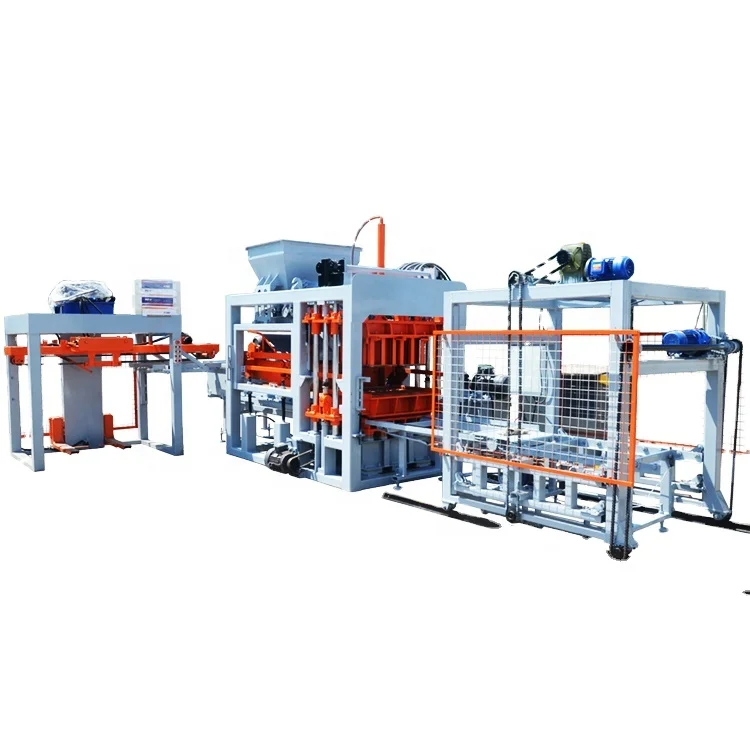
Stocked Readiness — The QT18-15 is assembled, tested, and staged for immediate container loading rather than waiting on a production queue.
Technical Specifications
| Parameter | Value |
|---|---|
| Model | QT18-15 |
| Product Type | Fully Automatic Block Production Line |
| Machine Type | Hollow Block, Paving Block, and Curbstone Block Making Machine |
| Raw Material | Concrete |
| Processing Method | Hydraulic pressure |
| Control System | PLC control |
| Voltage | Local Voltage (source value — verify against manufacturer catalog) |
| Overall Dimensions (L×W×H) | 935025202950mm |
| Net Weight | 150000 kg |
| Pallet Size | 1350x1350x30mm |
| Molding Cycle | 15s (basis not stated in source — confirm block format / material / thickness) |
| Forming Cycle | 15~20 Sec (basis not stated in source — confirm block format / material / thickness) |
| Hydraulic Pressure | 15-30MPA |
| Vibrating Force | 260-420KN |
| Brick Size Options | 400100200mm, 400120200mm, 20010060mm, 400150200mm, 24011590mm, 20020060mm, 400200200mm, 230220115mm |
| Core Components | PLC, Pressure Vessel, Engine, Gear, Motor, Pump, Bearing, Gearbox |
| Warranty | 1 Year |
| Color | Client requirement |
Application Suitability
| Application | Material or Output |
|---|---|
| Housing and development contractors | On-site concrete hollow block production for phase-completion deadlines |
| Building material distributors | High-volume paving and curbstone manufacturing for rapid inventory replenishment |
| Concrete product manufacturers | Standardized concrete block formats using locally sourced aggregates |
Why "Fast Delivery" Often Fails at the Container Door
When a project deadline is looming, waiting months for manufacturing is not an option, but securing a QT18-15 block machine in stock is only the first step. True speed relies on matching the physical footprint of the machinery to standard shipping dimensions before the order is finalized.
I have seen contractors rush a heavy press out the factory door, only to realize the 150000 kg mainframe and 1350x1350x30mm pallets were not properly dismantled for standard container loading. The machine sits at the port while the site deadline passes. Dispatch lead times mean nothing if the loading plan causes clearance delays [NEED_CITE: standard container loading limits for heavy industrial machinery]. A fast delivery concrete block production line must be stripped, braced, and photographed for customs before it ever leaves the facility.
Dispatch Timelines and Container Loading
Securing a QT18-15 block machine in stock eliminates the manufacturing queue, shifting the focus entirely to logistics. The 935025202950mm mainframe requires precise dismantling to fit into standard shipping containers without compromising the hydraulic pressure vessels or the gearbox. Every component is braced and secured to prevent transit damage, ensuring the equipment arrives exactly as it left the floor.
Pallet Configuration and Shipping Efficiency
The standard 1350x1350x30mm pallet configuration is selected not just for the press, but for transport efficiency. These pallets are stacked and bundled to maximize container space alongside the core components. By confirming pallet availability from current stock, we prevent the common delay where the mainframe ships but the curing racks and handling boards are left behind waiting for a separate production run [NEED_CITE: impact of missing auxiliary equipment on project commissioning].
Understanding the Physical Footprint
The 260-420KN vibrating force and 15-30MPA hydraulic pressure require a heavy, rigid frame, resulting in a 150000 kg net weight. This mass dictates the crane requirements at the destination port and the foundation prep on-site. The PLC control system and motor are disconnected and packed in weather-sealed crates to protect the sensitive electronics from ocean humidity. Knowing these physical realities upfront prevents expensive surprises when the container doors finally open.
The Hidden Cost of Uncoordinated Dispatch
Rushing a machine to the port without verifying the destination voltage or the control language turns a fast delivery into a prolonged site delay. If the PLC is not pre-configured for the local grid before dismantling, the contractor pays for idle installation crews while waiting for replacement components. I have watched projects stall for weeks simply because the dispatch team ignored the electrical schematic [NEED_CITE: common electrical mismatches in exported heavy machinery].
Why Source This Equipment Here
Our focus is strictly on block machinery, meaning the mainframe, moulds, and pallets are staged together as one matched system. We provide upfront arrival estimates based on actual container loading plans, not generic catalogue promises. Standard moulds for the 8 common brick sizes are verified in stock alongside the press. Every shipment includes packing photographs and complete customs documentation to ensure smooth port clearance.
Documentation & Verification
- Factory test record verifying hydraulic pressure and vibrating force before dismantling.
- Detailed container loading plan showing bracing for the 150000 kg mainframe.
- Packing photographs documenting the condition of the PLC and motor crates.
- Machinery test report and video outgoing-inspection for customs clearance.
- CE declaration where applicable for destination market compliance.
Installation, Commissioning & Support
- Foundation requirements mapped to the 935025202950mm footprint and dynamic vibrating force.
- Dedicated power circuit planning based on the confirmed local voltage and motor specifications.
- Reassembly of the dismantled hydraulic pressure vessels and core gearbox components on-site.
- Initial PLC control system boot-up and language verification upon power connection.
- Operator training focused on rapid mould change procedures for the 8 standard brick sizes.
- Immediate handover of the wear parts list for the hydraulic pump and bearings.
Preparing Your Site for Arrival
To ensure the equipment integrates smoothly upon arrival, provide your destination port details and local voltage frequency so the electrical crates are labeled correctly. Confirm the crane lifting capacity available at your site to handle the 150000 kg mainframe during unloading. Finally, verify your raw material staging area can support the continuous feed requirements of the press once reassembled.
Frequently Asked Questions
Q: What is the exact dispatch lead time for the stocked QT18-15?
A: Because the mainframe and standard moulds are already assembled, the lead time is strictly limited to the dismantling, bracing, and container loading process. We provide a confirmed dispatch date and an upfront arrival estimate based on your specific destination port before the order is finalized, ensuring your project timeline remains intact.
Q: How is the heavy machinery dismantled for fast shipment?
A: The 150000 kg mainframe is carefully stripped of its PLC control panels, hydraulic hoses, and motor assemblies. These sensitive components are packed in weather-sealed wooden crates, while the heavy structural frame is braced and secured directly to the container floor to prevent transit shifting and ensure rapid reassembly on-site.
Q: Which standard pallets and moulds are currently in stock?
A: We hold the standard 1350x1350x30mm pallets and the standard moulds for the 8 common brick sizes, including the 400200200mm hollow block format. Confirming these auxiliary items from current stock ensures they are loaded into the same containers as the main press, preventing delayed commissioning.
Q: What customs documentation is provided to prevent delays?
A: Every shipment includes a comprehensive documentation package featuring the machinery test report, video outgoing-inspection records, detailed packing lists, and packing photographs. Where applicable, we also include the CE declaration, giving your customs broker everything required to clear the heavy equipment through the port without administrative holds.
Q: Is the PLC voltage pre-configured before dispatch?
A: Yes, we confirm your destination country’s voltage and frequency requirements before the machine is dismantled. The PLC control system and motor configurations are verified against these specifications, and the control language is set accordingly, ensuring the electrical crates are ready for immediate connection upon arrival.