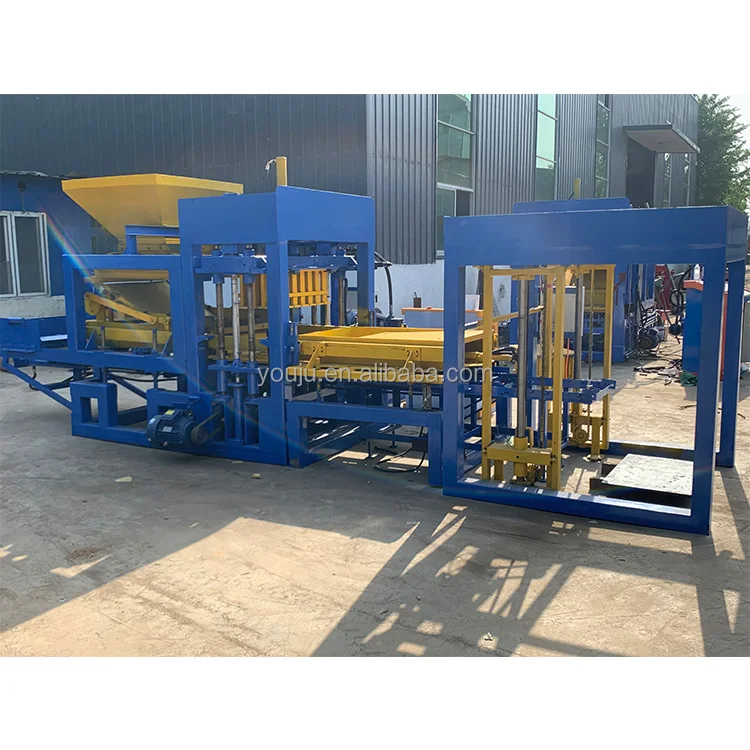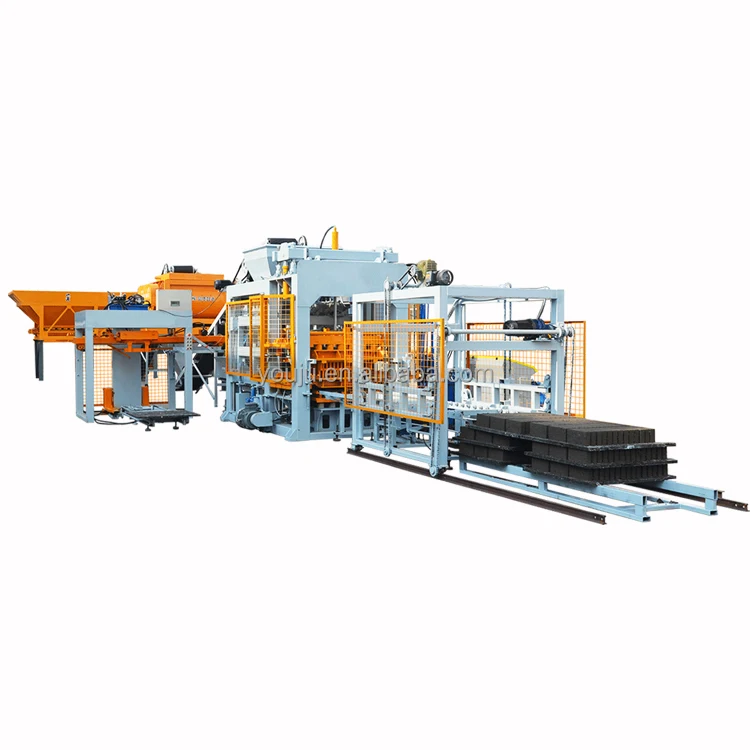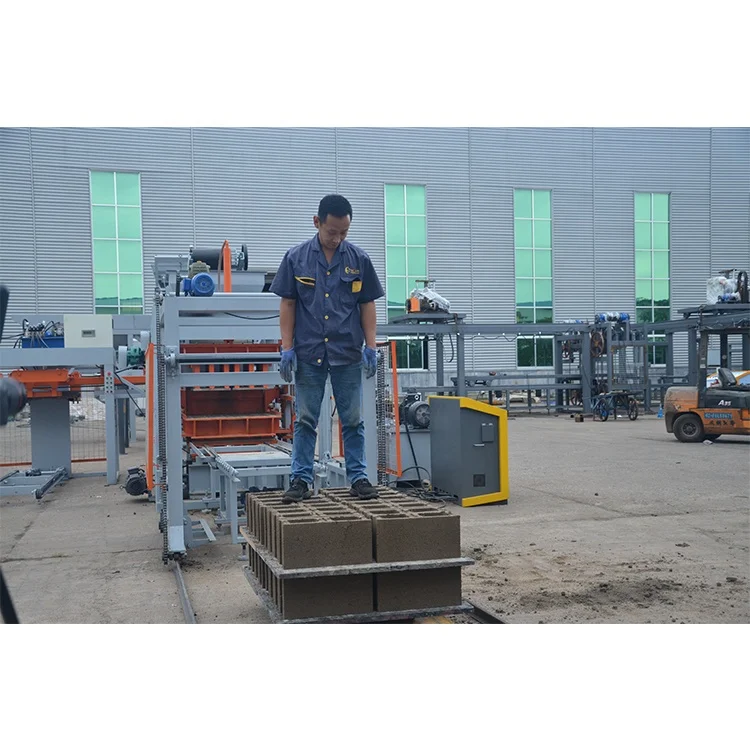
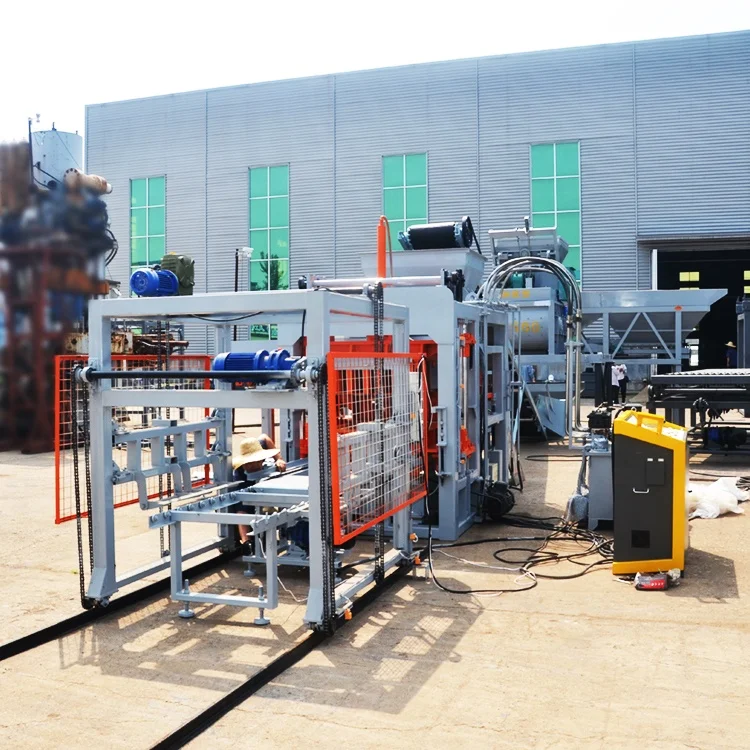
Description
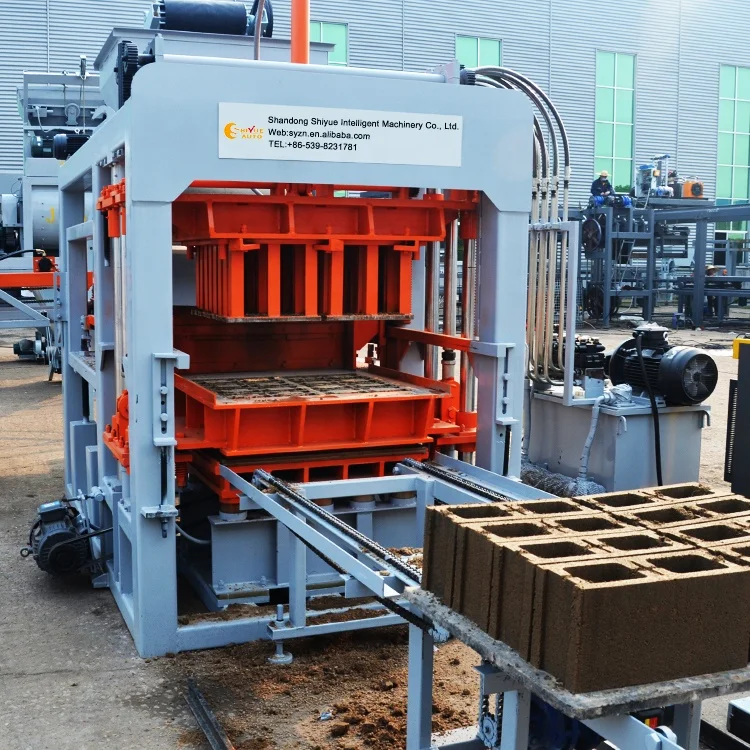
Dispatch-Ready Configuration — every QT6-15 block machine in stock is matched to your local voltage, PLC language, and pallet size before the container doors close, so commissioning starts the day power is connected.
Technical Specifications
| Parameter | Value |
|---|---|
| Model | QT6-15 |
| Product Type | Hydraulic Block Making Machine |
| Overall Dimensions (L×W×H) | 8200×1700×2950 mm |
| Total Mass | 7 T |
| Overall Power | 37 kW |
| Vibration Frequency | 0-60 Hz |
| Vibration Force | 45 kN |
| Vibration Form | Platform Vibration |
| Moulding Mode | Automatic loading, vibration moulding |
| Demolding Method | Hydraulic |
| Pallet Size | 880×850 mm |
| Molding Cycle | 15-20 s (basis not stated in source — confirm block format / material / thickness) |
| Control System | PLC with touch screen interface and fault diagnosis |
| Output — Hollow Block 400×200×200 mm | 1080-1440 pcs/h, 8640-11520 pcs/8hr |
| Output — Hollow Block 400×150×200 mm | 1440-1920 pcs/h, 11520-15360 pcs/8hr |
| Output — Solid Brick 240×115×53 mm | 5760-7680 pcs/h, 46080-61440 pcs/8hr |
| Output — Rectangular Brick 200×100×60 mm | 2160-2880 pcs/h (cycle 20-25 s), 17280-23040 pcs/8hr |
| Output — Zigzag Brick 225×112.5×60 mm | 2160-2880 pcs/h (cycle 20-25 s), 17280-23040 pcs/8hr |
| Block Compressive Strength | More than 15 MPa |
| Recommended Factory Area | 1200 m² |
| Hydraulic System | Independent integrated station, isolated from dust and main machine vibration |
| Raw Material Adaptability | Waste ash, slag, and various aggregates; reduces cement dosage |
| Warranty | 1 year for whole machine (excluding spare parts) |
Application Suitability
| Application | Material or Output |
|---|---|
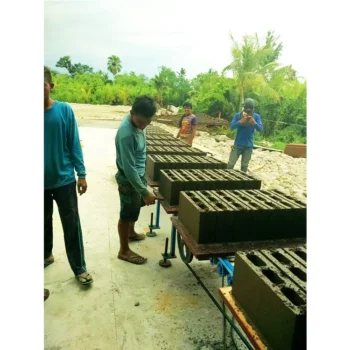
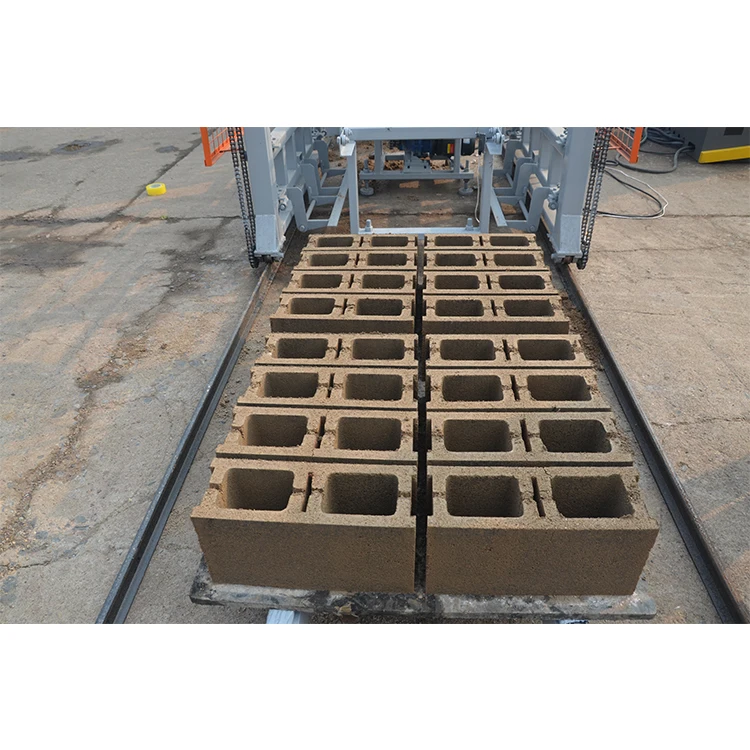
| Housing project hollow block production | Crushed stone, river sand, and cement producing 400×200×200 mm or 400×150×200 mm hollow blocks |
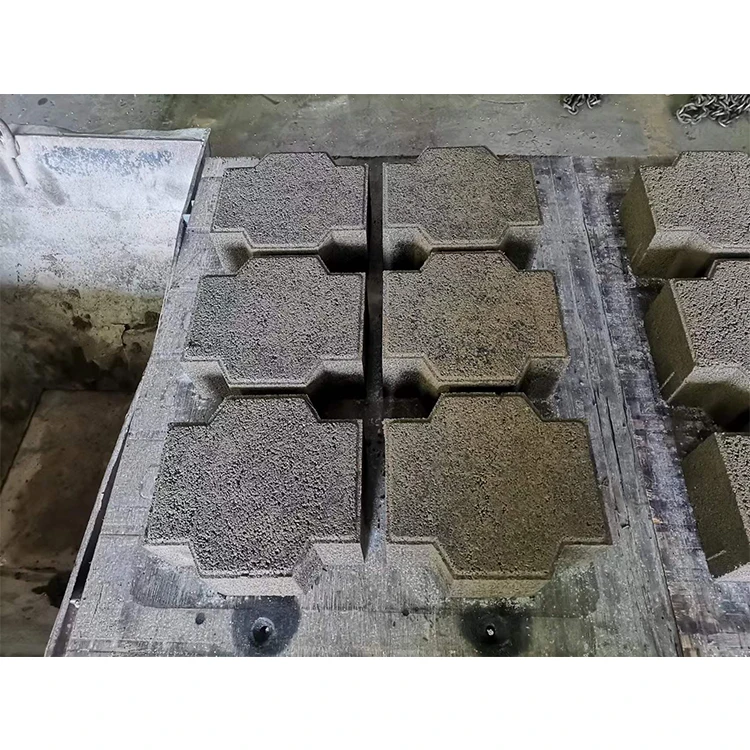
| Paving brick for commercial and municipal areas | Fine aggregate and cement producing 200×100×60 mm rectangular or 225×112.5×60 mm zigzag pavers |
| Solid brick for load-bearing walls | Standard sand-cement mix producing 240×115×53 mm solid bricks |
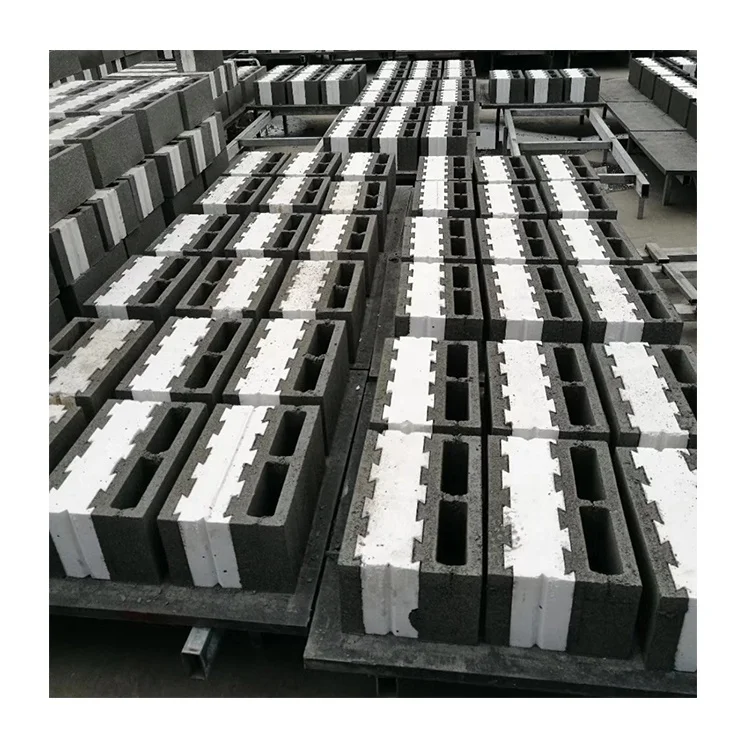
| Lightweight block from industrial by-products | Waste ash or slag blended with cement for multicellular or hollow lightweight formats |
| On-site block production for remote construction projects | Local aggregate sourced near the job site, reducing transport cost for hollow blocks |
Why "Output per Hour" Alone Can Derail Your Project Timeline
Real daily throughput depends on the block format you actually sell, not the fastest cycle the press can achieve.
When a buyer receives a quotation stating only the peak hourly figure — often based on the smallest solid brick — the real production rate for the hollow blocks that dominate most markets can fall well below expectations. On a housing development with a fixed handover date, that gap between quoted and actual output translates directly into missed milestones, penalty clauses, and rushed overtime shifts. The QT6-15 block machine in stock is listed here with cycle times broken down per format so you can plan your pour schedule against real numbers, not catalogue maximums [NEED_CITE: block production planning based on format-specific cycle times].
Container Loading and Dispatch Readiness
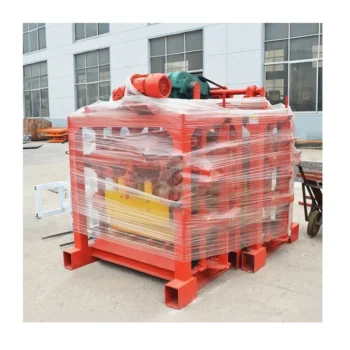
The QT6-15 block machine in stock ships dismantled into press frame, hydraulic station, and mould assembly for standard 40-foot container loading. Each component is secured with timber bracing and steel strapping so transit damage to the hydraulic lines and PLC panel is eliminated. Stocked models and standard mould formats can be dispatched within a typical multi-week lead time, and the loading plan is shared with the buyer before the container is sealed. This matters when your project deadline is measured in weeks, not months, and any delay at the factory gate ripples through ocean freight booking and port-side customs clearance.
Arrival Estimates and What Ships with the Machine
Before the container leaves, you receive packing photographs showing every major component, the mould crate, and the spare parts box. The dispatch documentation confirms exactly which moulds, hydraulic seals, and pallet-handling accessories are inside so there are no surprises at the destination port. For buyers importing the QT6-15 block machine in stock to replenish inventory or meet a seasonal demand window, knowing the full manifest before sailing eliminates the scramble to air-freight missing parts across continents [NEED_CITE: container loading practices for heavy industrial machinery].
Spec Details That Shape Your Daily Production Reality
The 45 kN vibration force paired with the independent hydraulic station determines how densely the concrete is compacted inside the mould cavity. Higher compaction pressure against the right mix design yields blocks that meet the 15 MPa compressive strength threshold consistently — essential for structural hollow blocks that must pass site inspection. The 880×850 mm pallet size must align with the curing racks and forklift fork dimensions already on your floor; a mismatch here means purchasing new handling equipment or rearranging the curing yard after the machine arrives. The PLC touch screen includes fault diagnosis, which shortens troubleshooting time when an operator is unfamiliar with hydraulic press sequences, though the display language must be confirmed before the unit leaves the factory. Platform vibration distributes force evenly across the pallet area, reducing density variation between blocks at the centre and edges of each cycle.
What Happens When Voltage and Language Are Left to Chance
A machine wired for a frequency that does not match the local grid will run motors at incorrect speeds, altering vibration frequency and cycle timing from the first day. Similarly, a PLC interface in a language the operators cannot read turns fault diagnosis from a quick screen check into a call to an overseas technician, leaving the line idle for hours. Buyers who confirm voltage, frequency, and control language during the order stage avoid these commissioning stalls entirely. When these details are left vague in the purchase order, the QT6-15 block machine in stock may arrive physically ready but electrically incompatible, pushing back first production by weeks [NEED_CITE: voltage and frequency standards by export market].
Why Buyers Source This Machine Here
The machine, mould, pallet, and handling equipment are specified as one matched system rather than assembled from unrelated suppliers, so pallet size and curing rack dimensions are coordinated before the container is loaded. Configuration is set against your actual mix design and local aggregate, not pulled from a generic catalogue default. Mould design covers the formats your market actually sells, including custom drawings if your region demands a non-standard block profile. Automation level is selectable — a buyer can begin with semi-automatic pallet handling and upgrade the stacking system later without replacing the press. Installation support includes operator training on the specific PLC interface and hydraulic sequences of this machine, and the wear parts list ensures the first replacement set is on hand when needed.
Documentation & Verification
- Line layout showing QT6-15 placement within your 1200 m² factory area
- Capacity calculation stating the specific block format assumed for each output figure
- Factory test record run on your target mould format before dispatch
- Voltage, frequency, and PLC language confirmation sheet signed before production
- Packing photographs and container loading plan shared before shipment
- Wear parts and mould list confirming what ships inside the container
Installation, Commissioning & Support
- Foundation pad sized for the 8200×1700 mm footprint and 7 T operating weight
- Dedicated 37 kW power circuit with confirmed voltage and frequency before connection
- Dismantled press frame, hydraulic station, and mould assembly reassembled on-site
- PLC touch screen calibrated and fault diagnosis system tested during commissioning
- Operator training covering mould change procedure and hydraulic pressure adjustment
- First-set hydraulic seals and mould wear parts included for initial production runs
Before You Send an Inquiry
Share the block formats you sell most and your target daily output so the correct moulds are allocated from stock. Confirm your local voltage, frequency, and preferred PLC display language to prevent commissioning delays after arrival. Provide details on existing curing racks, forklifts, and pallet dimensions so the 880×850 mm pallet specification is validated against your site conditions.
Frequently Asked Questions
Q: What is the current dispatch lead time for the QT6-15, and is the machine in stock or built to order?
A: Stocked models and standard mould configurations can ship within typical multi-week lead times. Built-to-order configurations requiring custom moulds or non-standard voltage may require additional production time. Confirm your required format and electrical specifications early to lock in the earliest available dispatch window for your project timeline.
Q: Which mould formats are stocked and ship with the machine, and what is the container loading plan?
A: Standard stocked moulds include 400×200×200 mm and 400×150×200 mm hollow blocks, 240×115×53 mm solid bricks, and common paver formats. The machine is dismantled into press frame, hydraulic station, and mould assembly for 40-foot container loading. A detailed loading plan is shared before the container is sealed.
Q: Can voltage, frequency, and PLC language be confirmed before shipment to avoid commissioning delays?
A: Yes. Voltage, frequency, and PLC display language are confirmed in writing during the order stage and verified again before dispatch. This prevents the situation where a machine arrives electrically incompatible with the local grid or with an interface the operators cannot navigate during initial production.
Q: What spare moulds and hydraulic wear parts are included, and what is the recommended first-order spare parts list?
A: The machine ships with the selected production mould and a set of hydraulic seals sized for the integrated station. A recommended first-order spare parts list is provided with the quotation, covering the hydraulic wear items and mould components most likely to need replacement during the first production cycle.
Q: How is the machine dismantled for container shipment, and what on-site reassembly support is provided?
A: The QT6-15 is dismantled into its main structural and hydraulic assemblies for container loading, with each component braced and strapped. On-site reassembly support covers press frame alignment, hydraulic line connection, PLC calibration, and initial test runs on your chosen mould format with operator training included.