
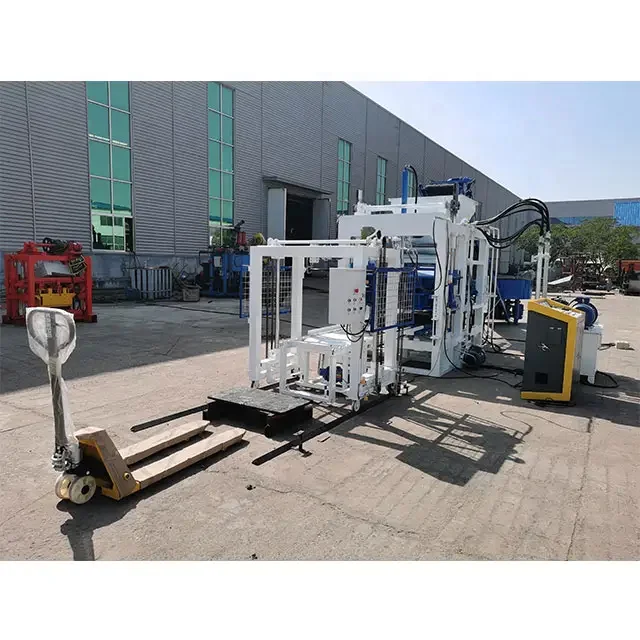
Description
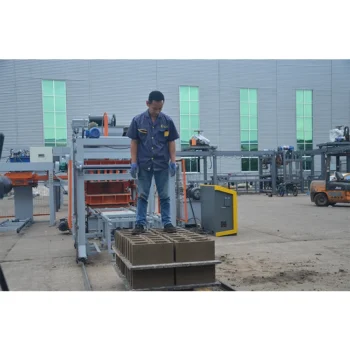
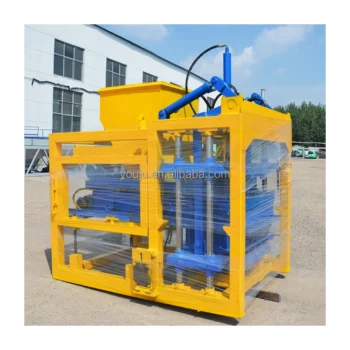
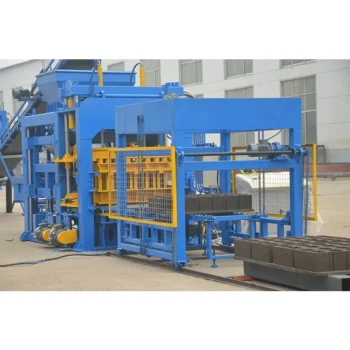
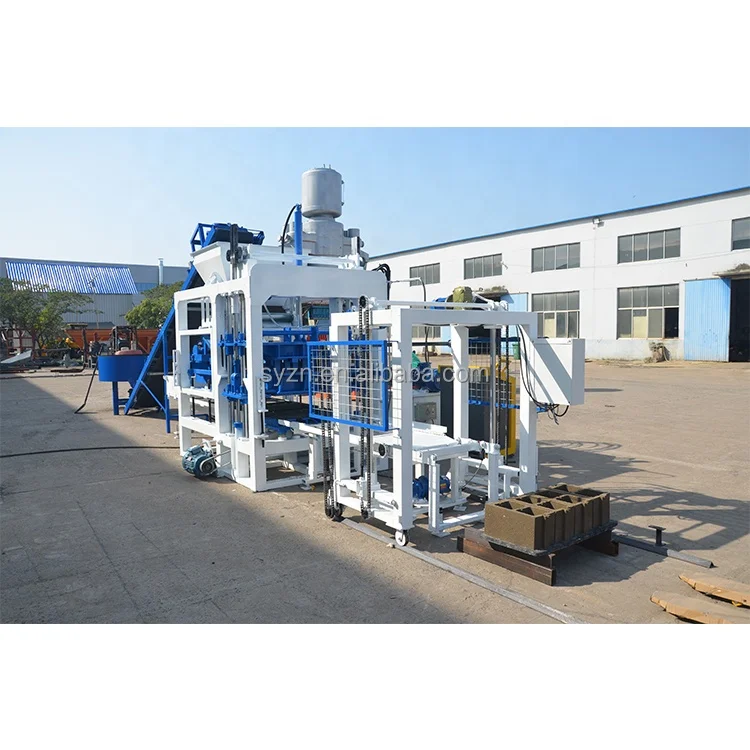
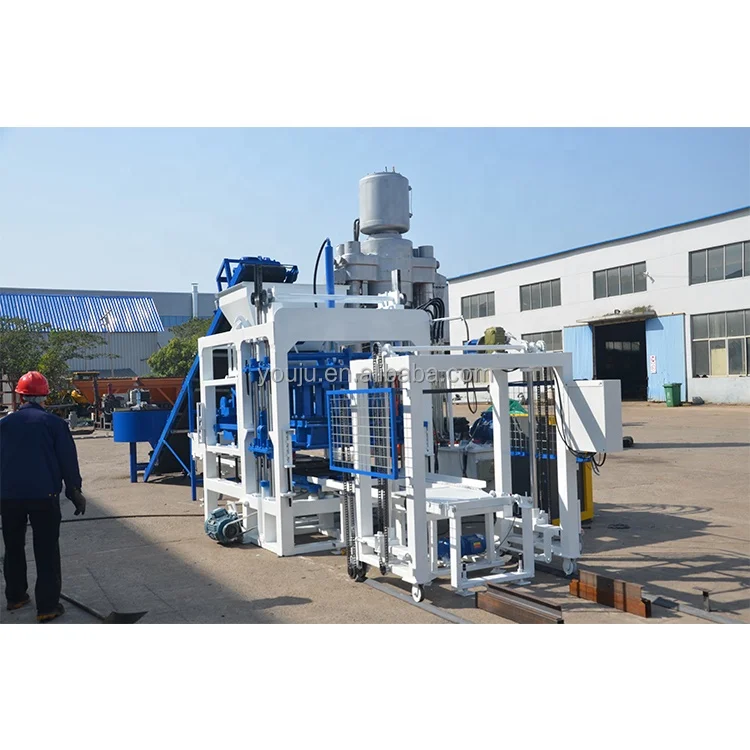
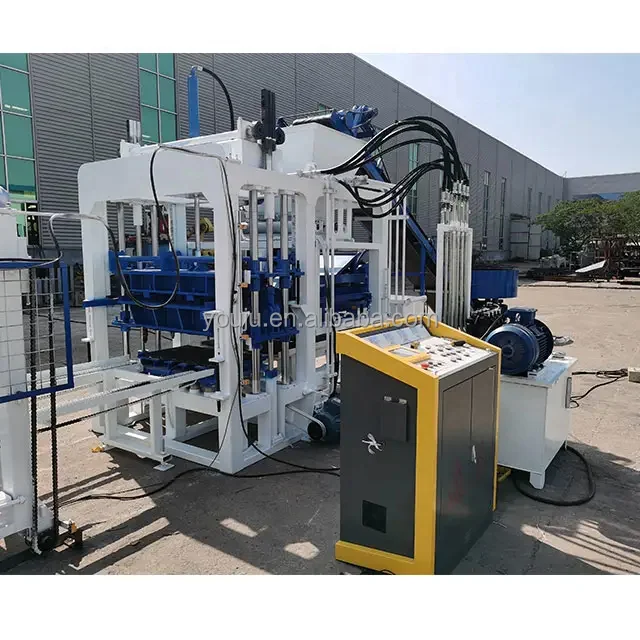
Stocked Configuration Match — We quote the QT4-18 block machine as one integrated line with pallet, handling and mould verified against your local grid before it leaves the factory floor.
Technical Specifications
| Parameter | Value |
|---|---|
| Model | QT4-18 |
| Product Type | Automatic Concrete Block Making Machine |
| Overall Dimensions (L×W×H) | 2500×1750×2200mm |
| Rated Pressure | 16 MPa |
| Vibration Form | Platform Vibration |
| Pallet Size | 950×550mm |
| Molding Cycle | 18–25s (basis not stated in source) |
| Overall Power | 27.5 kW |
| Control System | PLC with frequency converter |
| Electrical Components | Schneider |
| Mold Lifting Mechanism | Double-sided synchronous gears |
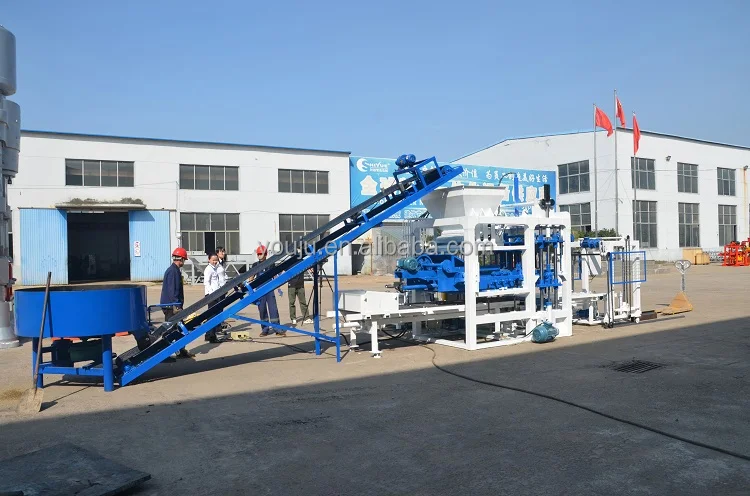
| Material Feeding System | Hopper, feeding box, feeding platform, conveyor system |
| Block Receiver | Chassis, transport system, idlers, motor, reducer, triangular belt |
| Pallet Loader Power Source | Hydro-cylinder |
| Voltage & Frequency | Configurable to destination market (confirm before shipment) |
Application Suitability
| Application | Material or Output |
|---|---|
| Construction Site Block Production | Hollow and solid blocks from local crushed stone, sand and cement |
| Small to Medium Block Plant Startup | Standard concrete masonry units for regional building supply |
| On-site Contractor Production | Pavers and interlocking bricks using site-available aggregate |
| First Plant Entrepreneurs | Format flexibility through mold changes for diverse market demand |
Why Voltage Confirmation Must Precede the Container Booking
A stocked machine sitting on a 220V/60Hz site with a 380V/50Hz motor is just painted steel until the transformer arrives.
I watched a contractor in Manila lose three weeks of curing time because the block machine quotation never asked about the local industrial supply. The QT4-18 block machine in stock fast delivery promise means nothing when the control panel refuses to initialize on arrival. Voltage mismatch is not a commissioning delay — it is a project penalty waiting to happen [NEED_CITE: industrial voltage standards across Southeast Asian and African markets].
Container Loading Starts Before the Machine Is Built
The QT4-18 block machine in stock fast delivery advantage only holds when the dispatch plan accounts for dismantling sequence. We strip the hydraulic station, remove the feeding conveyor and stack moulds vertically against the main frame before container loading begins. Every QT4-18 unit ships with photographs documenting the packing state so customs clearance at destination does not stall on missing paperwork.
Pallet Size Is a Site Decision, Not a Catalog Default
The 950×550mm pallet dimension on the QT4-18 must align with the curing racks and forklift capacity already present at the buyer’s yard. We confirm pallet material — bamboo, PVC or steel — against local humidity and curing method before the machine enters the assembly stage [NEED_CITE: curing rack load limits versus pallet material selection]. A pallet mismatch discovered after arrival means manual re-stacking from day one.
Pressure and Vibration Define What the Block Survives
The 16 MPa rated pressure combined with platform vibration determines block density, but only when matched to the buyer’s specific aggregate gradation and cement ratio. Double-sided synchronous gears keep the mould lifting balanced, preventing uneven compaction that shows up as corner crumbling during transport. The hydro-cylinder pallet loader maintains consistent feed timing so each cycle produces uniform output regardless of operator experience. The 27.5 kW overall power draw requires dedicated circuit allocation at the plant site. Schneider electrical components are specified for international serviceability, but the PLC display language must be locked in before the control cabinet is sealed [NEED_CITE: PLC interface language requirements for operator safety compliance].
What Unpriced Supporting Equipment Costs on Day One
Buyers who accept a quotation covering only the press discover on arrival that output piles on the ground because no stacker was included. The QT4-18 supporting equipment options exist for a reason — the JQ500 mixer, belt conveyor and block gripper are not accessories but operational necessities. A machine without its material feeding and output handling chain forces manual labor into every cycle, erasing the automation advantage the PLC control was designed to provide [NEED_CITE: labor allocation in semi-automated versus manual block plants].
Why Buyers Source This Machine Here
The QT4-18 ships as a matched system where press, mould, pallet and handling equipment are specified together rather than assembled from disconnected suppliers. Every configuration references the buyer’s actual mix design and target block format, not a generic catalog default. Mould supply covers the formats the buyer’s market moves, including custom drawings when standard options do not fit. Automation level remains selectable, allowing a buyer to start with manual pallet handling and add stacker integration later. Installation includes commissioning support with operator training focused on cycle optimization and mould change procedure.
Documentation & Verification
- Factory test record captured on your specified block format and mix ratio
- Voltage and frequency confirmation sheet signed before control cabinet assembly
- Machine specification with pallet size, power draw and hydraulic pressure values
- Mould drawing and format list showing changeover procedure
- Packing photographs documenting dismantling state before container sealing
- Customs documentation package matching destination country import requirements
Installation, Commissioning & Support
- Foundation pad leveled to QT4-18 footprint of 2500×1750mm with anchor bolt placement
- Dedicated 27.5 kW circuit with voltage matching confirmed at main distribution panel
- Hydraulic station reconnected and pressure verified to 16 MPa operating specification
- PLC frequency converter parameters set to molding cycle between 18–25 seconds
- Schneider component inventory reviewed with local electrical supplier for serviceability
- Mould change procedure demonstrated using double-sided synchronous gear system
- Pallet loader hydro-cylinder operation verified with selected pallet material type
What We Need to Quote Your Dispatch Window
Send us your target block format with dimensions, daily output requirement and local aggregate source so we calculate realistic cycle timing. Confirm the industrial voltage and frequency at your site, along with the PLC display language your operators need. Provide your curing area dimensions and existing forklift capacity so we match pallet specification before production begins.
Frequently Asked Questions
Q: What is the dispatch lead time for the QT4-18 in standard configuration?
A: Stocked QT4-18 units in standard configuration ship within a typical multi-week window from order confirmation. Lead time depends on mould customization requirements and supporting equipment inclusion. Container loading plan and dispatch date are confirmed in writing before production begins so project scheduling remains accurate.
Q: Is the quoted price inclusive of pallets, conveyor, and stacking equipment?
A: Each quotation specifies exactly which supporting equipment is included — pallets, belt conveyor, mixer and stacker are configured as options. The QT4-18 quotation lists every item by part number so buyers know whether output handling is covered or remains manual on arrival.
Q: What voltage and frequency options are available, and how is this confirmed before shipment?
A: The QT4-18 motor and control system are configurable to destination market voltage and frequency. We require written confirmation of your industrial supply specification before the electrical cabinet is assembled. A verification photograph of the motor nameplate is provided before container loading.
Q: How is the machine dismantled and loaded for container shipment?
A: The QT4-18 is partially dismantled with hydraulic station, feeding conveyor and moulds separated from the main frame for container loading. Packing photographs document the dismantling state and component placement so reassembly at destination follows a verified sequence.
Q: Are standard hollow block molds included, and how fast can extra molds be supplied?
A: Standard hollow block moulds are included in the base QT4-18 configuration. Additional moulds for paving blocks, interlocking bricks or custom formats are manufactured to buyer drawings. Mould supply lead time is quoted separately and depends on drawing complexity and current production schedule.